
CF8M Stainless Steel Neck Flange with Internal Support
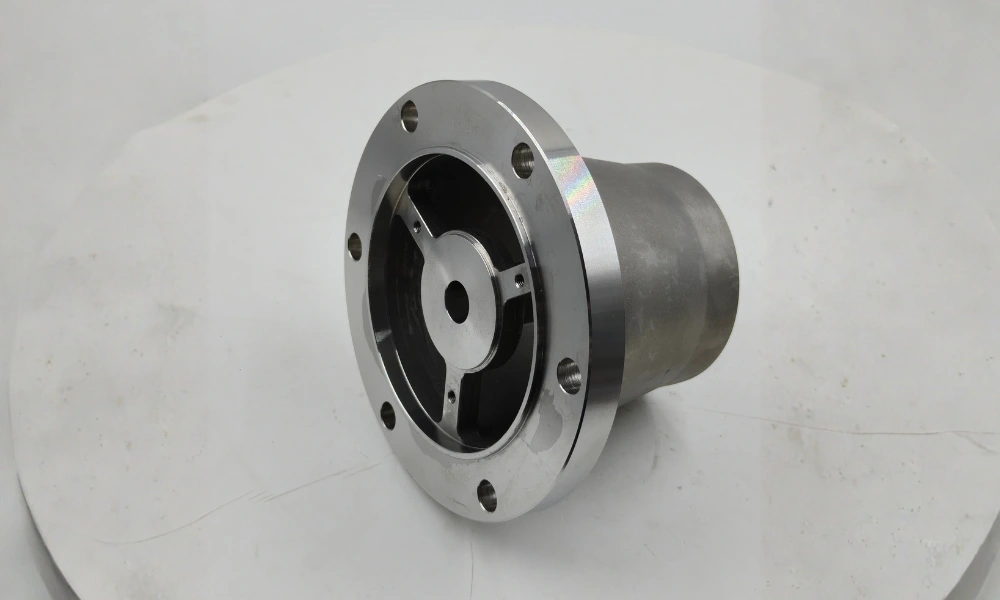
Complexity Inside the Component
Product Views
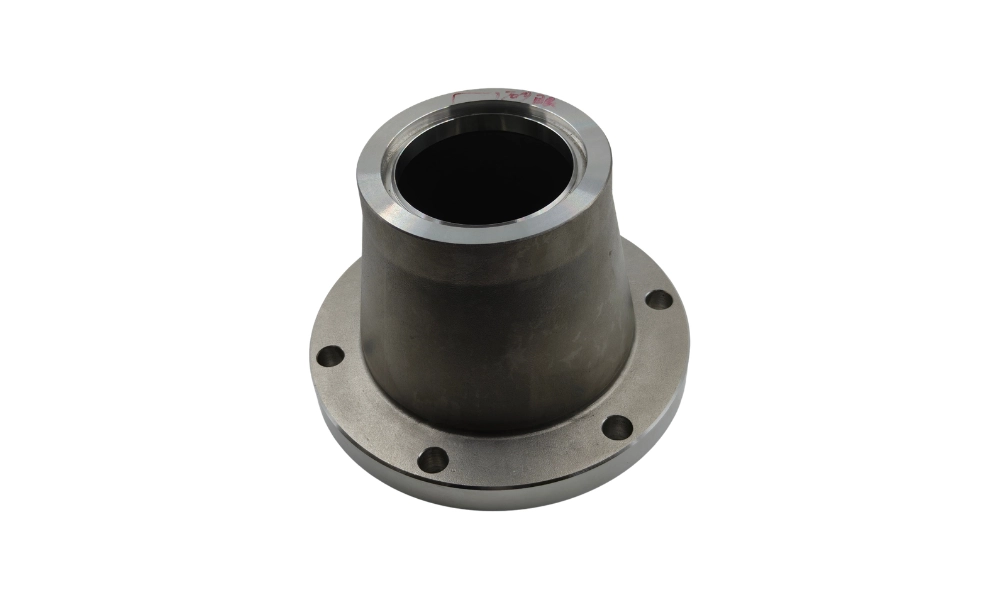
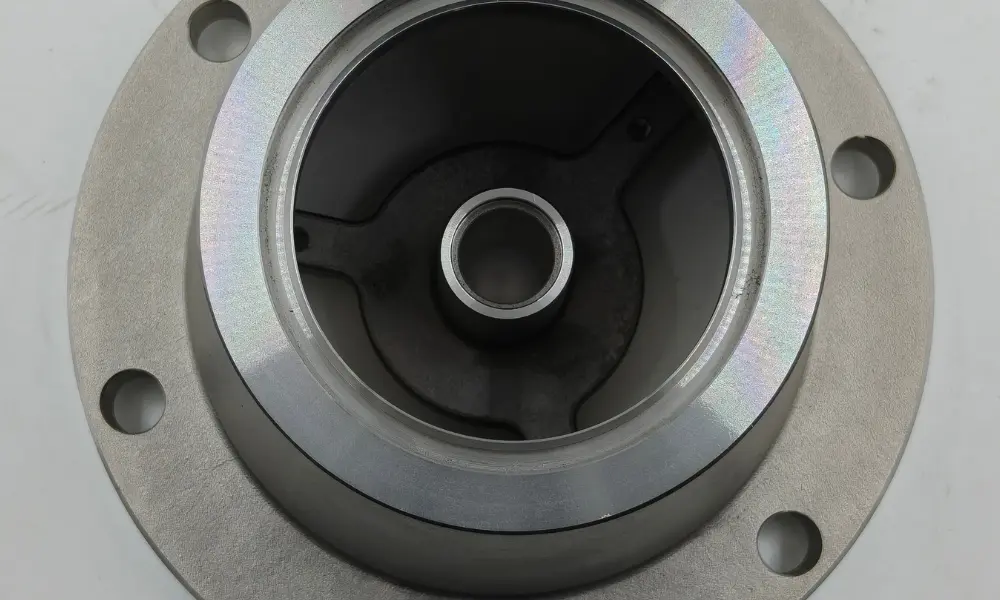
Tapered Body
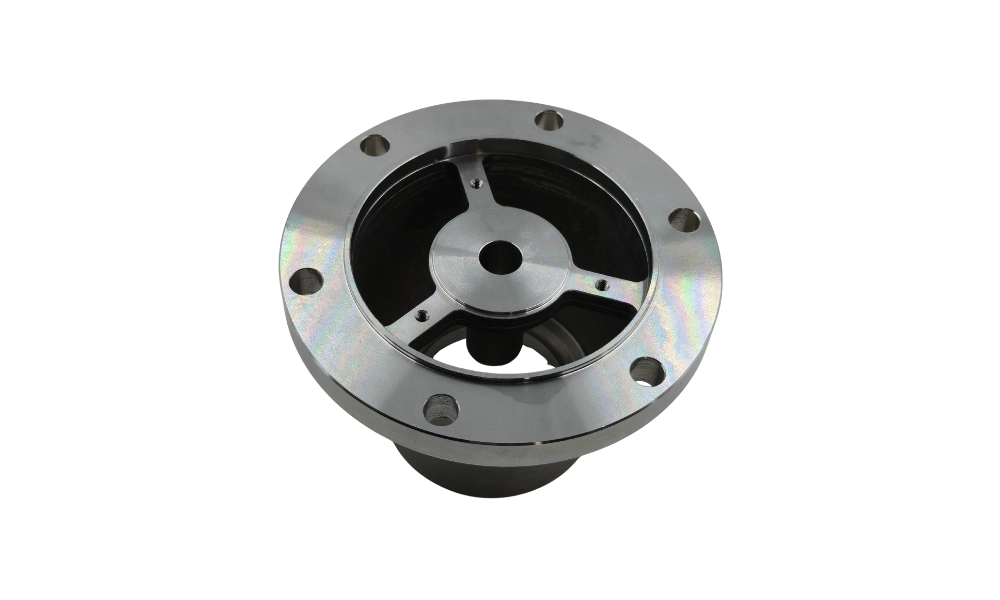
Internal Support
Customer Requirements & YTD’s Approach for Neck Flange
An integrated internal structure
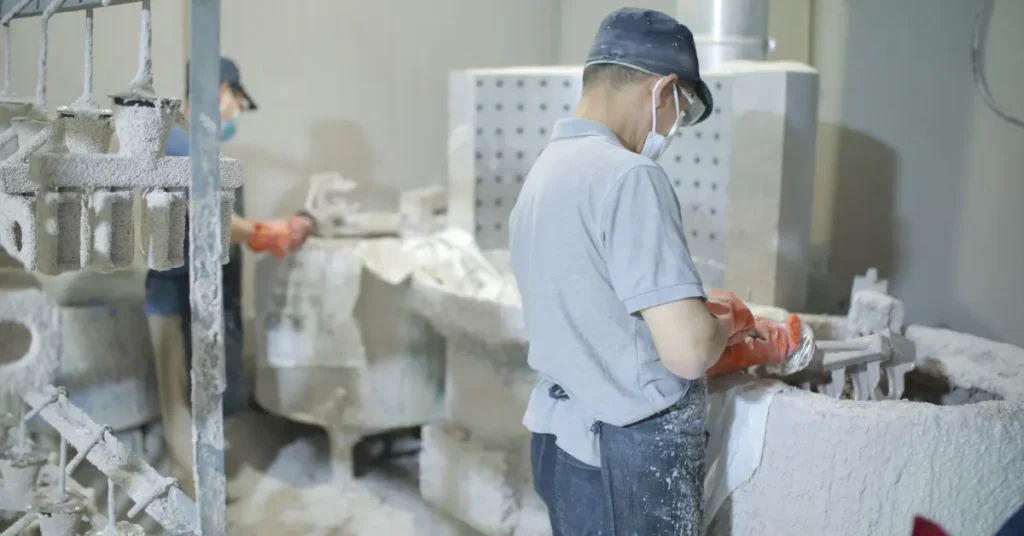
Produce the complete structure by investment casting.
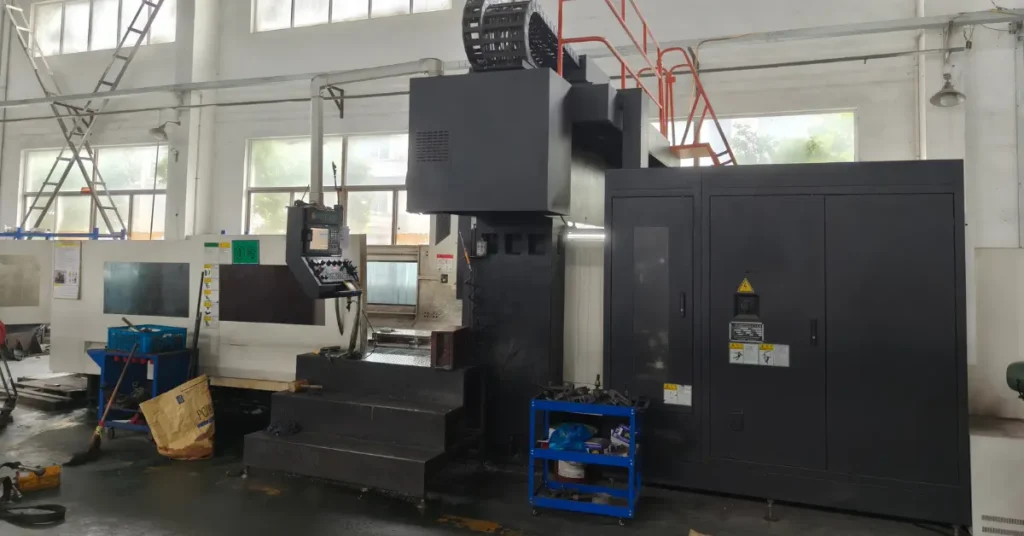
Machining included in the supply
Complete the assembly machining after casting.
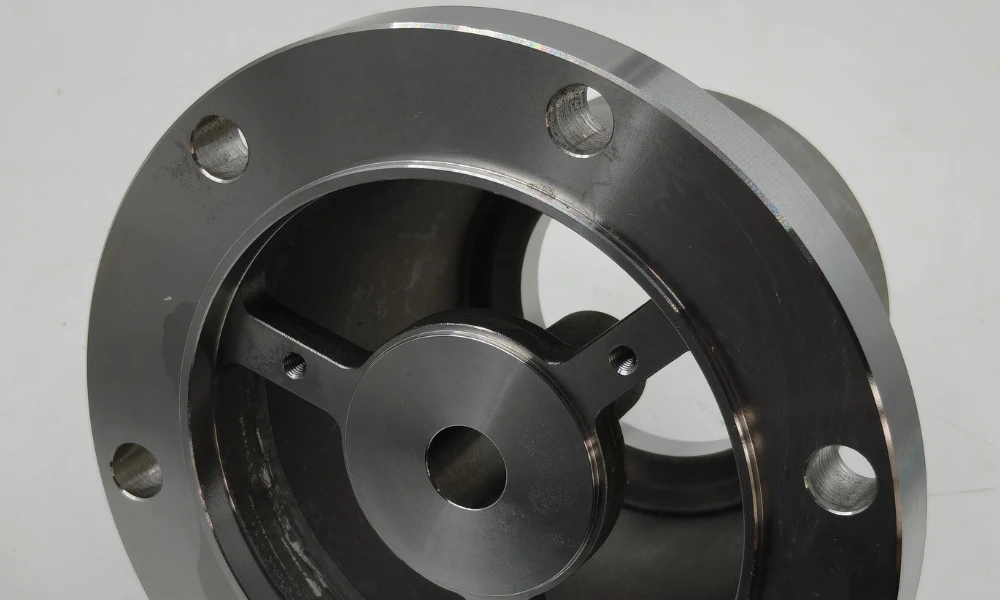
Forming a Cavity with Restricted Core Removal
The narrow-end rim projects into a larger internal cavity. A single rigid core matching that cavity cannot pass straight through the smaller opening. At the opposite end, the three ribs and central platform also obstruct a direct axial withdrawal path.
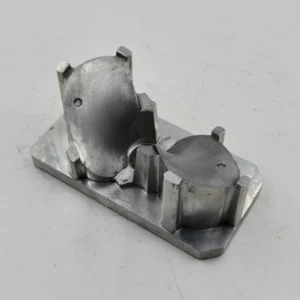
These restrictions made internal cavity formation and wax-pattern release central to the tooling design. The tooling had to reproduce the enclosed profile and connected support structure while allowing the wax pattern to be released without damage. Resolving this at the wax-pattern stage enabled the complete geometry to be carried through into the CF8M casting.
Machining Stepped Interfaces and Recessed Features
The large end contains three distinct levels: the annular ring stands above the flange mounting face, while the support ribs sit below it. YTD machined the mounting interface and its six holes, finished the central platform face, and produced one threaded hole in each rib.
At the narrow end, machining covered the complete end face and curved annular groove. The central sleeve’s through-bore was also machined. Together, these operations completed the component’s assembly features across both ends and inside the body.
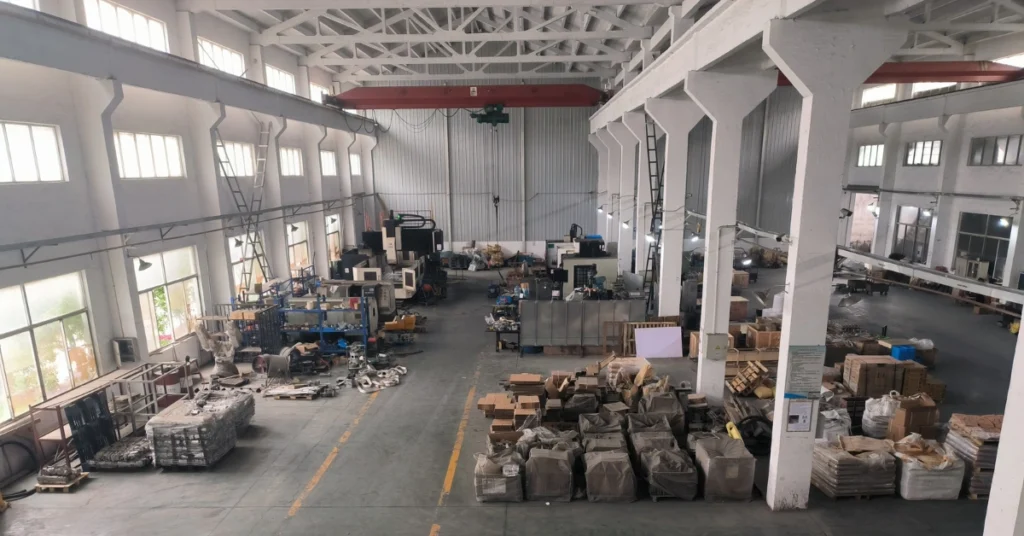
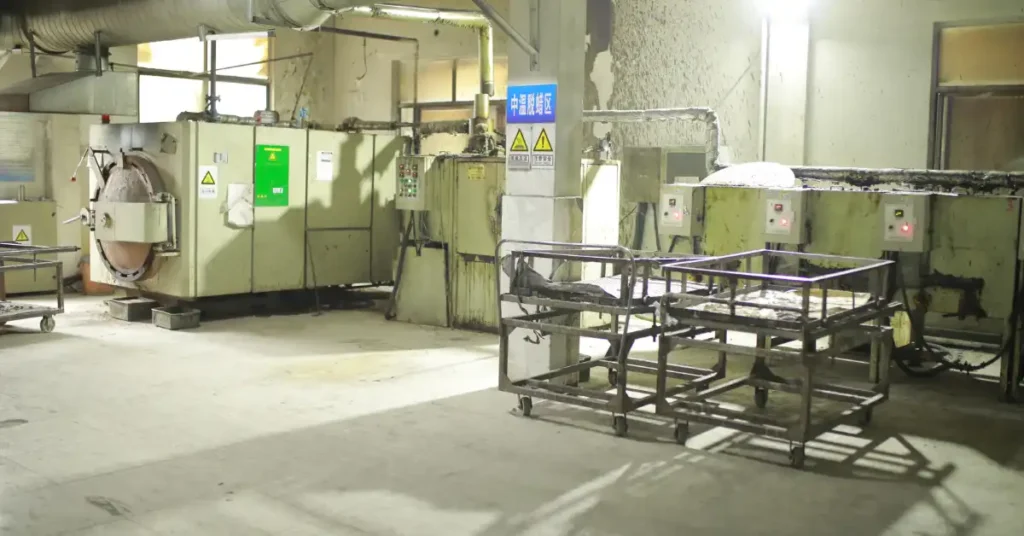
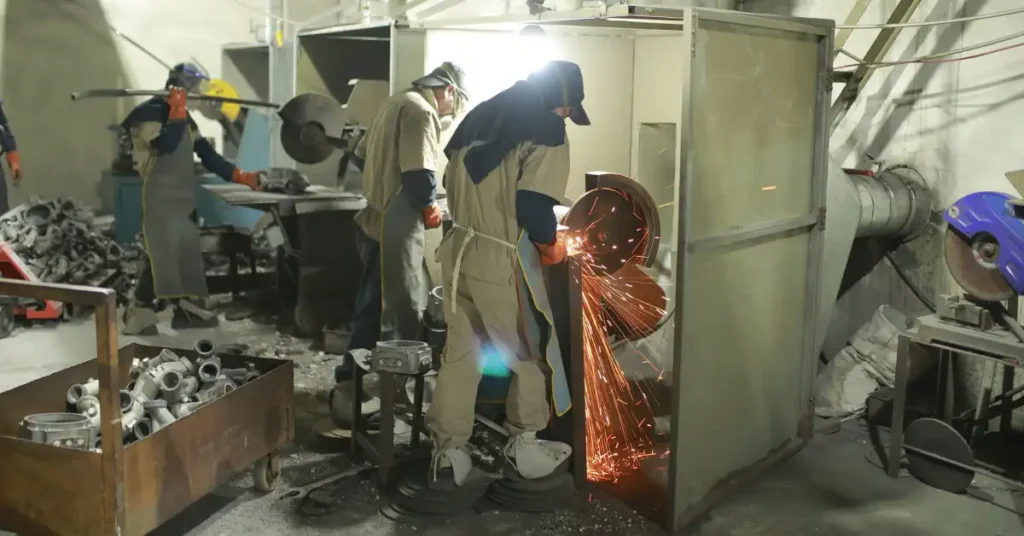
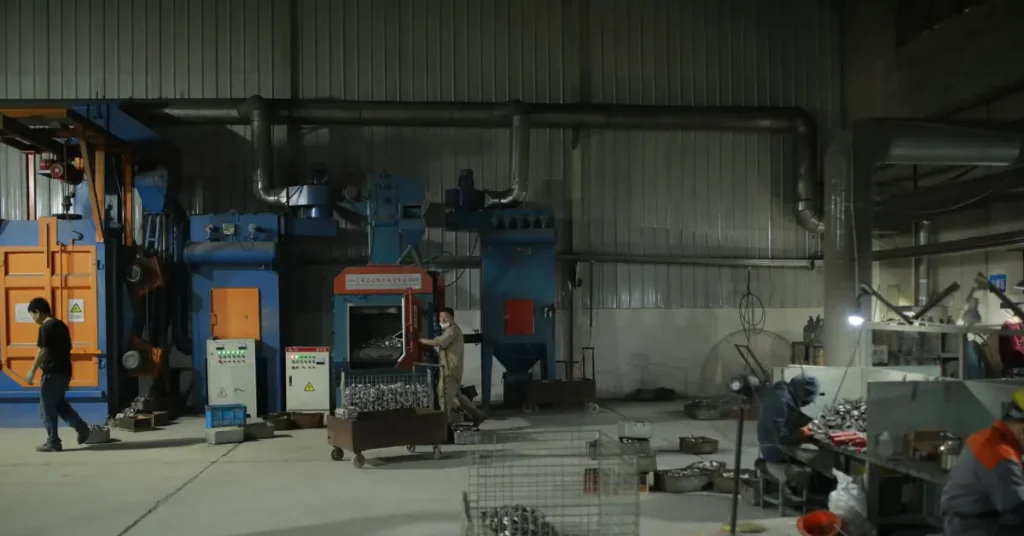
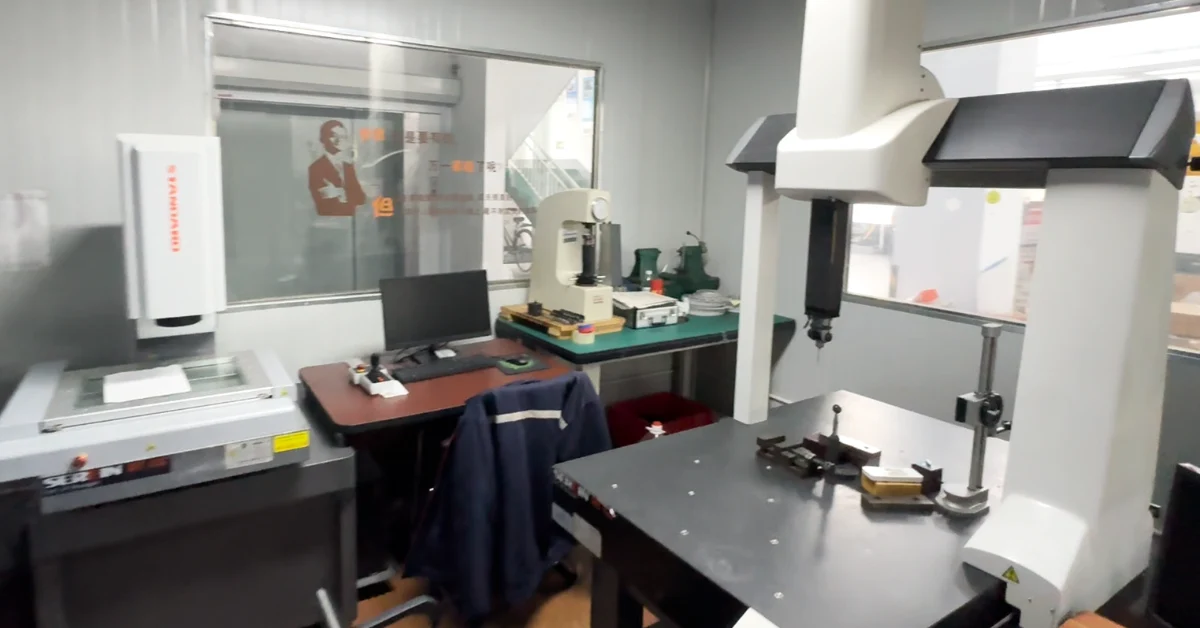
Inside Our Factory
Related Casting Projects
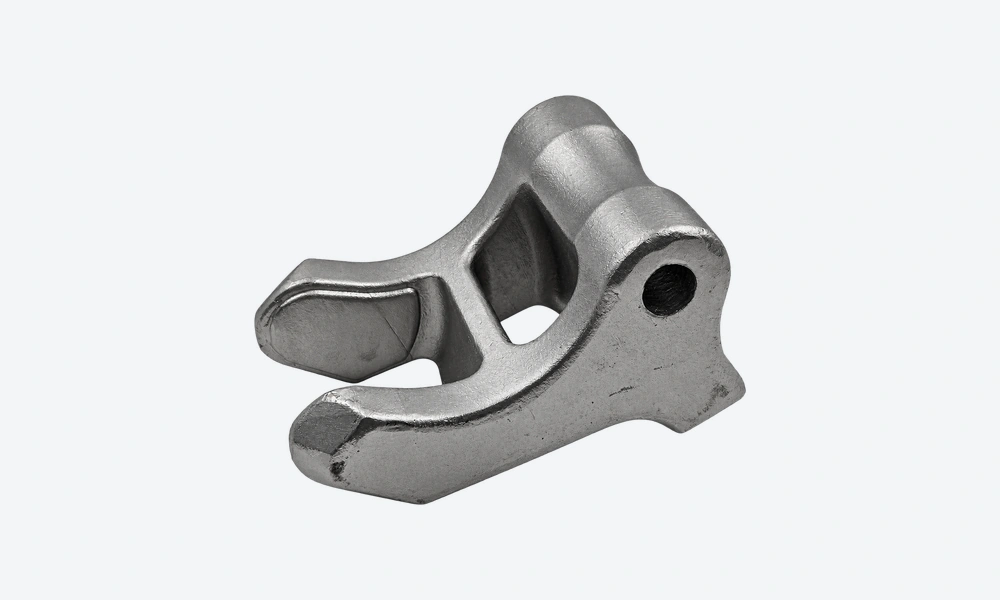
Stainless Steel Fork Casting with a Shot-Blasted Finish
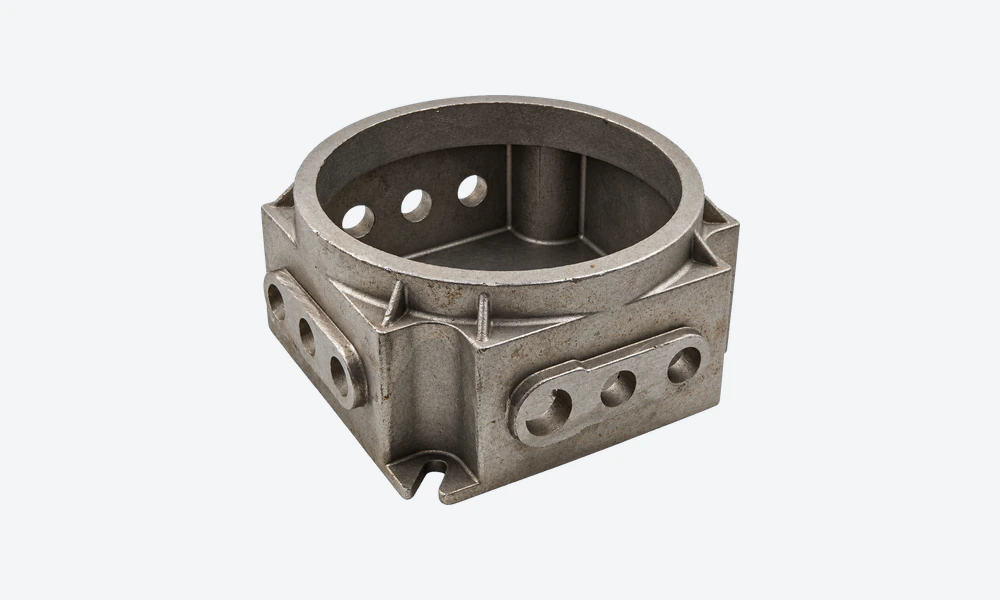
Carbon Steel Housing Casting with Side Openings
Stainless Steel Impeller Casting with Curved Vanes
CF8M Stainless Steel Threaded Housing with Cast Fins
Aluminum Fishing Reel Frame
CF8 Three-Way Pipe Fitting
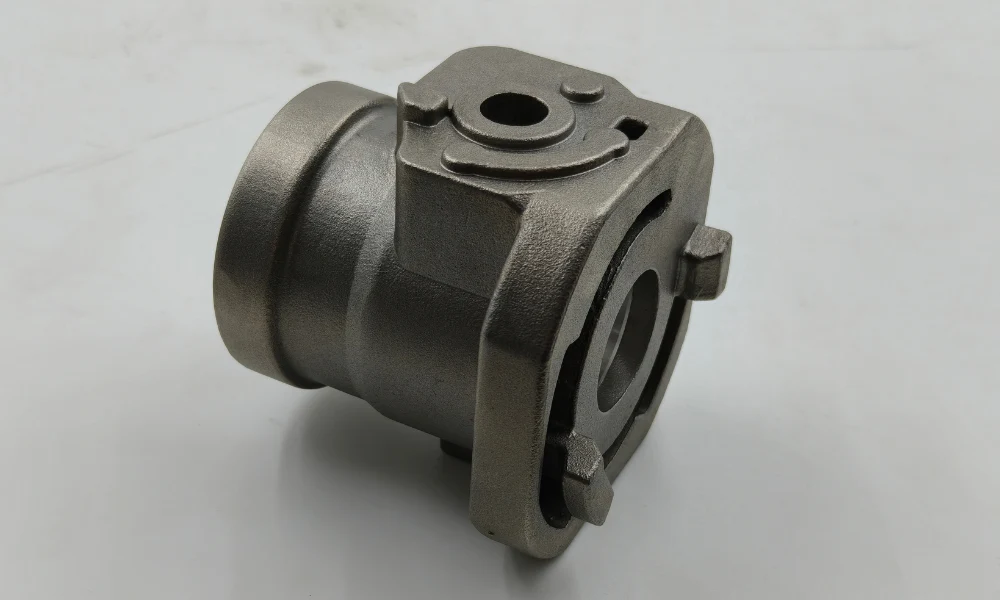
CF8 Quick-Connect Coupling Body
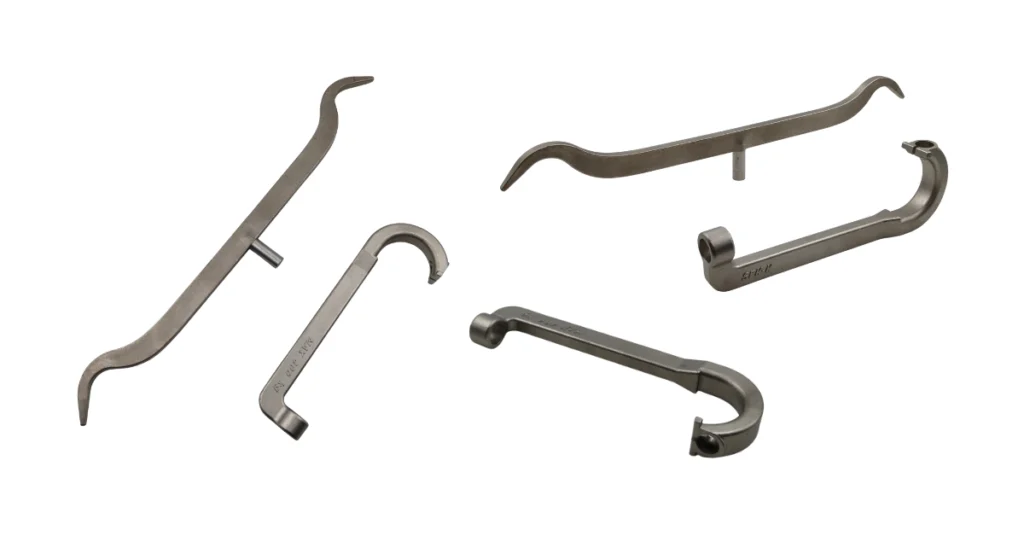
CF8M Carcass Hook
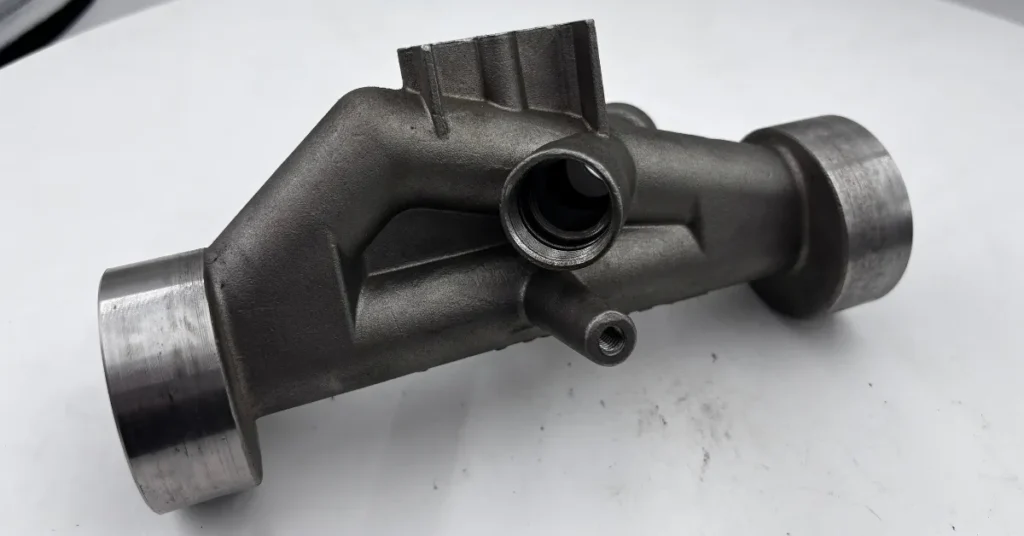
Stainless Steel Flow Meter Body
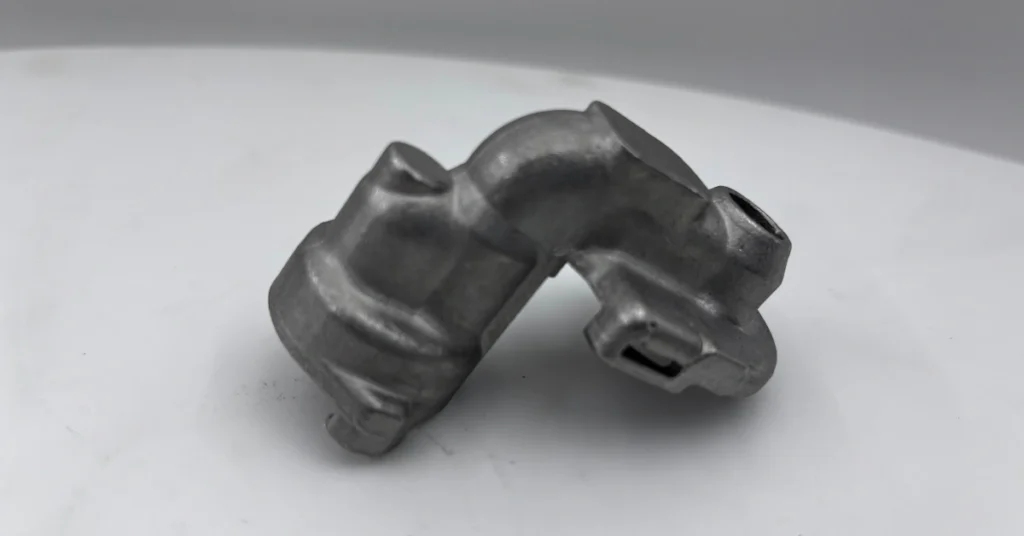
CF8M Pump Valve Body
Have a Casting with Complex Internal Features?
Share your drawing or 3D model, material specification, order quantity and machining requirements. YTD will review the internal geometry, tooling requirements and finishing scope for your project.