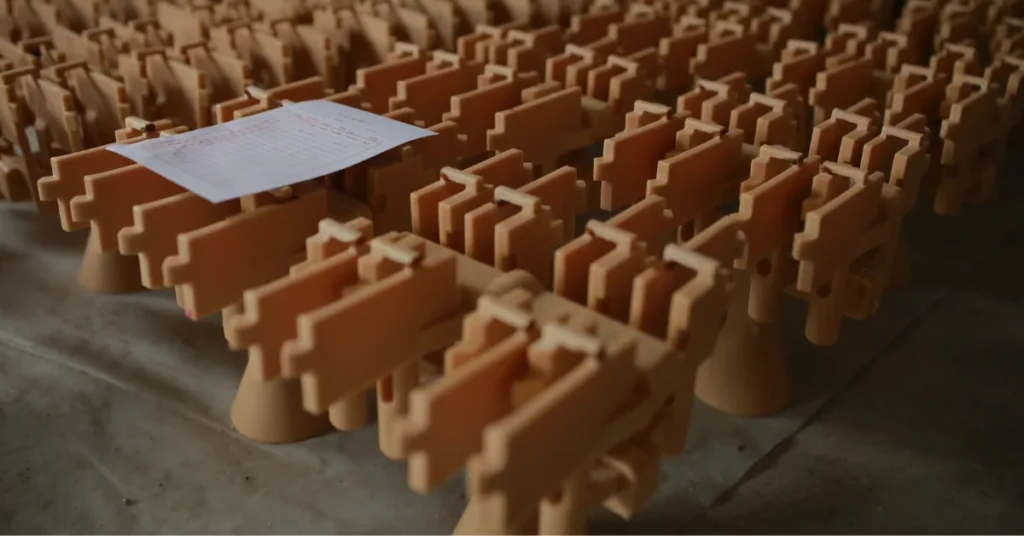
CustomInvestment Casting Service by YTD Foundry
Custom investment casting solution provider in China. OEM service from casting to post-processing, offering components ready for assembly.
ISO 9001 Certified
50+ Casting Materials
Global Customer Served
Design Support
YTD - Factory Dedicated to Investment Casting
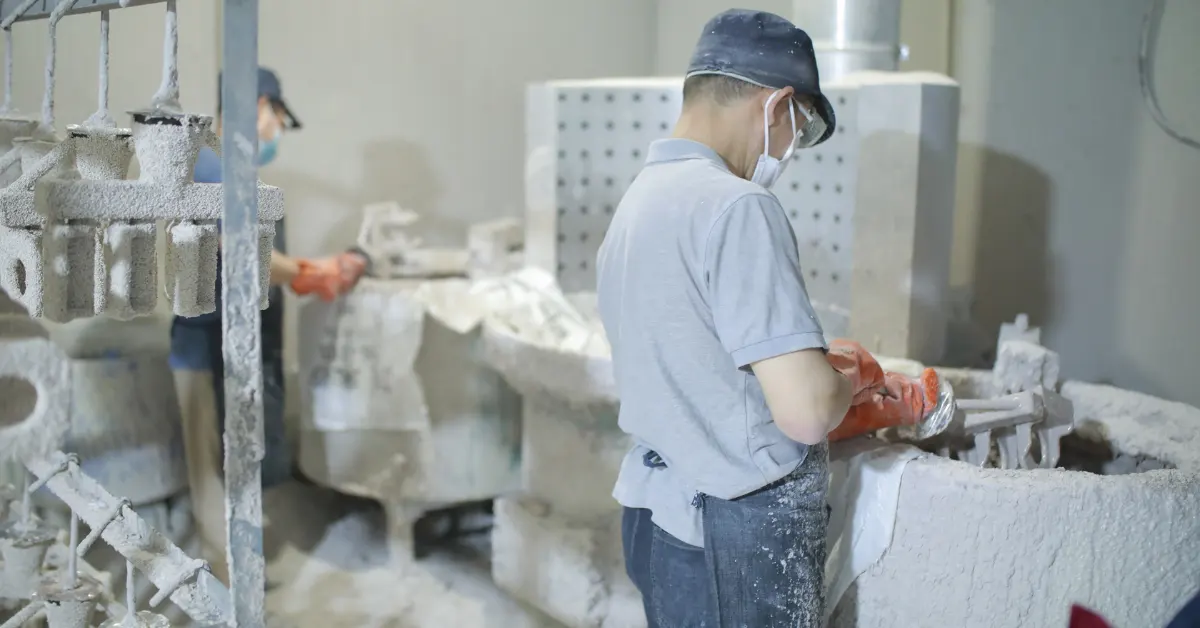
As a metal foundry, YTD has been focusing on the silica sol casting process for over 15 years. This lost-wax casting process allows us to cast metals in a wide range, spanning from aluminium to superalloys.
With our rich experience across thousands of casting projects, we offer comprehensive support to guide you through the whole project lifecycle, including design optimization, material selection, and post-processing.
Investment Casting Materials
Stainless Steel
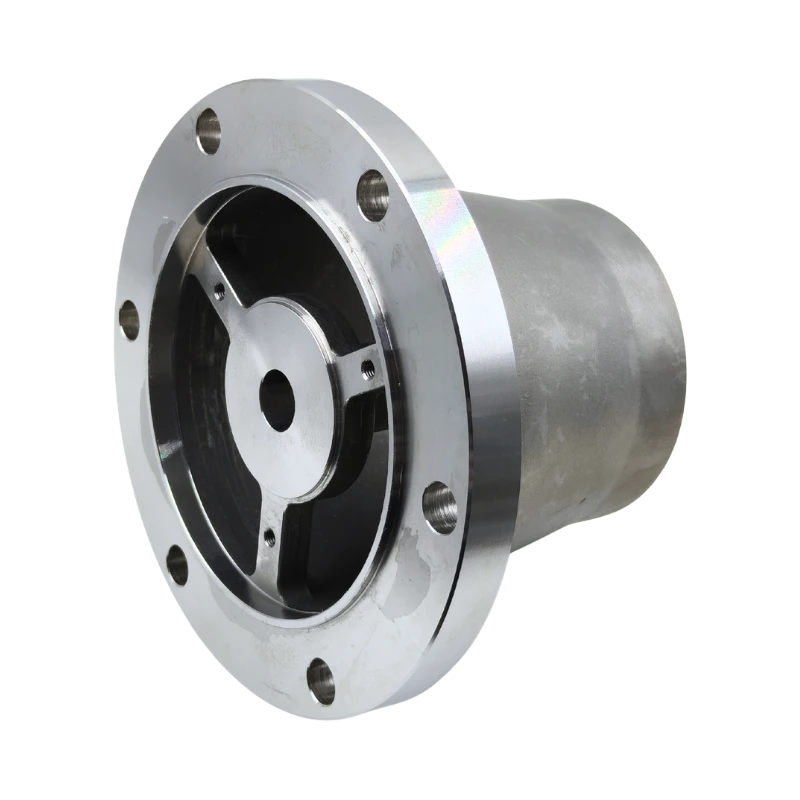
Stainless steel and investment casting are a natural pairing. Investment casting bypasses the work-hardening limitations of stainless steel and enables complex geometries that machining alone cannot achieve, making it the preferred production route for corrosion-resistant, high-strength stainless components. Stainless steel, such as CF8, CF8M, and CF3, is the most used material at YTD Foundry, accounting for almost half the products we cast.
Learn More
Carbon Steel
As the name suggests, carbon steel is mainly composed of carbon and steel. Based on the carbon content, it can be divided into low-carbon steel(< 0.25%), medium-carbon steel(0.25–0.60%), and high-carbon steel(> 0.60%). With low material cost, balanced performance, and good castability, carbon steel has become the preferred casting material for most non-special applications.
Learn More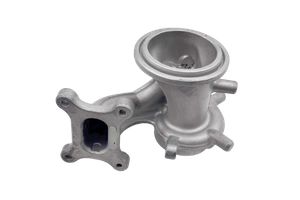
Alloy Steel
Alloy steel is a broad category of steels that incorporate additional alloying elements beyond carbon, including chromium, molybdenum, nickel, and manganese, to selectively enhance properties such as strength, hardness, and wear resistance. The common grades used in investment casting are 4140 and 4340.
Learn More
Superalloy
Superalloys are mostly designed for specific extreme applications, which is why they are "Super". As an investment casting expert, YTD offers a broad range of superalloys, which include nickel-based superalloys, cobalt-based superalloys, and iron-based superalloys. The most commonly cast are K418 for components operating above 950 °C and IN718 for high-precision structural parts where tensile strength and fatigue resistance are equally critical.
Learn More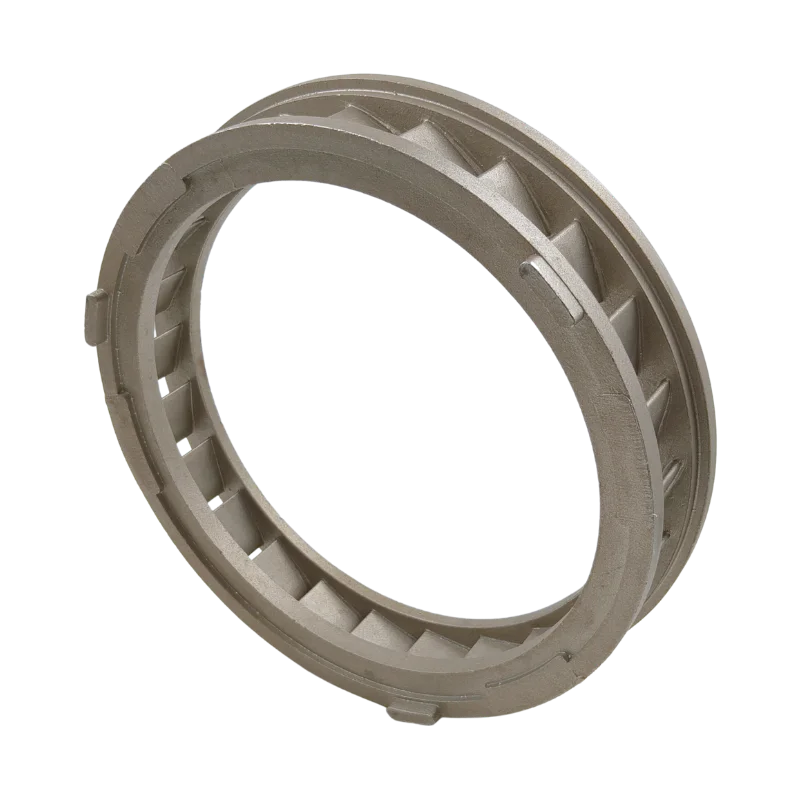
Aluminum
Aluminum is not a common material for investment casting. However, for components with complex geometries that cannot be die cast or economically machined from solid, investment casting offers a precise and cost-effective alternative, as demonstrated by our own production experience.
Learn More
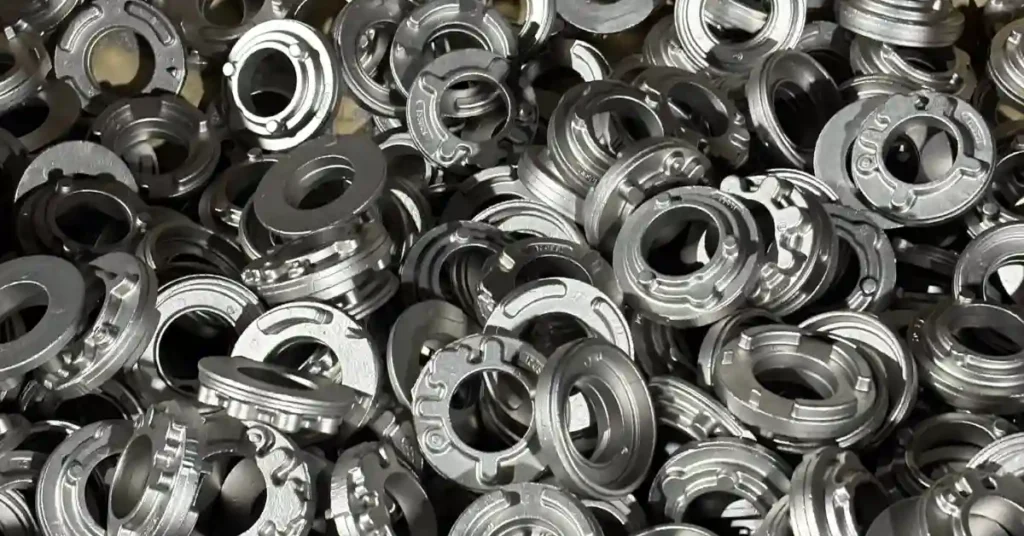
Need Material That's Not on The List?
Through our casting network and the collaboration with the IMR (Institute of Metal Research), the casting materials we can provide are not limited to the existed one. We can also configure alloys that are tailored to your application.
Request Customized MaterialInvestment Casting Capabilities
This general data is offered to help you get a quick understanding of our casting capabilities. Contact us for more project-specific data.
Dimensions & Weight
Parts of the data are strictly limited by our equipment parameters. Which is the max part envelope limited by the inner dimensions of our shell mold baking furnace, and the max weight limited by the capacity of our medium-frequency furnace. As for other restrictions, such as wall thickness and hole diameter, it is affected by multiple factors and need to evaluate the specific project to get accurate data.
| Iron-Based Alloys | Aluminum Alloys | Nickel-Based Alloys | |
|---|---|---|---|
| Max Part Envelope | 600 × 800 × 800 mm | 600 × 800 × 800 mm | 500 × 600 × 600 mm |
| Min. Wall Thickness | 1.5 mm | 1.0 mm | 1.5 mm |
| Max Pouring Weight | 250 kg | 250 kg | 100 kg |
Tolorances
Silica sol investment casting achieves tight as-cast tolerances typically within ±0.1–0.3 mm for small and medium-sized castings, depending on part geometry and material.
| Part Size | Tolorances | |
|---|---|---|
| As Cast Blanks | ≤25 mm (≤1″) | ±0.15 mm (±0.006″) |
| 25–100 mm (1–4″) | ±0.20–0.30 mm (±0.008–0.012″) | |
| 100–200 mm (4–8″) | ±0.30–0.50 mm (±0.012–0.020″) | |
| >200 mm (>8″) | ±0.5 mm | |
| CNC Machined — 4-axis (in-house) | ~ | ±0.05 mm |
| CNC Machined — 5-axis (via qualified partner) | ~ | ±0.02 mm |
Surface Roughness
Further surface treatment options including polishing, passivation, and coating are available. See our Surface Treatment section for details.
| Surface Roughness (Ra) | |
|---|---|
| As Cast — Shot Blasted | Ra 6.3 – 12.5 μm |
| As Cast — Sand Blasted | Ra 3.2 – 6.3 μm |
| CNC Machined — 4-axis | Ra 1.6 – 3.2 μm |
| NC Machined — 5-axis | Ra 0.8 – 1.6 μm |
Logo & Text
For logos and texts that need to be attached to the parts, we primarily provide three methods:
- Directly cast on the surface: This method needs to engrave the logo or text on the wax injection mold, both intaglio and relief carving are supported. This is also the most cost-effective and flexible way we suggest.
- Engraving: Engraving is typically applied on the outer surface, which is limited by the engraving machine and the part geometries. This will need an extra fee for each part.
- Laser Etching: This process is similar to engraving, but has more limitations. Surface treatment, such as polishing, will affect the result.
Dimensions & Weight
| Iron-Based Alloys | Aluminum Alloys | Nickel-Based Alloys | |
|---|---|---|---|
| Max Part Envelope | 600 × 800 × 800 mm | 600 × 800 × 800 mm | 500 × 600 × 600 mm |
| Min. Wall Thickness | 1.5 mm | 1.0 mm | 1.5 mm |
| Weight Range | 0.01 – 120 kg | 0.01 – 50 kg | 0.01 – 70 kg |
Tolorances
| Iron-Based Alloys | Aluminum Alloys | Nickel-Based Alloys | |
|---|---|---|---|
| Max Part Envelope | 600 × 800 × 800 mm | 600 × 800 × 800 mm | 500 × 600 × 600 mm |
| Min. Wall Thickness | 1.5 mm | 1.0 mm | 1.5 mm |
| Weight Range | 0.01 – 120 kg | 0.01 – 50 kg | 0.01 – 70 kg |
Surface Roughness
| Surface Roughness (Ra) | |
|---|---|
| As Cast — Shot Blasted | Ra 6.3 – 12.5 μm |
| As Cast — Sand Blasted | Ra 3.2 – 6.3 μm |
| CNC Machined — 4-axis | Ra 1.6 – 3.2 μm |
| NC Machined — 5-axis | Ra 0.8 – 1.6 μm |
Logo & Text
For logos and texts that need to be attached to the parts, we primarily provide three methods:
- Directly cast on the surface: This method needs to engrave the logo or text on the wax injection mold, both intaglio and relief carving are supported. This is also the most cost-effective and flexible way we suggest.
- Engraving: Engraving is typically applied on the outer surface, which is limited by the engraving machine and the part geometries. This will need an extra fee for each part.
- Laser Etching: This process is similar to engraving, but has more limitations. Surface treatment, such as polishing, will affect the result.
Post Processing on Castings
Get precision-cast, surface-finished parts ready for end use. You only need to deal with one supplier to get it all done.
Request a QuoteOur Foundry Capabilities
- CNC Finishing
- Heat Treatment
- Sand/Bead Blasting
- Polishing
Through Our Network
- Powder Coating
- Galvanizing
- Electroplating
- Anoadizing
From Drawing Review to Finished Components
Engineering and Tooling
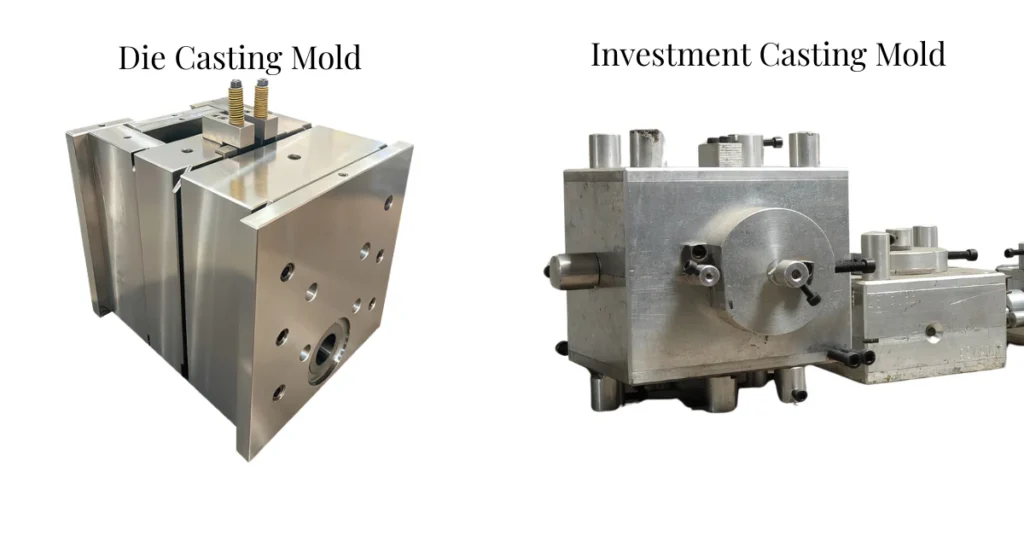
Before tooling begins, we review the part for castability, material requirements and features that may affect quality or cost. Our in-house tooling capability supports wax-pattern production for investment casting.
For suitable prototype projects, 3D-printed wax patterns can provide a route without conventional injection tooling. The pattern method, development cost and schedule are assessed for your design and quantity.
Casting and CNC Machining
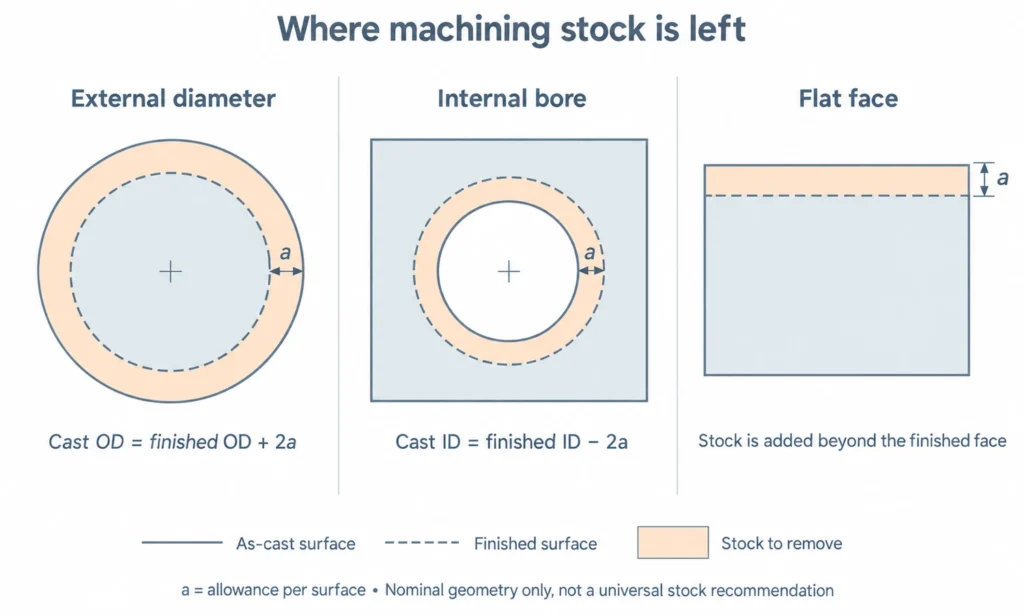
Silica-sol investment casting produces the main part geometry. CNC machining then completes the bores, threads, mounting faces and other features specified for closer dimensional control.
We coordinate the casting and machining requirements in one project, so the drawing and delivery condition provide a common reference through production.
Heat Treatment and Surface Finishing
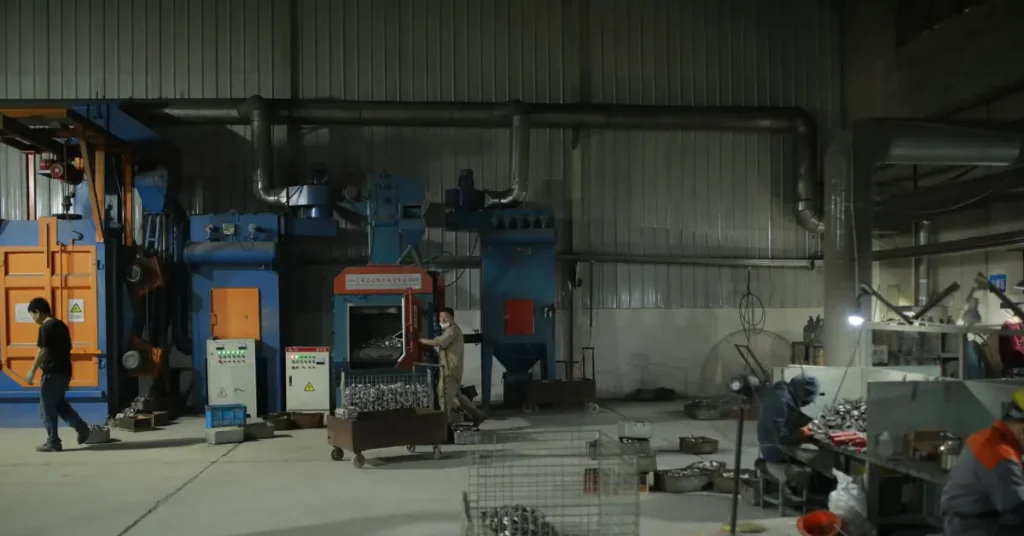
Our in-house capabilities include heat treatment, sand or bead blasting and polishing. Additional finishing, including coating and plating, can be arranged through our supplier network where appropriate to the material and application.
Cast-in identification, engraving and laser marking can also be reviewed when your part requires a logo, text or traceability marking.
End-to-End Investment Casting Service
We don't just do casting. YTD is a foundry that provides turnkey casting solutions. Specify your requirements, and we'll turn them into precision-cast and surface-finished components.
Get a QuoteEngineering & Tooling Support
We solve every problem on your way to a finished casting,engineering review, tooling, and production managed under one roof.
Get an Expert ReviewDFM Review
Tooling Fabrication
Inspection Planned Around Your Requirements
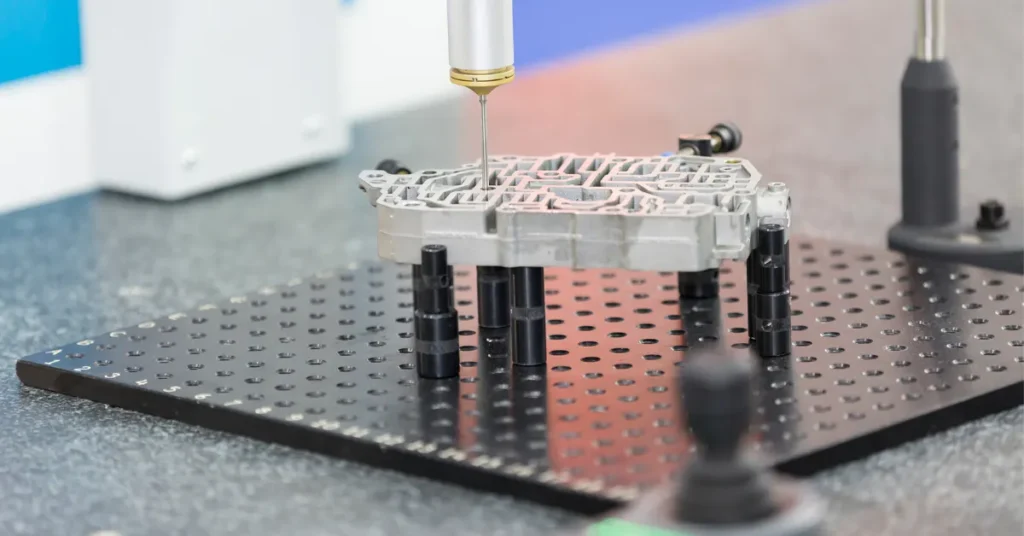
Quality planning begins with tooling and process review. Casting simulation and wax-pattern inspection help address potential manufacturing issues before the finished casting is produced.
Available checks include chemical composition, hardness, tensile testing and dimensional inspection, including CMM measurement where required. Fluorescent penetrant, X-ray, ultrasonic and salt-spray testing can be considered according to the material, geometry and specified inspection needs.
The inspection method, coverage, acceptance criteria and reporting requirements are agreed for the order. Material and inspection reports can be provided for the tests included in that scope.
YTD’s ISO 9001 quality management system supports project control alongside these part-specific checks.
Applications Supported by YTD Casting Service
Rapid Prototyping
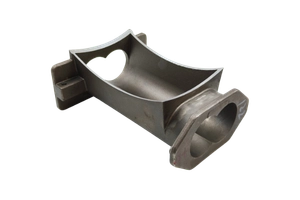
Part Consolidation
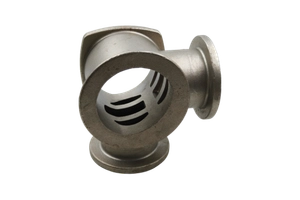
Reduce Costs
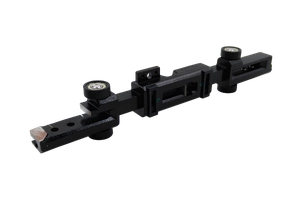
End-Use Production
How Your Project Moves into Production
Share Your Part Requirements
Review the Manufacturing Proposal
Develop and Review Samples
Approve the Production Reference
Produce, Inspect and Deliver
Request a Quote Now
Investment Casting Service FAQs
Address common questions you may have about investment casting and our casting service
Can I start without a complete drawing?
Yes. A model, sample details or photos can help start the discussion. We will clarify the information needed and agree the drawing and material requirements before manufacture.
Can you supply machined parts as well as castings?
Yes. In-house CNC machining can be combined with investment casting, heat treatment and finishing. Send the required delivery condition and identify the critical dimensions or assembly features.
How are tooling costs and lead times determined?
Tooling requirements are assessed from the geometry, pattern method and order quantity. The quotation confirms development costs and the planned timing for tooling, samples and production.
Is every operation completed at your own factory?
Silica-sol investment casting, tooling and core machining are managed through our in-house capabilities. Selected operations, such as 5-axis machining and additional surface finishing, are coordinated through qualified partners. We confirm the production scope for your order.
How do you inspect investment casting parts?
Chemical composition is verified by OES spectrometry. Dimensional inspection covers critical features per drawing. Mechanical testing available on request. Full material certifications and inspection reports provided with shipment.
What's your typical MOQ for investment casting parts?
No fixed MOQ. We run prototypes as single pieces and scale to production volumes. Economical batch size depends on part complexity and material — our team will advise during quoting.
Do you accept prototype and small-batch projects?
We review prototype, small-batch and production enquiries. The tooling or pattern route and economical quantity depend on the material and part design. Share the sample quantity and expected production demand when available.
Can you provide material and inspection reports?
Yes. Reports are available for the tests agreed for the order. Include any required standard, acceptance criteria, inspection coverage or report format with your enquiry.