Investment casting does not have a meaningful universal price per kilogram or per part.
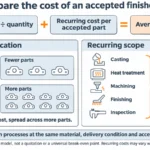
The quote includes more than molten metal. Tooling, wax patterns, ceramic shells, gating metal, melting, heat treatment, cut-off, machining, finishing, inspection, and production quantity can all change the final cost.
For buyers, the useful question is not simply “How much does investment casting cost?” It is which parts of the manufacturing route are driving the price, and which of those costs can be reduced without weakening the finished component.
What Does Investment Casting Cost?
As a current YTD reference, our investment-casting tooling typically starts at around USD 1,000, while many custom cast parts fall roughly in the USD 5–40 per-piece range. These are not fixed industry prices or limits; they are reference figures from our current project mix. Material, weight, geometry, quantity, machining, finishing, and inspection can move a project well outside that range.
A small carbon-steel bracket made in repeat quantities and a large nickel-superalloy component requiring vacuum melting, machining, and X-ray inspection are both “investment castings,” but their cost structures are completely different.
That is why a useful quotation starts with a drawing, material specification, and quantity rather than only finished part weight.
Investment Casting Cost Structure: One-Time and Recurring Costs
Investment casting cost becomes easier to understand when the project is separated into fixed and recurring expenses.
One-time or project-level costs can include tooling design, wax-pattern tooling, ceramic-core tooling where required, process development, first-article work, and some dedicated fixtures or gauges.
Recurring costs include each wax pattern, tree assembly, ceramic shell building, alloy, melting and pouring, shell removal, gate cut-off, heat treatment, finishing, machining, inspection, and packaging.
A simplified way to think about unit cost is:
tooling amortization + casting production + secondary operations + inspection
The balance changes with quantity.
At low volume, tooling can represent a large share of the cost per part. Once the same tool produces hundreds or thousands of pieces, tooling becomes a much smaller part of each unit and material, labor, machining, and quality requirements become more important.

Wax Tooling Cost and Prototype Pattern Options
Production investment casting normally begins with reusable wax-pattern tooling.
Tool size, cavity count, parting structure, inserts, slides, dimensional requirements, and ceramic-core positioning features all affect the amount of design and machining required.
At YTD, smaller and higher-precision tools are commonly CNC-machined directly from aluminum. For suitable large tools with lower overall precision requirements, we can first create the bulk tool shape using lost-foam casting and then CNC-machine the cavity and critical interfaces.
Those routes have different cost structures, which is why mold price cannot be estimated reliably from finished casting weight alone.
For prototype quantities, hard tooling can sometimes be removed from the project entirely.
A sacrificial pattern can be 3D printed directly from the CAD model and used to build the ceramic shell. Investment Casting Institute research notes that printed patterns are widely used for prototype and low-volume work, while conventional tooling becomes more economical once repeated quantity spreads the initial tooling cost. For many castings, its reported printed-pattern cost break-even is roughly 10–50 pieces, although actual crossover quantity changes with pattern size and complexity.
At YTD, we use the same principle: printed sacrificial patterns are useful for prototypes and small batches, while stable repeat production normally moves toward conventional tooling and injected wax patterns.
Investment Casting Mold and Tooling Guide
Material Grade, Part Weight, and Casting Yield
Material cost begins with the alloy, but finished part weight is not the amount of metal the foundry has to melt.
The complete pour also contains sprues, runners, gates, and other feeding metal.
A 5 kg finished casting may therefore require considerably more than 5 kg of molten alloy.
This matters much more when the metal itself is expensive.
Carbon steel, stainless steel, and nickel- or cobalt-based superalloys have very different raw-material and melting costs. Suitable superalloys may also require vacuum induction melting, adding equipment and process cost beyond ordinary air melting.
Casting yield describes how much of the poured metal becomes usable casting:
Casting Yield = Good Casting Weight ÷ Total Pour Weight
For small parts assembled on a wax tree, the central sprue and gates can weigh more than all the finished parts combined. Larger single castings can have a much higher product-to-gating ratio.
Low yield therefore increases alloy consumption per acceptable part even if the gates are later recycled or remelted.
The design goal is not maximum theoretical yield at any cost. Gates still need to fill and feed the component correctly. A lighter gating system that raises scrap can increase total cost rather than reduce it.

Casting Yield: Part Weight, Pour Weight & Gating
Part Geometry, Tree Layout, and Ceramic Cores
Investment casting is often chosen because complicated geometry can be produced close to final shape.
That does not mean complexity is free.
A simple component that fits many times on one wax tree uses shell-building and furnace capacity differently from a large part that requires its own tree.
Part geometry can change cost through:
- the number of patterns that fit on each tree
- gate and runner size
- shell-building access
- cut-off difficulty
- straightening or grinding
- ceramic cores for internal passages
Ceramic cores deserve particular attention. A component with a curved or enclosed internal passage may need separate core tooling, core production, positioning inside the wax pattern, and core removal after casting.
That adds cost, but the alternative might be several machined parts, welding, or an internal shape that cannot be produced economically by another method.
This is an important distinction in investment-casting economics: geometry can make the casting more expensive while still making the finished component much cheaper.
Tolerances, Surface Finish, and CNC Machining Cost
Investment casting provides good near-net-shape accuracy, but applying tight tolerances to every dimension is one of the easiest ways to increase cost unnecessarily.
Some features can remain as cast.
Others—bearing bores, sealing surfaces, precision threads, or critical datums—may need CNC machining.
The cost impact depends on how much machining the drawing forces into the production route.
A precision bore may require machining stock, a fixture, one or more CNC operations, tool changes, dimensional inspection, and possibly an additional setup after heat treatment.
A surface that can remain as cast avoids all of that.
Machining allowance also affects the raw casting itself. Too little stock creates a risk that the machined surface will not clean up. Too much adds alloy weight and unnecessary cutting time.
At YTD, casting and CNC machining are both part of our in-house investment-casting workflow, so we can review the raw casting and final machining requirements together rather than treating them as unrelated operations.
Investment Casting Machining Allowance Guide
Heat Treatment, Vacuum Melting, Finishing, and Inspection
The raw casting price is not always close to the final part price.
A drawing may also require heat treatment, blasting, polishing, machining, passivation, plating, painting, pressure testing, penetrant inspection, radiography, or mechanical testing.
Each requirement adds a real operation.
Heat treatment cost changes with alloy, cycle, batch size, and handling requirements.
Vacuum melting adds specialized equipment and process control for suitable nickel-, cobalt-, and iron-based superalloys. It should be specified because the alloy needs it, not simply because vacuum sounds like a higher-grade casting process.
Inspection can also have a substantial effect on cost.
A visual and dimensional inspection plan is very different from 100% fluorescent penetrant inspection plus radiography, tensile testing, chemistry reports, and serialized traceability.
The right quality plan verifies what the part actually needs. Specifying every available test does not automatically create a better component.
Vacuum Investment Casting Guide
Casting Inspection Methods Guide
Order Quantity and Tooling Amortization
Quantity affects more than tooling cost.
At low volume, the tooling charge is divided among relatively few parts. Setup, furnace, shell-building, inspection, and production planning also have fewer pieces across which to spread their fixed effort.
As quantity rises, several efficiencies become possible.
More wax patterns can be produced from the same approved tool. Production trees can be standardized. Shell batches, furnace loads, machining fixtures, and inspection routines can be run repeatedly instead of being set up for a handful of pieces.
But investment casting does not suddenly become cheap at one universal quantity.
Part size and geometry change the economics.
A complex stainless impeller can justify tooling at a much lower quantity than a simple cylindrical component that can be turned directly from bar stock.
For prototype and early validation work, printed sacrificial patterns can avoid permanent tooling. Once the design stabilizes, conventional wax tooling normally becomes more economical for repeat orders.
The relevant number is therefore expected lifetime production, not only the first purchase order.
Scrap, Rework, and Process Stability
A quotation also has to account for the number of good parts expected from production.
If a casting has a high risk of non-fill, shrinkage, shell damage, distortion, or difficult dimensional correction, the foundry may need more process development, more inspection, or a higher expected scrap allowance.
Those costs do not always appear as a separate line item. They are built into the production economics.
This is why a design change that makes the casting easier to fill or reduces an isolated heavy section can save more money than negotiating a slightly lower alloy price.
For suitable difficult components, we use casting simulation during tooling and process development to study filling, solidification, hot spots, and gating before the production route is finalized.
Reducing avoidable trial-and-error and scrap is a real cost-control measure, not only a quality improvement.
Investment Casting Defects Guide
Investment Casting Cost vs. Other Manufacturing Routes
Investment casting should not be chosen simply because its tooling is cheaper than die casting or because its surface is better than sand casting.
Its economic advantage appears when the near-net shape removes expensive work elsewhere.
Investment Casting vs. Machining From Solid
A simple block, shaft, or cylinder may be cheaper to machine directly, especially at very low quantity.
Investment casting becomes more attractive when machining would remove large amounts of expensive material or require many setups to create curved surfaces, ribs, bosses, internal passages, or difficult three-dimensional geometry.
Casting vs Machining Guide
Investment Casting vs. Sand Casting
Sand casting usually starts with lower tooling and mold-process cost and becomes especially attractive for large components.
Investment casting can justify a higher casting price when its finer surface, closer dimensions, and more complex geometry remove machining and finishing.
Sand Casting vs Investment Casting Guide
Investment Casting vs. Die Casting
Investment casting normally has a lower permanent-tooling commitment but more recurring processing in each part.
Die casting places much more money into the steel die and becomes powerful when a suitable non-ferrous design is stable enough to run at very high lifetime volume.
Investment Casting vs Die Casting Guide
The correct comparison is always the finished component, not the raw casting alone.
How to Reduce Investment Casting Cost
The best cost reductions normally come from removing manufacturing work rather than simply negotiating a lower piece price.
Keep Tight Tolerances Where They Affect Function
A sealing face or bearing bore may genuinely need machining-level control.
A non-critical outside contour often does not.
Relaxing unnecessary tolerance does not reduce quality; it prevents the foundry from spending money controlling a dimension that does not affect the product.
Separate As-Cast and Machined Features
Define which surfaces can stay as cast and which must be machined.
This allows tooling and machining stock to be designed intentionally rather than leaving excessive material everywhere.
Stabilize the Design Before Production Tooling
Early design changes are inexpensive in CAD.
They become more costly after tooling, wax trials, fixtures, and inspection gauges have been created.
For an unstable design, a 3D-printed sacrificial pattern may be a better development route before conventional tooling.
Review Part Consolidation
Investment casting can sometimes combine several machined, welded, or assembled components into one casting.
The casting itself may be more expensive, but removing fasteners, welding, machining setups, assembly labor, and additional inspections can lower total product cost.
Provide Realistic Quantity Information
Tooling, cavity count, tree layout, machining fixtures, and production planning all depend on expected demand.
A quote for 50 pieces and a quote for 5,000 pieces should not be built around the same assumptions.

How to Compare Investment Casting Quotes
Two suppliers can quote the same drawing and still include different manufacturing scopes.
Before comparing unit price, check whether both quotations include the same:
- material grade and heat-treatment condition
- tooling and tool ownership
- machining
- surface finishing
- inspection and certification
- packaging
- order quantity and annual volume
A quote for raw castings should not be compared directly with a quote for finished machined parts.
Tooling should also be separated from recurring piece price. This makes it easier to see how the economics change after the initial order.
The Investment Casting Institute’s purchasing guidance specifically recommends careful review of tooling quotations, realistic quality requirements, and clear communication between buyer and foundry because hidden or poorly defined requirements can create avoidable cost later in the program. (Investment Casting Institute — 71st Technical Conference Proceedings)
Final Thoughts
Investment casting cost comes from the complete manufacturing route, not just the weight of the finished metal part.
Tooling dominates some low-volume projects. Alloy and casting yield matter more when the material is expensive. Tight tolerances, machining, heat treatment, finishing, and inspection can add more cost than the raw casting itself.
The most useful cost review therefore starts with the finished drawing and lifetime quantity, then identifies which operations are truly necessary and which can be designed out.
FAQs
How Much Does Investment Casting Cost Per Part?
There is no universal piece price. As a current YTD reference, many custom parts fall around USD 5–40 each, but material, weight, quantity, geometry, machining, finishing, and inspection can move the price substantially outside that range.
How Much Does Investment Casting Tooling Cost?
At YTD, a typical investment-casting mold currently starts at around USD 1,000. Large, multi-cavity, high-precision, or core-intensive tooling costs more because it requires additional material, machining, inserts, or core equipment.
Is Investment Casting Expensive?
It can have a higher raw casting cost than simpler molding processes because every part requires a wax pattern and ceramic shell. It becomes economical when near-net geometry removes enough machining, fabrication, assembly, or material waste from the finished component.
Is Investment Casting Cheaper at Higher Quantities?
The per-part cost generally falls as tooling and setup effort are spread across more pieces and production becomes more repetitive. Material, shell building, pouring, finishing, and machining remain recurring costs, so the unit price does not fall indefinitely.
Is Investment Casting Cheaper Than CNC Machining?
For simple low-volume geometry, machining can be cheaper because it avoids casting tooling. Investment casting becomes more competitive when the part would require substantial material removal, multiple setups, or difficult three-dimensional machining.
Can I Avoid Tooling Cost for a Prototype?
Often, yes. A suitable sacrificial pattern can be 3D printed directly from CAD and used to build the ceramic shell. ICI research places the tooling-versus-printed-pattern cost crossover for many castings around 10–50 pieces, although actual economics depend on pattern size and complexity.