Post CNC Machining for Casting Projects
We combine reliable casting expertise with precision CNC machining to deliver complete metal components ready for your application.
CNC Machining Capabilities
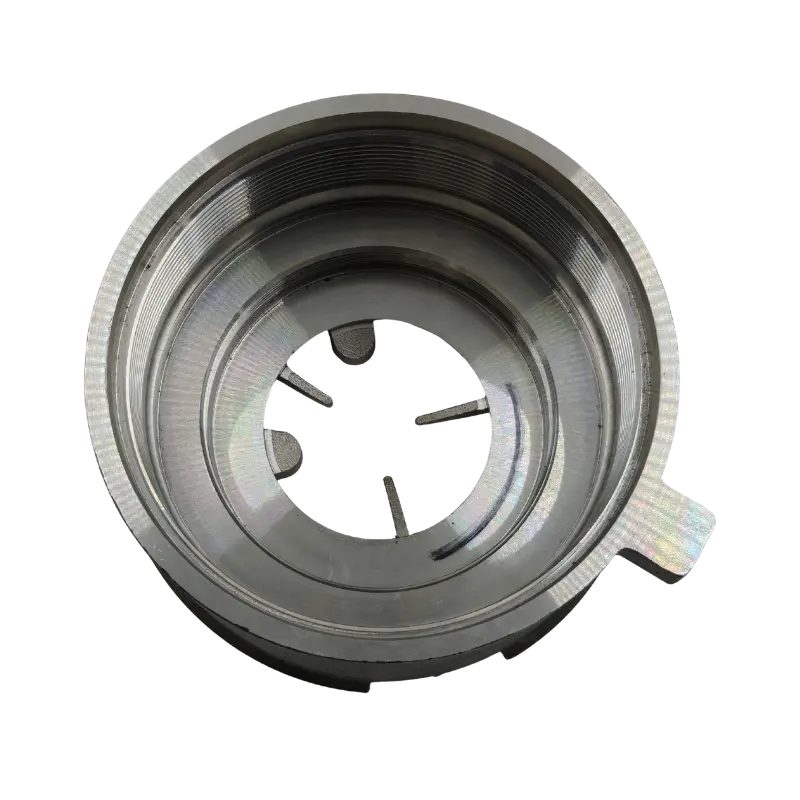
With in-house capabilities and qualified manufacturing partners, we provide CNC machining solutions to transform castings into precision-finished components, from prototypes to production parts.
CNC Turning
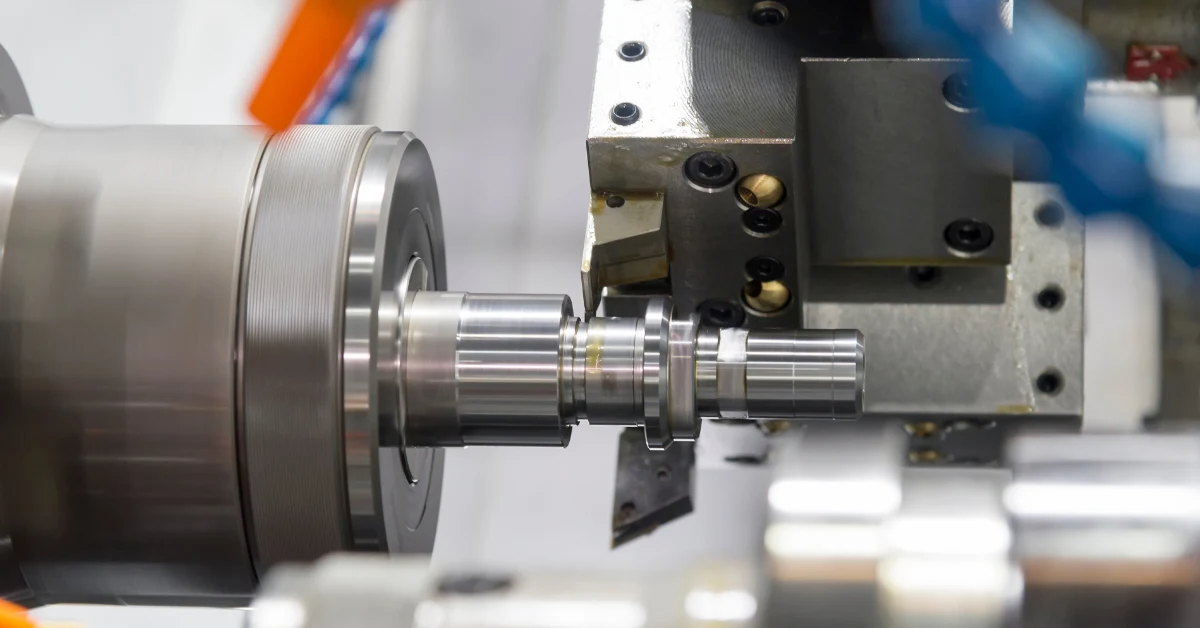
CNC turning is an effective way to finish casting parts with cylindrical features, enabling precise machining of diameters, bores, and threads for accurate assembly.
CNC Milling
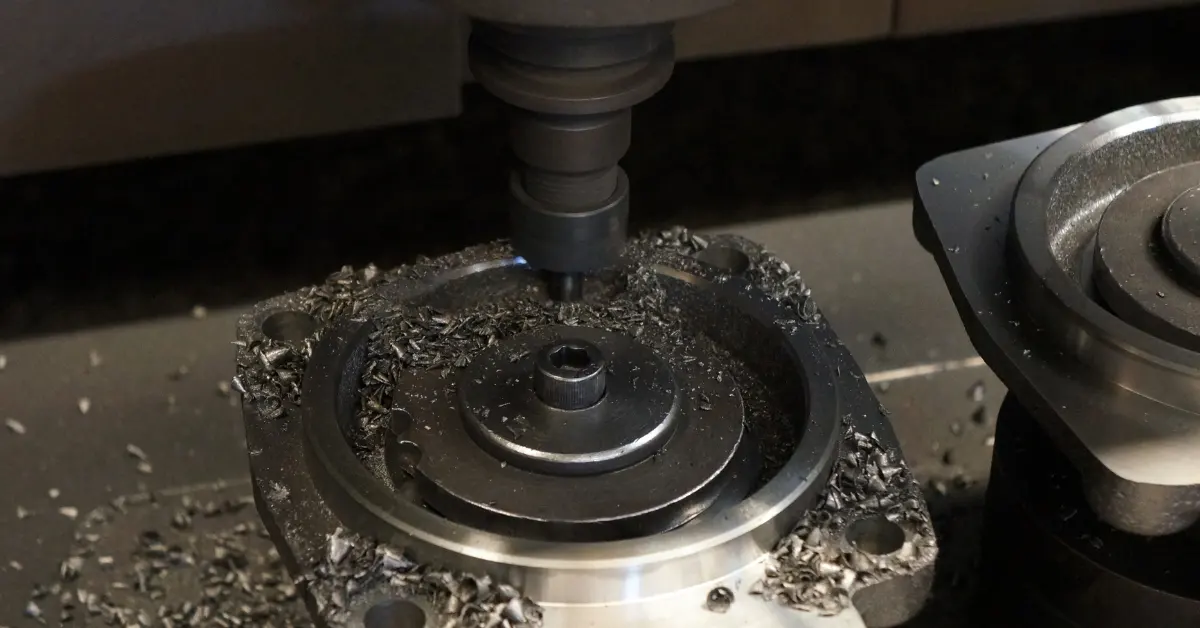
CNC milling is commonly used for castings requiring precision machining of complex geometries, including curved surfaces, angled holes, and critical mounting features.
Network Capabilities
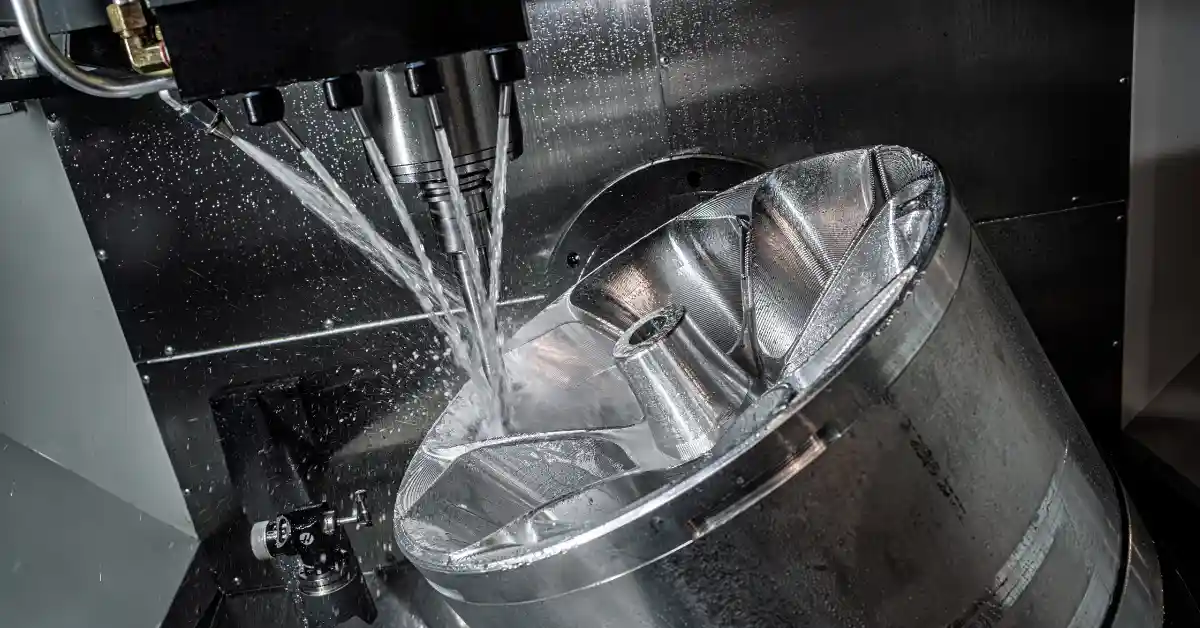
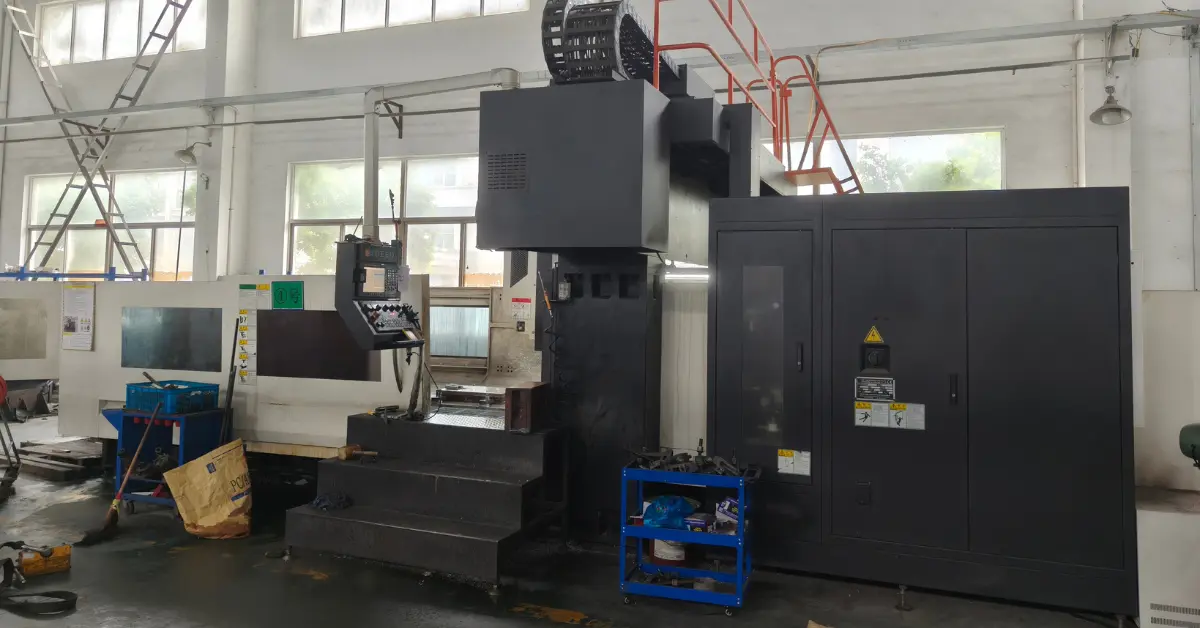
Our qualified manufacturing network provides advanced CNC processes, including 5-axis machining, to deliver high-precision finishing for complex castings with challenging geometries and tight tolerances.
CNC Machining for Complete Casting Solutions
Casting provides excellent near-net-shape components, but critical features often require additional machining to achieve final dimensional requirements.
With CNC machining capabilities and qualified manufacturing partners, we help transform castings into finished components with precise surfaces, accurate holes, and assembly-ready features.
Need Finished Metal Casting Parts?
Share your casting drawings or machining requirements. Our engineers will help determine the best manufacturing approach from casting and machining to surface finishing for your parts.
Request a QuoteCNC Machining Capabilities
Learn about the CNC machining capabilities offered by our in-house equipment and qualified partners.
Max Dimensions
| Metric (mm) | US (Inch) | |
|---|---|---|
| 5-Axis CNC Machining Centers | X1270 × Y508 × Z500 mm | X50.0″ × Y20.0″ × Z19.7″ |
| 4-Axis CNC Machining Centers | X790 × Y490 × Z500 mm | X31.1″ × Y19.3″ × Z19.7″ |
| 3-Axis Precision Milling & Tapping | X810 × Y500 × Z500 mm | X31.9″ × Y19.7″ × Z19.7″ |
| High-Precision CNC Turning Centers | Max Dia: Ø400 mm Length: 500 mm |
Max Dia: Ø15.75″ Length: 19.7″ |
| Standard CNC Lathes | Max Dia: Ø400 mm | Max Dia: Ø15.75″ |
Tolorances
| Metric (mm) | US (Inch) | |
|---|---|---|
| Precision Machining | Up to ±0.03 mm | Up to ±0.0012″ |
| Standard Machining | ±0.05 mm | ±0.0020″ |
| General Machining | ±0.10 mm | ±0.0039″ |
Network CNC Machining Capability
| Max Dimensions | Tolerance | |
|---|---|---|
| CNC Turning | Ø800 mm × 3000 mm | ±0.02 – ±0.10 mm |
| CNC Milling | 2000 × 1000 × 800 mm | ±0.02 – ±0.10 mm |
| 5-Axis Machining | 1000 × 800 × 700 mm | ±0.02 – ±0.05 mm |
Dimensions & Weight
| Iron-Based Alloys | Aluminum Alloys | Nickel-Based Alloys | |
|---|---|---|---|
| Max Part Envelope | 600 × 800 × 800 mm | 600 × 800 × 800 mm | 500 × 600 × 600 mm |
| Min. Wall Thickness | 1.5 mm | 1.0 mm | 1.5 mm |
| Weight Range | 0.01 – 120 kg | 0.01 – 50 kg | 0.01 – 70 kg |
Tolorances
| Iron-Based Alloys | Aluminum Alloys | Nickel-Based Alloys | |
|---|---|---|---|
| Max Part Envelope | 600 × 800 × 800 mm | 600 × 800 × 800 mm | 500 × 600 × 600 mm |
| Min. Wall Thickness | 1.5 mm | 1.0 mm | 1.5 mm |
| Weight Range | 0.01 – 120 kg | 0.01 – 50 kg | 0.01 – 70 kg |
Surface Roughness
| Surface Roughness (Ra) | |
|---|---|
| As Cast — Shot Blasted | Ra 6.3 – 12.5 μm |
| As Cast — Sand Blasted | Ra 3.2 – 6.3 μm |
| CNC Machined — 4-axis | Ra 1.6 – 3.2 μm |
| NC Machined — 5-axis | Ra 0.8 – 1.6 μm |
Logo & Text
For logos and texts that need to be attached to the parts, we primarily provide three methods:
- Directly cast on the surface: This method needs to engrave the logo or text on the wax injection mold, both intaglio and relief carving are supported. This is also the most cost-effective and flexible way we suggest.
- Engraving: Engraving is typically applied on the outer surface, which is limited by the engraving machine and the part geometries. This will need an extra fee for each part.
- Laser Etching: This process is similar to engraving, but has more limitations. Surface treatment, such as polishing, will affect the result.
What is CNC Machining?
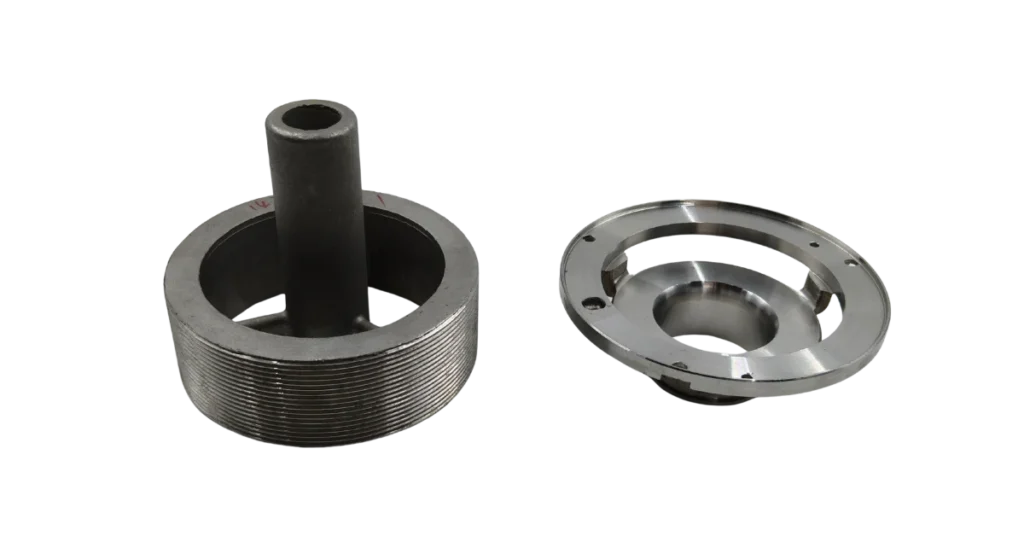
CNC machining is a highly precise subtractive manufacturing process where computers control the movement of factory tools. The workflow begins with engineers creating a 3D digital model using CAD software. This CAD model is then translated into G-code, a specialized programming language that provides the machine with exact coordinates and operational instructions. Following the G-code, the CNC machine automatically removes material from a raw block to produce the final physical part with extreme accuracy.
Depending on the required material and final shape, the industry relies on various specialized machines. The most important types include CNC milling, CNC turning, CNC routing, and CNC laser cutting.
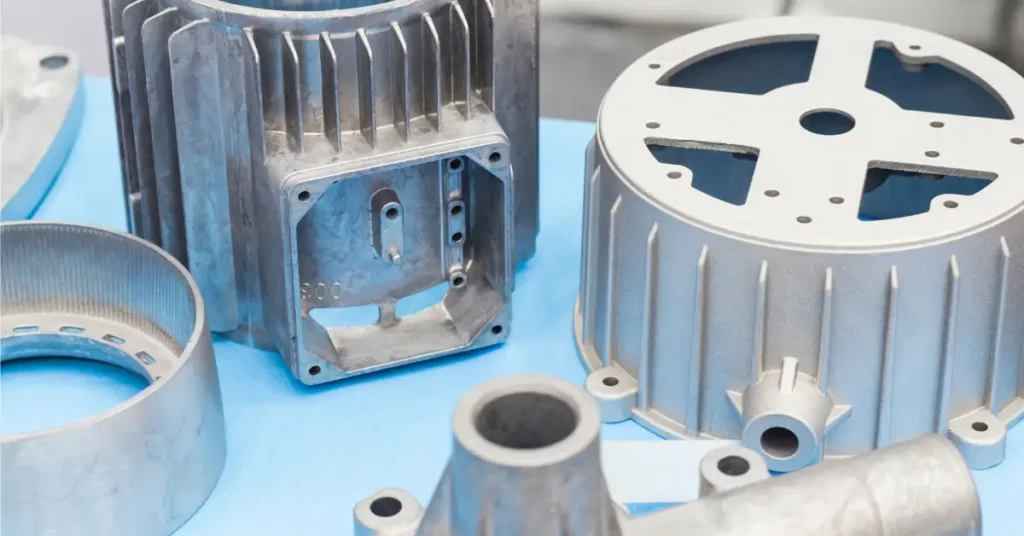
Advantages of Using CNC for Finishing Casting Parts
While modern casting is highly precise—with investment casting reaching tolerances around ±0.1mm. It is often insufficient for final functional requirements. Key assembly surfaces and intricate features like internal threads still demand the extreme accuracy of CNC machining. Using CNC to finish cast parts offers several critical advantages.
- CNC achieves micron-level precision, ensuring perfect fits for critical mating components.
- Significantly improves surface finish, smoothing out rough cast textures for better mechanical sealing and performance.
- Easily creates complex small holes and exact threads that are impossible to cast accurately.
- CNC guarantees absolute consistency across batches, eliminating the slight dimensional variations that naturally occur during the raw casting process.
FAQs
What types of castings can be CNC machined?
CNC machining can be applied to various cast components, including silica sol investment castings, sand castings, and die cast parts. Machining requirements depend on casting size, material, geometry, and required tolerances.
Which areas of a casting usually require CNC machining?
We use spectrometer analysis for alloy verification, coordinate measuring machines (CMM) for dimensional checks, and non-destructive testing such as X-ray and dye penetrant inspection for internal integrity. Material certifications and full inspection reports are provided with every order.
What machining tolerances can you achieve?
Our CNC machining capabilities support tolerances from ±0.10 mm for general machining to ±0.03 mm for precision features, depending on part geometry, material, and machining process.
What is the maximum casting size you can machine?
Our in-house CNC capabilities support machining up to Ø400 mm for turning and 1270 × 508 mm for milling. Through our qualified manufacturing network, larger cast components can also be supported.
Do you provide inspection reports for machined castings?
Dimensional inspection and quality documentation can be provided according to customer requirements, including inspection reports for critical dimensions.
Do you provide 5-axis CNC machining?
Yes. We provide access to 5-axis CNC machining for complex castings requiring multi-face machining, curved surfaces, and reduced setup operations.
Can you machine stainless steel and difficult materials?
We provide CNC machining for a wide range of casting materials, including stainless steel, aluminum, carbon steel, and nickel alloys.
Do you machine castings before or after heat treatment?
Machining sequence depends on material, dimensional requirements, and application. Critical features are typically machined after heat treatment when required to achieve final stability and accuracy.
Can you handle both prototype and production quantities?
Yes. Our CNC machining capability supports prototype development, low-volume production, and repeat production of cast components.