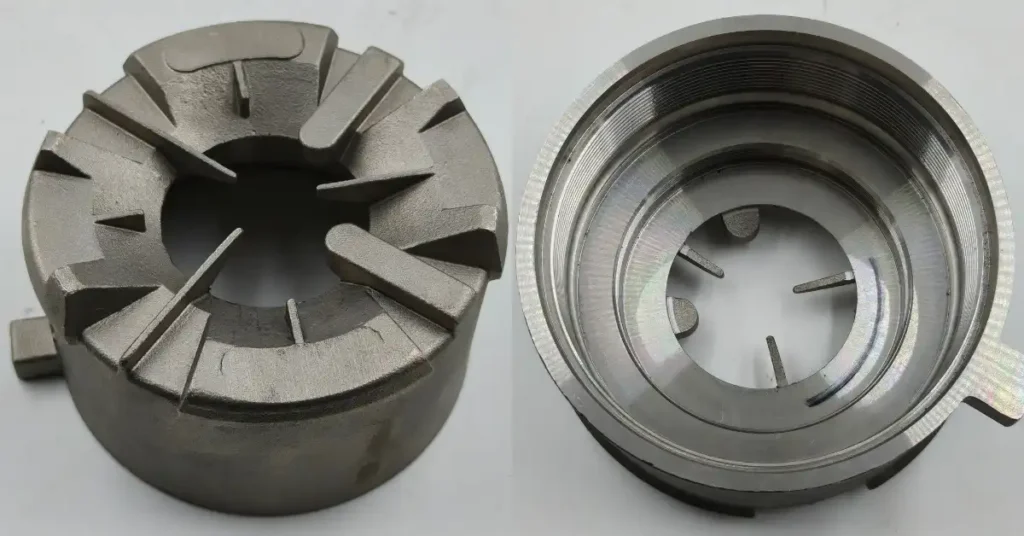
Investment casting surface finish is known to be the smoothest of any casting process. They usually land between Ra 1.6 and 6.3 micrometers, and even the best of sand casting can’t come close to that.
Even so, there are a lot of things that need to be better. This article looks at what affects the finish at the foundry, which extra steps can make it smoother, and how to choose the right option without paying for more than you need.
Why Improve Your As-Cast Investment Casting Finish?
Don’t look at surface finish as a cosmetic and physical detail on parts and components. In many cases, it helps the part work better and can reduce the amount of finishing needed later.
- Longer fatigue life:Deep surface marks can become starting points for cracks. Smoother finishes lower that risk greatly.
- Better corrosion resistance:Water and dirt have fewer places to sit on a smoother surface. This can help in marine and medical parts.
- More reliable sealing:Pumps and valves need flat, smooth contact areas. A rough face can leave small gaps where leaks begin.
- Easier coating:Paint, plating, and other finishes usually apply more evenly on a controlled surface.
- Better cleanability:Smooth parts are simply easier to wash. That matters in food and medical equipment, where dirt or bacteria can collect in rough spots.
- Less machining:If the casting already comes out smooth enough, fewer surfaces need extra work afterward.
Improving Investment Casting Finish at the Foundry
Good finishes start before the metal is poured. The casting copies the wax pattern, so problems in the die or wax can show up on the final part.
Wax Pattern Quality
Smooth dies produce a smoother wax pattern. This gives the ceramic shell a better surface to copy. Stable wax injection also helps prevent flow lines before they become a finishing problem later.
The Ceramic Face Coat
The first ceramic layer touches the metal, so they have major effect on the final surface. Fine powder in the 200 to 325 mesh range creates a smoother face coat. Zircon is often used because it holds finer detail and handles contact with hot metal better.
Binder Choice
The binder holds the ceramic together. Colloidal silica usually creates a tighter shell and smoother finish. Sodium silicate costs less, but the surface is often rougher.
Pour Temperature
The metal needs enough heat to fill the mold properly. Too hot, and it may react with the ceramic shell. Too cold, and small details may not fill completely.
Alloy Selection
The alloy can change how cleanly the casting separates from the shell. Stainless and cobalt-chrome alloys can reach about Ra 1.2 to 3.2 µm. Carbon steel is often rougher, closer to Ra 3.2 to 6.3 µm.
Drying and Handling
Even a small shell crack can leave a raised mark on the casting. Giving each layer enough time to dry and handling the shell carefully helps prevent these defects before pouring.
Comparing Foundry-Side Improvements
Here is how those six levers stack up against each other.
| What to control | Effect on finish | How much it costs | Who decides it |
| Wax pattern quality | Very high | Built into tooling | Foundry, at tooling stage |
| Ceramic face coat | Very high | Moderate | Foundry |
| Binder choice | High | Higher for silica sol | Foundry, worth asking about |
| Pour temperature | High | None, process control | Foundry |
| Alloy selection | Moderate | Varies widely | You, on the drawing |
| Drying and handling | Moderate | None, process discipline | Foundry |
Mechanical Finishing for Investment Castings
After the shell comes off, some castings are ready with only basic cleaning. Others need more work. The right method depends on the surface you need and where that surface is on the part.
Blasting
Blasting usually comes first because small pieces of ceramic may still be stuck to the metal. What happens next depends on the blasting material:
- Glass bead:Gives a soft satin finish, usually around Ra 0.5 to 0.8 µm.
- Aluminum oxide:Cuts into the surface more and leaves about Ra 1.8 to 3.5 µm. This can work well before coating.
- Steel shot:Cleans more heavily, with a finish around Ra 3.6 to 5.0 µm. It can also help the surface handle repeated stress.
Tumbling
You can finish batches of small castings together instead of doing them one at a time. They go into a machine with ceramic media, moving around the parts and wears away small burrs. Finishes below Ra 5 µm are possible.
Deep holes are harder to reach, though. Furthermore, there’s a chance for sharp edges to become slightly rounded during the process.
Grinding
You wouldn’t normally grind the whole casting. It makes more sense for small areas that need extra attention. Gate marks are a good example. Grinding can remove the raised metal and smooth it into the nearby surface.
On an easy-to-reach area, the finish may reach Ra 0.1 to 0.4 µm.
Polishing
This is usually the step chosen when the final appearance matters. The surface is worked with finer abrasives until it becomes smooth. Buffing can take it even further and produce a mirror-like finish below Ra 0.1 µm.
CNC Machining
CNC machining is used when certain areas need tighter dimensions or a more controlled surface than casting alone can provide. Common examples include mounting faces, bearing seats, holes, threads, and sealing surfaces.
A machined surface can typically reach around Ra 0.8 to 3.2 µm, depending on the operation and cutting conditions. Only the areas that need it are usually machined, since removing material from the whole casting would add cost without much benefit.
There is one simple limit: the tool has to reach the surface. Outside faces are much easier to polish than deep holes or hidden areas.
Chemical Finishing for Investment Castings
Chemical methods are useful when tools or blasting media cannot easily reach the surface. Let’s take a look at some of the typical investment casting chemical finishing option available.
- Pickling: Removes scale and heat marks from the metal. It can make the surface a little smoother and is often used before another finishing step.
- Electropolishing: Useful for holes and complex shapes because it does not need direct tool access. It removes very small high points from the surface and may improve roughness by about 10% to 50%. Deep scratches will usually remain.
- Passivation: This one is different because its main purpose is not smoothing. On stainless steel, it helps restore the protective surface layer and improve corrosion resistance.
- Isotropic superfinishing: Used when an extremely smooth surface is needed, such as on gears or bearings. It can bring the finish below Ra 0.1 µm by gradually removing the high points on the surface.
What Makes a Bad Surface?
A poor finish is usually telling you something specific about what went wrong. Learning to recognize a few common patterns saves a lot of back and forth with your supplier.
| What you see | What caused it | How it gets fixed |
| Rough, sandy patches | The face coat used powder that was too coarse, or grit from the outer shell layers worked its way through to the surface | Foundry, by changing the shell recipe |
| Small round pits | Gas trapped against the surface, usually from a damp shell or metal that filled too turbulently | Foundry, by drying shells properly and calming the fill |
| Dimpled, orange-peel look | The metal or the mold was too hot going in | Foundry, by lowering temperature |
| Ripples or fine lines | The wax pattern itself, not the metal. Injection settings were off when the pattern was made | Foundry, at the wax stage |
| Hard specks in the surface | Bits of shell or slag carried in with the pour | Foundry, by filtering and handling shells more carefully |
| Rough, burnt-on texture | Metal poured too hot soaked into the ceramic and fused to it | Blasting can remove it, but the real fix is a lower pour temperature |
Most surface problems start at the foundry, not during finishing. If the same defect keeps showing up, polishing or tumbling will only hide part of it. Usually, the best and most effective fix is to look at the process first.
Improve Your Investment Casting Finish With YTD Foundry
Most finish problems are cheaper to solve at the wax and the shell than after the parts arrive. Investment casting is our entire focus at YTD Foundry, so investment casting surface finish is something we build in rather than fix afterward.
Send us a copy of your sketch with the surface finish requirements marked, and we’ll tell you what we can hold as-cast, what needs a secondary operation, and what each option adds to the part.