
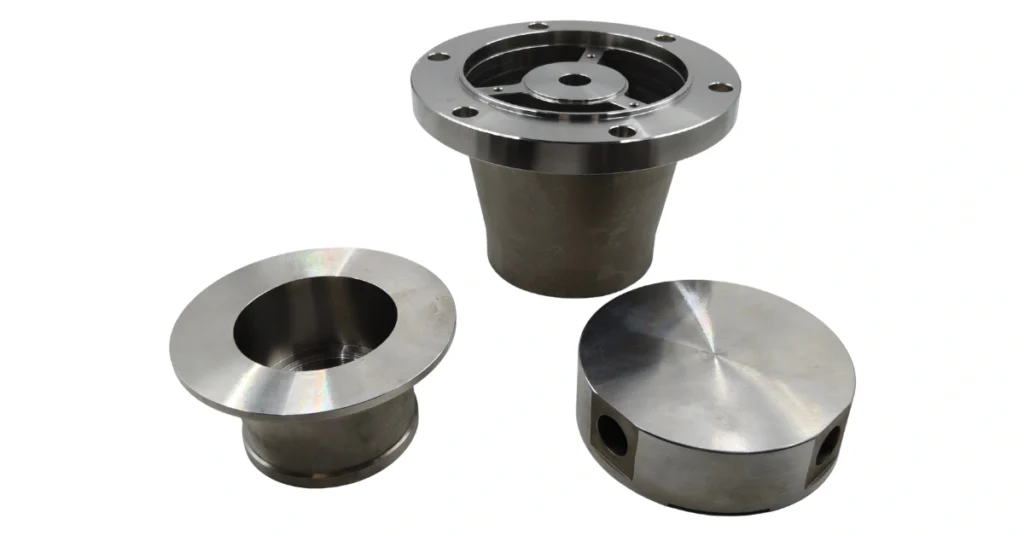
Why Stainless Steel Is Widely Used in Investment Casting
Compatibility of Stainless Steel with Investment Casting
Investment casting, also called lost wax casting, allows us to produce intricate geometries, thin walls, and complex internal passages with superior surface finishes for your projects.
When we pair this process with stainless steel—which is heavily relied upon for its exceptional corrosion resistance, high strength, and thermal durability—the result is a high-precision component capable of surviving your harshest operational environments.
Advantages of Stainless Steel Investment Casting
Solid raw stainless steel is difficult to cut and prone to work-hardening. If you opt for costly CNC machining, it not only causes severe tool wear but also results in significant material waste.
Investment casting can solve this problem perfectly. By delivering your parts in a near-net shape, it minimizes secondary machining allowances, reduces cycle times, eliminates the need for multi-part welded assemblies, and significantly lowers your overall production costs.
Types of Stainless Steel Used in Investment Casting
Austenitic Stainless Steel
Austenitic grades are the most popular alloys we use in stainless steel investment casting, offering you the best balance of exceptional corrosion resistance and overall processability.
While this type of stainless steel has medium casting fluidity and a low tendency to crack from heat, it features a relatively high shrinkage rate (about 2.3%–3%). This can cause cavities to form in the center of your casting as it solidifies. To prevent this, we design a well-planned gating and riser system to make sure the shrinkage is properly compensated.
Common Grade: 304(CF-8), 316(CF-8M), 304L(CF-3), 316L(CF-3M)
Martensitic Stainless Steel
Martensitic stainless steels are commonly applied in cast components requiring excellent wear resistance and moderate corrosion resistance, and they can achieve higher strength and hardness through heat treatment.
In investment casting, martensitic stainless steel exhibits good fluidity and low shrinkage (approximately 1.5%–2.0%); however, it is extremely sensitive to thermal cracking.
To prevent your castings from snapping or cracking, we strictly control the shell’s shakeout timing by implementing slow and insulated cooling processes.
Common Grade: 410(CA-15), 420(CA-40), 440C
Duplex Stainless Steel
Duplex stainless steels offer you high strength and outstanding chloride stress corrosion resistance, but bring processing challenges beyond those of austenitic or martensitic grades.
Their two-phase structure is thermally sensitive—pouring temperature or cooling rate deviations easily trigger σ phase precipitation, which severely compromises both corrosion resistance and ductility.
To ensure your castings are reliable, we perform mandatory solution annealing after casting to restore the proper austenite-ferrite balance, while our gating design carefully accounts for the different shrinkage behaviors of the two phases during solidification.
Common Grade: 2205(CD3MN), 2507
Precipitation-Hardening Stainless Steel
Precipitation-hardening stainless steels are valued in investment casting for their narrow freezing range (which aids filling), minimal distortion during heat treatment, and low temperature aging that eliminates quenching cracks and scaling.
They flow well in the mold, yet solidification driven segregation—especially of copper—can lead to uneven hardness after final aging.
Therefore, we tightly control melt chemistry and implement precise high-temperature homogenization heat treatment to eliminate copper segregation and ensure consistent mechanical properties for your applications.
Common Grade: 17-4 PH(CB7Cu-1), 15-5 PH
Ferritic Stainless Steel
Ferritic stainless steel offers low cost and low thermal expansion, but poor toughness and irreversible grain coarsening in thick sections make it rarely used in investment casting—except for cost-sensitive, heat-resistant non-thin-walled parts.
Common Grade: 430
304 vs 316 Stainless Steel Investment Castings
Both 304 (CF8) and 316 (CF8M) are austenitic grades sharing similar casting traits—medium fluidity, low hot cracking tendency, and high shrinkage. The sole difference is 316’s 2–3% molybdenum addition, which shifts several process parameters in practice.
| Comparison Aspect | 304(CF8) | 316(CF8M) | Impact on Casting Process |
| Fluidity | Better | Slightly lower (molybdenum increases viscosity) | 316 requires adjusted pouring parameters |
| Pouring Temperature | Baseline | Similar to 304, but needs strict control/higher shell preheating to compensate for higher viscosity | Different process parameters for each grade |
| Shrinkage Rate | Baseline | About 0.12–0.17% higher (difference grows with section thickness) | 316 demands a more robust riser and gating design |
| Hot Tearing Tendency | Low | Slightly higher (wider freezing range) | 316 complex parts need stricter cooling control |
| Cost | Baseline | 15–25% higher | Choose 304 for non-chloride environments, 316 for seawater/chemical applications |
Challenges in Stainless Steel Investment Casting
While stainless steel investment casting delivers unmatched design freedom, achieving a flawless component requires overcoming severe metallurgical and physical constraints during the stainless steel investment casting process.
High Pouring Temperatures
Stainless steels require pouring temperatures of 1,500–1,600°C, placing extreme thermal stress on your shell molds and demanding precise process control.
A ±15°C deviation can cause hot tears or gas porosity, so we monitor temperatures tightly and use robust materials to protect your casting quality.
Shrinkage and Feeding
Austenitic stainless grades shrink 2.3–3% during solidification—significantly more than carbon steel—making your parts prone to centerline cavities and microporosity without proper feeding.
That’s why we design strategic risers and directional solidification; these are musts in our process to secure your component integrity.
Thin-Wall Filling Limits
Stainless steel melts have inherently lower fluidity than aluminum or copper alloys, limiting their ability to fill long, thin cross-sections before freezing off.
For 300 series grades, we recommend a minimum wall thickness of 1.0–1.5 mm; for complex shapes, an early design evaluation is essential to avoid failed trials.
Machining Still Needed
Investment casting delivers near-net shapes, but “near” still leaves room for post-cast machining.
Austenitic grades work harden fast, so we use specialized tooling and slower speeds to prevent wear on your tools. Our in house machining is a capability we manage carefully for you.
Grade-Specific Behaviors
Each stainless family has quirks—martensitic cracks easily, duplex embrittles if cooling varies, and PH suffers copper segregation.
We’ve tackled these through experience, so we can advise you on grade selection and process control. Rely on our know how for your project.
Common Defects in Stainless Steel Investment Castings
Surface Pockmarks
Small craters unique to stainless steel casting—chromium reacts with facecoat impurities at high heat, etching the surface.
We use high-purity zircon facecoat and strict shell controls to keep your surfaces smooth.
Black Spots
Dark spots from non-metallic inclusions. Stainless steel’s chromium-rich melt oxidizes easily, making cleanliness tougher than carbon steel.
We maintain rigorous melt purification and slag removal for clean castings.
Dimensional Deviation
Parts that miss your tolerances from uneven solidification or wrong shrinkage allowance. Different grades shrink differently—304 less than 316—so we adjust tooling factors per grade and simulate solidification to get your dimensions right.
Typical Applications of Stainless Steel Investment Castings
Aerospace & Defense
- Engine brackets, fuel system components, actuator housings, structural fittings…
- 17-4PH is selected for high strength and corrosion resistance in critical, tight-tolerance parts.
Valves, Pumps, and Flow Control
- Valve bodies, impellers, pump housings, pipe fittings….
- 316/316L is preferred for pitting resistance, while investment casting delivers smooth internal passages for pressure integrity.
Medical & Dental Instruments
- Surgical tool handles, implant prototypes, dental instrument heads…
- 304L and 316L offer biocompatibility and smooth surfaces that polish easily for sterilization.
Food & Beverage Processing
- Pump rotors, valve seats, fittings, spray nozzles…
- Crevice-free surfaces are cast for hygiene, and 316L is recommended for acidic or corrosive cleaning environments.
Marine & Offshore Equipment
- Seawater pump casings, valve trim, propellers, deck hardware…
- Duplex grades provide chloride stress corrosion resistance for constant saltwater exposure.
Industrial Machinery & General Engineering
- Gear housings, lever arms, brackets, custom fittings…
- Multiple parts can be consolidated into single castings, with 304 offering strength and cost balance.
How to Choose the Right Stainless Steel Grade for Your Casting Project
Service environment first. Chloride exposure? 316L or duplex. No chlorides? 304 handles most jobs. Need wear resistance? Martensitic. Extreme strength? 17-4PH.
Then castability. Thin walls and complex geometry favor austenitic or PH grades. Martensitic casts easily but needs slow cooling. Duplex is strong but process-sensitive. Ferritic only for simple, thick sections.
Budget last. 304 is your baseline. 316 adds 15-25%. Duplex and PH carry premiums—justify them against performance needs.
Still unsure? Send us your drawing. We’ll pick the grade for you.
Conclusion
Stainless steel investment casting offers unmatched design freedom and corrosion resistance, but success requires the right grade, process control, and defect prevention. As your experienced stainless steel investment casting manufacturer, we deliver quality castings with reliable service. Contact us to start your project.
FAQs
Is 304 or 316 better for investment casting?
Neither is “better”—304 costs less; 316 adds pitting resistance for chlorides. Choose based on your environment.
Can stainless steel investment castings be heat treated?
Austenitic grades cannot be hardened by heat treatment. Martensitic and PH grades can—and need it for strength.
What are the main advantages of stainless steel castings over carbon steel castings?
Corrosion resistance and higher strength, plus near-net shapes that reduce machining and material waste.
What defects are common in stainless steel investment castings?
Surface pockmarks (chromium reaction), black spots (inclusions), and dimensional deviation from shrinkage differences.
Is stainless steel investment casting suitable for marine applications?
Yes—use duplex grades or 316L for chloride stress corrosion resistance in constant saltwater exposure.
Can investment casting reduce machining on stainless steel parts?
Yes—near-net shapes minimize machining, but austenitic grades still work-harden fast during any required post-processing.
What is the difference between austenitic and martensitic stainless steel castings?
Austenitic offers corrosion resistance and high shrinkage; martensitic offers wear resistance and hardness but cracks more easily.
Can you weld stainless steel investment castings after casting?
Yes—but L-grades (304L/316L) resist intergranular corrosion better when welded. Consider post-weld heat treatment.
What certifications should a stainless steel investment casting manufacturer have?
ISO 9001 is standard; industries like aerospace or medical require AS9100 or ISO 13485.
Which grade offers the highest strength among stainless steel castings?
17-4PH (precipitation-hardening) delivers the highest strength, up to 1300 MPa after aging treatment.


