Investment casting and die casting can both produce precise, complex metal parts, but they are usually chosen for different reasons.
Investment casting is flexible in material choice and complex geometry, with a lower commitment to permanent tooling. Die casting becomes especially powerful when a stable non-ferrous part must be produced repeatedly at high volume.
In many projects, the decision can be narrowed quickly by asking two questions first:
What metal does the part require, and how many parts will the program need over its lifetime?
The rest of the comparison follows from there.
Investment Casting vs Die Casting: Quick Comparison
| Factor | Investment Casting | Die Casting |
|---|---|---|
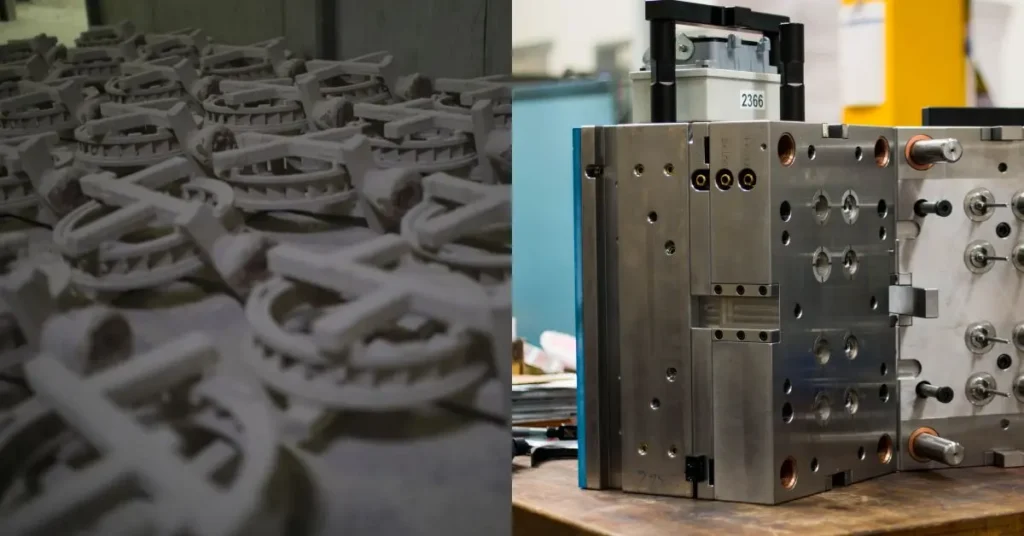
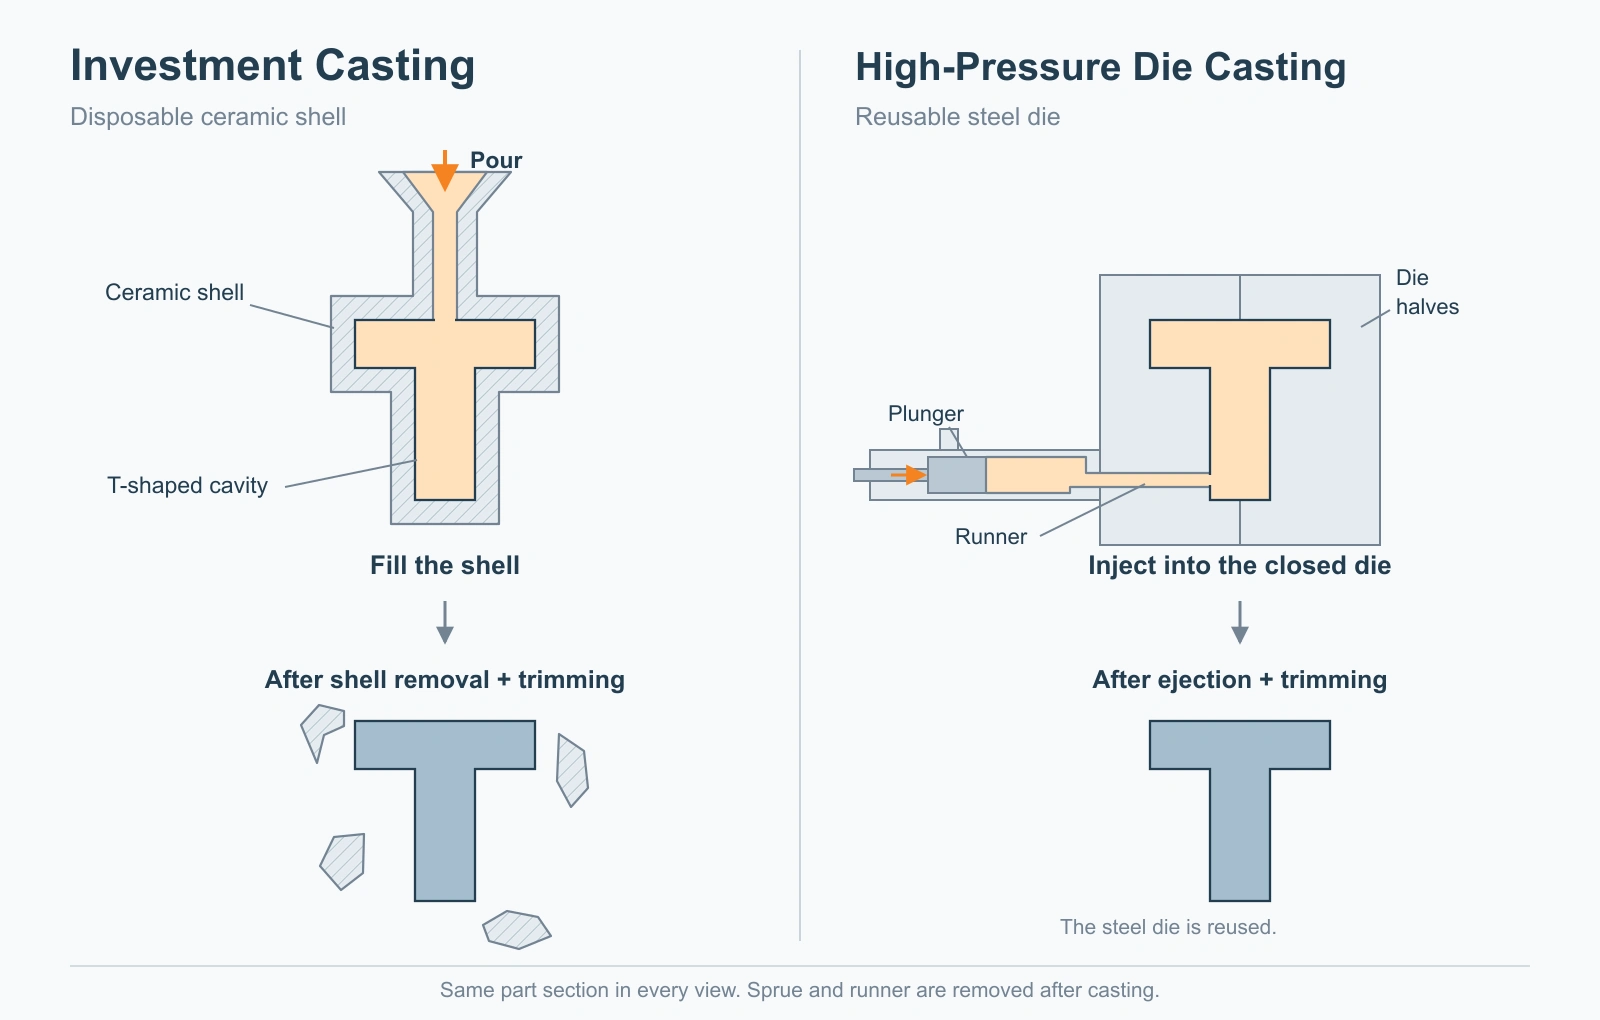
| Mold | Disposable ceramic shell | Reusable steel die |
| Metal Filling | Usually gravity poured | Injected under high pressure |
| Common Materials | Steel, stainless steel, alloy steel, aluminum, superalloys and more | Mainly aluminum, zinc, magnesium; selected copper alloys |
| Tooling Investment | Lower | Higher |
| Production Speed | Slower | Very fast after tooling is complete |
| Best Volume Range | Low to medium, plus repeat specialized production | Medium to very high volume |
| Complex Geometry | Excellent | Excellent, but constrained by die opening and ejection |
| Thin Walls | Good | Strong advantage for suitable non-ferrous alloys |
| Surface Finish | Good to very good | Very good and highly repeatable |
| Dimensional Repeatability | Good | Excellent in stable production |
| Heat Treatment | Broadly available depending on alloy | Process-dependent |
| Design Changes | Easier before production tooling is finalized | Can become expensive after the die is built |
The important point is that these processes do not always compete directly.
A stainless steel turbine component and a zinc hardware component may both be “precision castings,” but they naturally belong to very different manufacturing routes.
What “Die Casting” Means in This Comparison
Die casting is a broader family than the name sometimes suggests.
For this article, die casting primarily refers to high-pressure die casting, where molten metal is forced into a reusable steel die.
There are several important versions of the process.
Hot Chamber Die Casting
In hot chamber die casting, the injection system remains connected to or immersed in the molten metal supply.
This shortens the cycle and is commonly associated with zinc and selected magnesium alloys.
Cold Chamber Die Casting
In cold chamber die casting, molten metal is prepared separately and transferred into the shot sleeve for each cycle.
This is the standard route for aluminum die casting and is also used for selected magnesium and copper alloys. NADCA identifies aluminum, copper, some magnesium alloys, and high-aluminum zinc alloys as typical cold-chamber materials.
High-Integrity Die Casting
High-vacuum, squeeze, and semi-solid die casting are specialized routes used where reducing gas porosity and improving mechanical integrity matter.
This distinction becomes important later when discussing heat treatment, welding, and structural applications.
For a general overview of the die casting family, see YTD’s die casting guide.
Material Choice Is Usually the First Filter
Before comparing tolerance or tooling cost, check whether both processes can realistically produce the required alloy.
Investment Casting Has the Broader Alloy Range
Investment casting can process a wide range of metals because the molten alloy is poured into a disposable refractory ceramic shell.
Typical material families include:
- Carbon steel
- Alloy steel
- Stainless steel
- Aluminum alloys
- Copper alloys
- Nickel-based superalloys
- Cobalt-based alloys
The ceramic mold is used once and destroyed after casting. The Investment Casting Institute describes this disposable shell system as a defining part of the process.
Die Casting Has a Narrower Practical Material Range
High-pressure die casting relies on a reusable steel die and injection system.
The most common die casting alloys are based on:
- Aluminum
- Zinc
- Magnesium
- Selected copper alloys
NADCA identifies these as the principal commercial die-casting alloy families.
The consequence is simple:
If the part must be stainless steel, carbon steel, alloy steel, or a nickel-based superalloy, conventional die casting is generally no longer the relevant comparison.
Investment casting, sand casting, forging, or machining becomes the more realistic process family.
The real overlap between investment casting and die casting is therefore strongest in metals such as aluminum.
Tooling Investment and Lifetime Production Volume
The second major filter is not simply “annual quantity.”
It is how many stable parts the program is expected to produce over the life of the tooling.
Investment Casting Tooling
Investment casting normally uses tooling to produce repeatable wax patterns.
That tool does not contain molten metal and does not experience the same thermal and mechanical stresses as a die casting die.
The result is generally a lower initial tooling commitment.
However, every production casting still requires:
- A new wax pattern
- Shell building
- Drying
- Dewaxing
- Firing
- Pouring
- Shell removal
The variable manufacturing effort remains significant for every batch.
Die Casting Tooling
A die casting tool is a production machine component in its own right.
It may incorporate:
- Cavity and core blocks
- Runners and gates
- Vents and overflows
- Cooling circuits
- Ejector systems
- Slides
- Moving cores
The tooling must survive repeated thermal cycles and high-pressure filling.
That creates a much higher initial cost.
But after the die is approved, the same tool can cycle repeatedly at high production rates.
This produces the basic economic difference:
Investment casting reduces the cost of entering production. Die casting reduces the cost of repeating production at scale.
There is no reliable universal break-even quantity.
The correct threshold depends on die complexity, cavity count, alloy, part size, cycle time, scrap rate, machining, finishing, and expected tool life.
Geometry: Complex Does Not Mean the Same Thing in Both Processes
Both processes can make very complex parts.
The difference is what kind of complexity each process tolerates naturally.
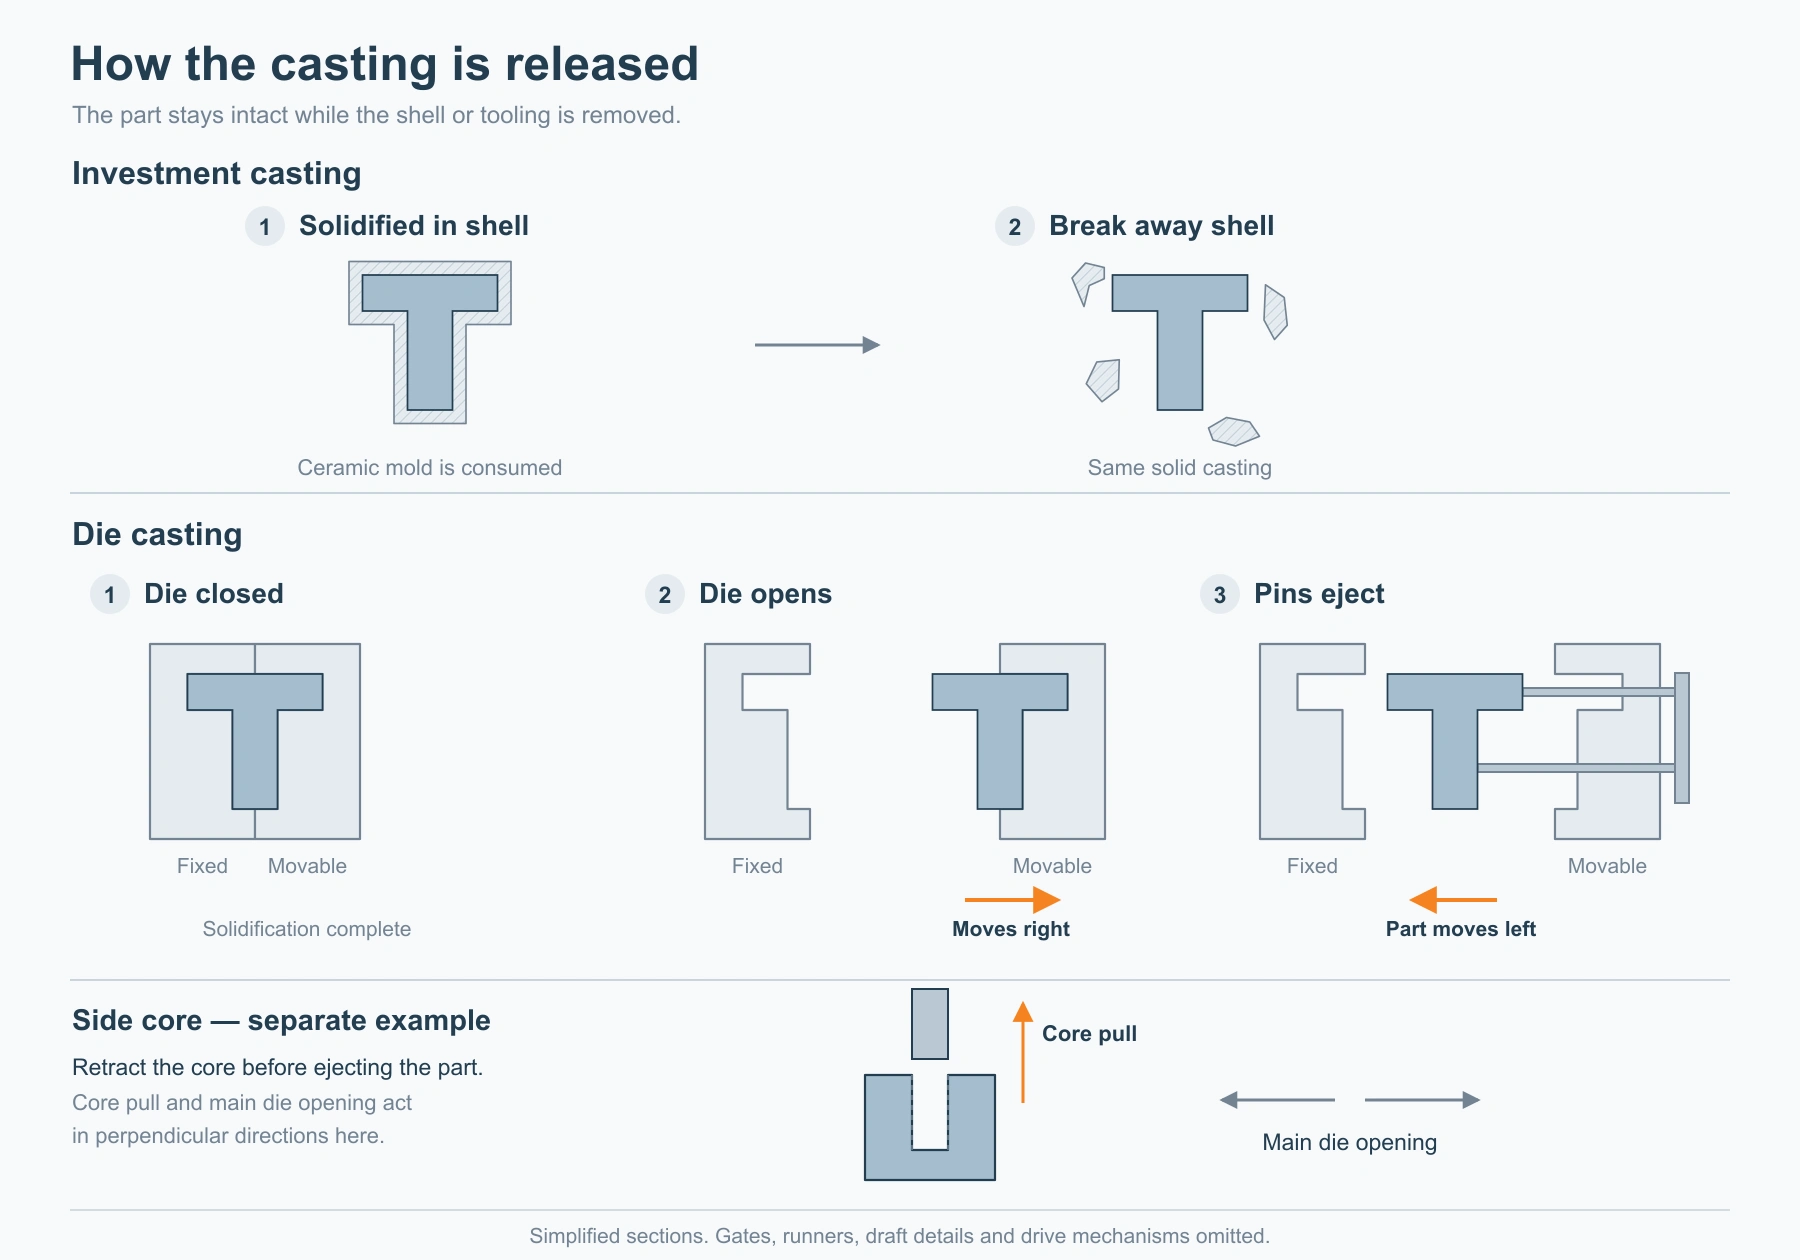
Investment Casting Is Free From Permanent-Die Ejection
The ceramic shell is destroyed after casting.
That means the finished metal component does not have to be mechanically pulled out of the mold in the same way as a die casting.
This creates useful freedom for:
- Irregular 3D geometry
- Difficult external contours
- Complex transitions
- Fine features
- Certain internal cavities
- Shapes that would require complicated die actions
Ceramic cores can also be used for selected internal passages.
Die Casting Must Open and Release the Part
A reusable die must open after every cycle.
The designer therefore has to consider:
- Draft
- Parting lines
- Ejector pin locations
- Slide direction
- Undercuts
- Core movement
Die casting can still create highly complex parts, but complexity may move from the casting into the tooling.
A geometry that looks simple on the finished component can require a very sophisticated steel die if several features cannot release in the main opening direction.
For investment-casting-specific geometry, see YTD’s investment casting design guidelines.
Thin Walls, Accuracy, and Surface Finish
This is one area where simple statements such as “investment casting is more precise” are not very useful.
Both are precision casting processes.
Thin Walls
High-pressure filling gives die casting a strong advantage when producing thin non-ferrous walls, ribs, fins, and lightweight housings.
Molten metal enters the die quickly before it can freeze.
This is one reason die casting is so widely used for:
- Electronic housings
- Automotive structures
- Gearbox housings
- Heat-management components
- Thin-wall zinc hardware
Investment casting can also produce relatively thin and intricate sections, but its filling mechanism is fundamentally different.
If the project is a very thin aluminum housing produced in large quantities, die casting deserves serious consideration.
Dimensional Accuracy
Investment casting provides good near-net-shape dimensional control, but several stages contribute variation:
- Wax tooling
- Wax shrinkage
- Shell building
- Alloy shrinkage
- Geometry
Die casting uses the same rigid steel cavity for every production cycle, giving it very strong repeatability once the tooling and process are stable.
This is particularly valuable in large-volume programs where dimensional consistency across tens of thousands of parts matters.
Surface Finish
Both processes can produce a good as-cast surface.
Investment casting inherits the smooth surface of the wax pattern through the ceramic shell.
Die casting solidifies against a machined steel die and can therefore deliver a smooth, highly repeatable surface.
The practical choice should be based on the surface the application actually needs rather than assuming one process automatically eliminates finishing.
Porosity Changes the Die Casting Discussion
One of the most important technical differences between these processes appears inside the casting rather than on its surface.
Conventional high-pressure die casting fills the mold very rapidly.
If air is trapped during filling, gas porosity can remain inside the component.
This matters because internal gas can affect:
- Heat treatment
- Welding
- Pressure tightness
- Structural performance
But it would be wrong to conclude:
Die castings are always porous.
Modern die casting includes several high-integrity processes designed specifically to reduce gas entrapment.
NADCA identifies high-vacuum, squeeze, and semi-solid casting as structural/high-integrity processes. High-vacuum systems evacuate the die cavity before and during filling, while squeeze and semi-solid approaches reduce turbulent gas pickup through different filling conditions.
Research on vacuum-assisted aluminum die casting has also found substantially reduced gas porosity and less blistering after heat treatment compared with conventional die casting.
So internal integrity should be treated as a process specification, not simply as a label attached to all die casting.
Heat Treatment: Avoid the Common Oversimplification
You will often see statements online such as:
“Investment castings can be heat treated; die castings cannot.”
That is too broad.
Investment Casting
Investment castings commonly receive whatever thermal treatment the alloy specification requires, including processes such as:
- Annealing
- Solution treatment
- Aging
- Normalizing
- Quenching and tempering
The exact treatment depends on material and required properties.
Conventional HPDC
Conventional high-pressure aluminum die castings may contain trapped gas.
When exposed to high solution-treatment temperatures, that gas can expand and produce surface blistering.
This limits the heat-treatment options for many conventional HPDC components.
High-Integrity Die Casting
High-vacuum, squeeze, and semi-solid processes reduce gas entrapment.
NADCA specifically notes that these routes can produce heat-treatable castings.
So if an aluminum project requires T6/T7-type structural properties, the correct comparison may not be:
Investment casting vs ordinary die casting
but:
Investment casting vs high-integrity structural die casting
That distinction can completely change the manufacturing decision.
CNC Machining and Secondary Operations
Neither process eliminates machining.
What changes is where machining adds value.
Investment casting is often selected because it can create complicated near-net geometry that would otherwise require substantial material removal.
Typical post-cast machining may be limited to:
- Precision bores
- Bearing seats
- Threads
- Sealing faces
- Mounting surfaces
At YTD, these features can be completed through in-house CNC machining after investment casting.
Die casting can also deliver excellent near-net geometry, especially after the production die has been optimized.
Large-volume die-cast components may still require machining for functional interfaces, but repeatable datum structures and automated fixtures can make this secondary machining very efficient.
The useful question is therefore not:
Which process needs no machining?
It is:
Which process leaves the least expensive machining for the features the drawing actually requires?
Production Speed vs. Time to Launch
Die casting clearly wins on casting cycle time once production is mature.
A reusable die can be filled, cooled, opened, and cycled repeatedly.
Investment casting must rebuild an expendable wax pattern and ceramic shell for every casting.
But production cycle time is not the whole schedule.
Investment Casting Can Require Less Tooling Commitment
A wax-pattern tool is generally simpler than a sophisticated multi-slide production die.
That can make investment casting attractive when:
- Production quantity is uncertain
- The product is early in its life cycle
- Geometry may still change
- A very expensive steel die would create financial risk
Die Casting Rewards Design Stability
After a production die has been designed, machined, assembled, sampled, corrected, and approved, engineering changes can become expensive.
A small geometry change may affect:
- Cavity inserts
- Slides
- Cooling
- Ejection
- Gating
- Venting
That is why lifetime production confidence matters.
The best die casting project is not simply a high-volume project.
It is a high-volume, stable project.
Investment Casting vs Die Casting Cost
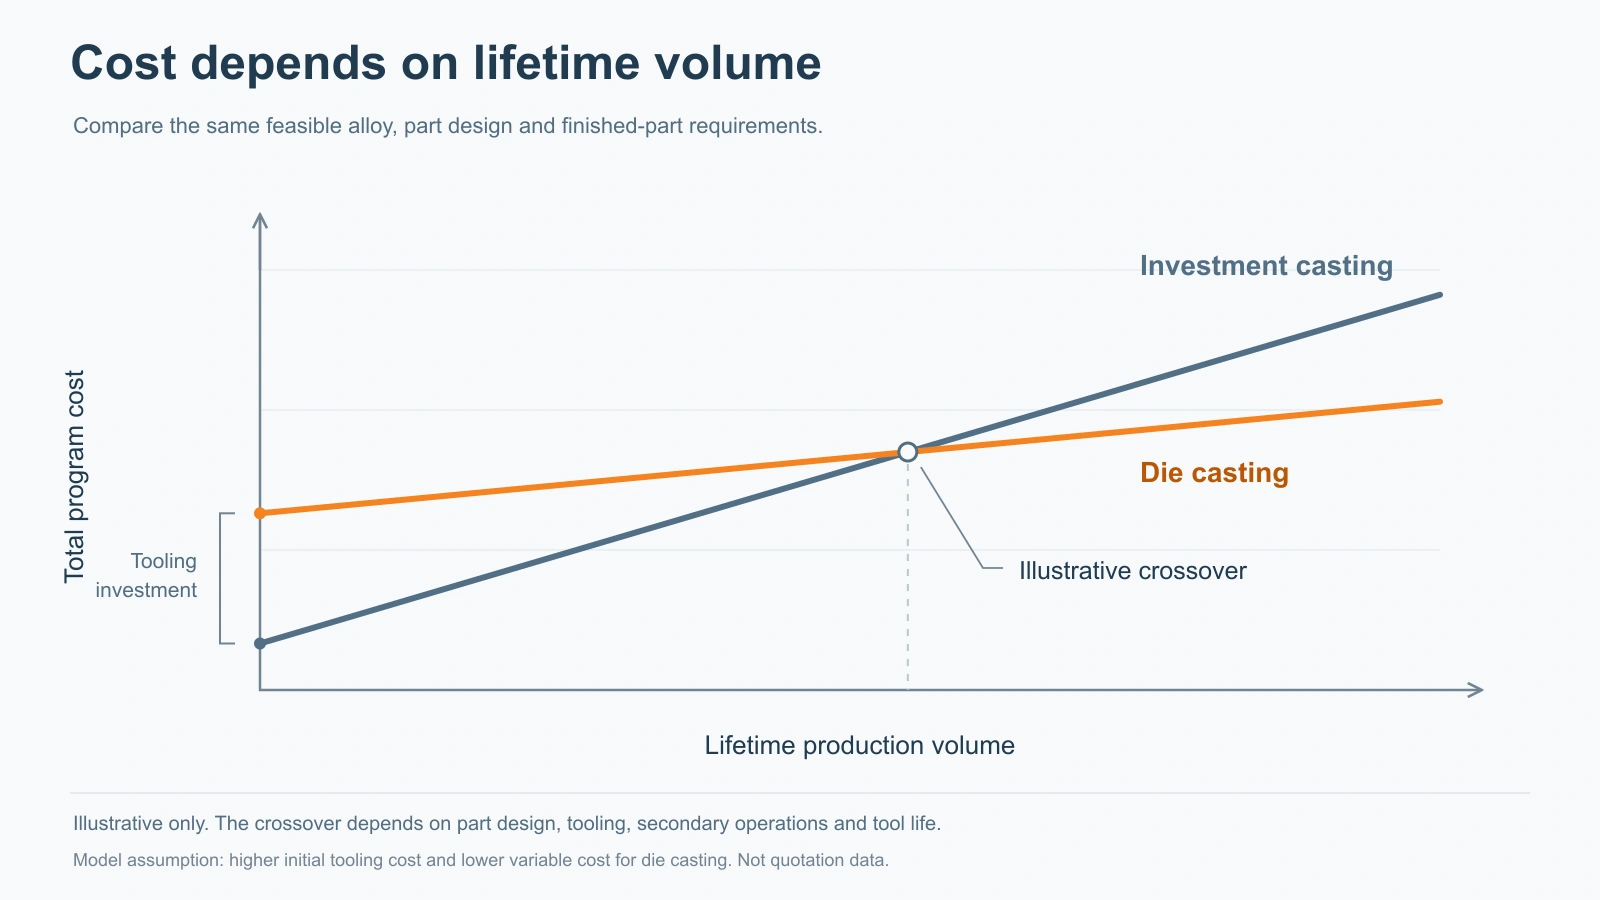
Comparing only the casting quote can hide the real economics.
A better model is:
Total Program Cost = Tooling + Casting Production + Machining + Finishing + Quality Cost + Tool Maintenance
Then divide that across the expected lifetime volume.
Investment Casting Cost Profile
Investment casting typically places less money into initial tooling and more cost into each production part.
That can work well when:
- Volume is moderate
- Material is expensive
- Geometry is complex
- Tooling risk should stay limited
Die Casting Cost Profile
Die casting moves a much larger share of cost into the permanent tool.
Once production volume becomes large enough, that fixed cost is spread across many parts and the fast casting cycle can drive unit cost down significantly.
The economic mistake is choosing die casting because:
“It is cheaper per part.”
That may be true at 100,000 pieces and completely false at 1,000 pieces.
The opposite mistake is choosing investment casting because:
“The tool is cheaper.”
A lower tooling bill may become insignificant if a long-running high-volume program carries a much higher variable cost for years.
The decision should be made using lifetime volume, not just the first purchase order.
How to Choose Between Investment Casting and Die Casting
A practical decision sequence is:
1. Check the Material
If the part requires steel, stainless steel, or a nickel/cobalt superalloy, investment casting is usually the relevant option between these two.
If the part uses aluminum, zinc, magnesium, or a suitable copper alloy, keep both routes open.
2. Estimate Lifetime Volume
Do not only ask how many parts are needed this month.
Estimate the expected total demand over the design’s life.
High, stable lifetime volume strengthens the die casting case.
3. Review Geometry and Ejection
Can the component release cleanly from a permanent die?
If not, calculate the tooling complexity required to solve that problem.
4. Check Wall Thickness
Thin non-ferrous walls and ribs strongly favor high-pressure die casting.
Highly complex geometry across a wider range of alloys may favor investment casting.
5. Define Internal-Integrity Requirements
Does the part require:
- High-temperature heat treatment?
- Welding?
- Pressure tightness?
- High structural ductility?
If yes, specify what type of die casting is being considered rather than treating all HPDC processes as identical.
6. Compare Total Program Cost
Include tooling, production, machining, finishing, quality requirements, maintenance, and lifetime quantity.
Only then compare the two processes financially.
Investment Casting vs Die Casting Selection Guide
| Project Requirement | Process to Evaluate First |
|---|---|
| Stainless steel component | Investment Casting |
| Carbon or alloy steel | Investment Casting |
| Nickel-based superalloy | Investment Casting |
| Complex aluminum part at modest volume | Investment Casting |
| Aluminum part at very high stable volume | Die Casting |
| High-volume zinc hardware | Die Casting |
| Thin-wall aluminum housing | Die Casting |
| Geometry difficult to eject from a steel die | Investment Casting |
| Lower initial tooling commitment | Investment Casting |
| Long-running repeat program | Die Casting |
| High-volume structural aluminum | High-Integrity Die Casting |
| Heat-treated structural aluminum | Compare Investment Casting and High-Integrity Die Casting |
The table is only an initial filter.
When aluminum components sit in the true overlap between the processes, DFM and lifetime-cost analysis are more useful than a generic rule.
How YTD Handles Investment Casting and Die Casting Projects
Investment casting is YTD Foundry’s in-house core casting process.
We handle tooling, wax pattern production, ceramic shell building, casting, heat treatment, CNC machining, inspection, and standard post-processing within our own production workflow.
Die casting is supported through specialized manufacturing partners, including hot-chamber, cold-chamber, and vacuum die casting capabilities.
That makes process selection especially important.
A stainless steel component should not be redesigned around die casting just to chase a lower cycle time.
Likewise, a stable aluminum housing needed in very high volume should not automatically be pushed into investment casting simply because investment casting is our in-house process.
Where both processes are technically possible, the useful comparison is the same finished drawing evaluated against material, lifetime quantity, tooling, mechanical requirements, machining, and total program cost.
Final Thoughts
Investment casting and die casting overlap much less than their similar names suggest.
Material usually narrows the decision first; lifetime volume narrows it next. Geometry, wall thickness, internal integrity, heat treatment, tooling risk, and total program cost then determine the better route.
If both processes remain technically viable—especially for aluminum—the right comparison is not casting price alone, but the cost and risk of producing the finished part over the entire program.
FAQs
Is Investment Casting More Expensive Than Die Casting?
Not in every production range. Investment casting usually requires lower tooling investment but higher variable cost per part. Die casting requires expensive permanent tooling but can achieve much lower unit cost when lifetime production volume is high enough.
Is Die Casting More Accurate Than Investment Casting?
Both are precision processes. Die casting can provide excellent production repeatability because each part is formed in the same rigid steel die. Investment casting provides strong near-net-shape accuracy across complex geometry and a much wider range of alloys.
Can Stainless Steel Be Die Cast?
Conventional high-pressure die casting is not normally used for stainless steel. Its very high melting temperature is incompatible with the reusable steel tooling and injection system used for standard die casting. Investment casting is widely used for complex stainless steel components.
Which Process Is Better for Aluminum?
Neither is automatically better. Die casting is especially strong for thin-wall aluminum components produced at high, stable volume. Investment casting can be attractive for lower volumes, difficult-to-eject geometry, or projects where lower tooling commitment matters.
Can Die Castings Be Heat Treated?
Some can. Conventional high-pressure die castings may contain trapped gas that creates blistering during high-temperature treatment. High-vacuum, squeeze, and semi-solid processes can reduce gas porosity and make suitable castings heat treatable.
Which Process Is Faster?
Die casting has a much faster production cycle after tooling is complete. Investment casting requires wax production, ceramic shell building, drying, dewaxing, firing, and pouring for every batch. However, tooling development time and design stability should also be considered when comparing total project lead time.