
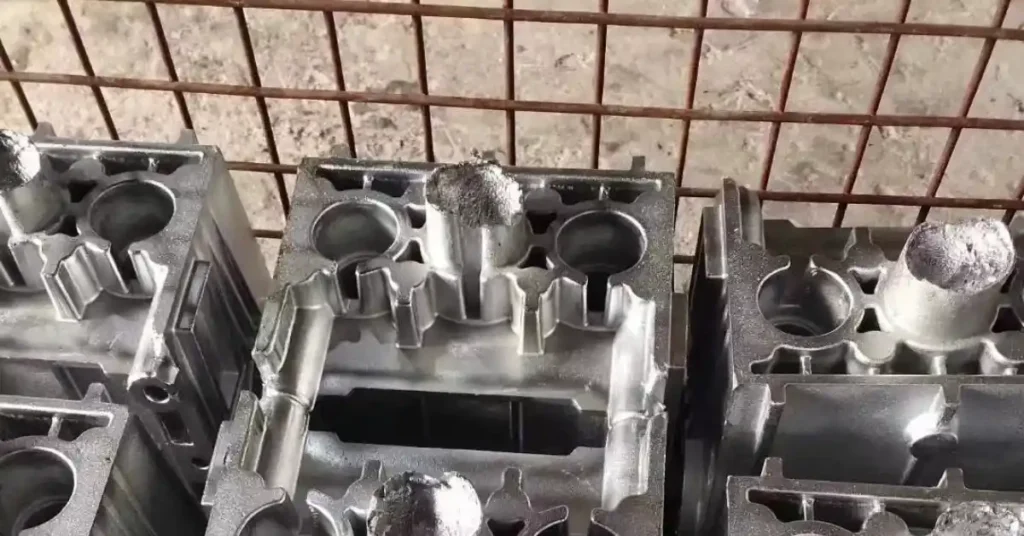
In case you’re interested to learn about aluminum investment casting, you’re in the right page. As we know, investment casting is a precision process that turns molten material into highly specific and detailed parts.
Most guides treat the process and the metal as separate subjects. That misses the point, because almost every problem you hit comes from how aluminum reacts inside the shell. Not all aluminum alloys work the same way inside a ceramic mold, though. So, the alloy you’ll choose will affect how the finished part performs, so it pays to know the options.
So, in this blog, we’ll be talking about what investment casting aluminum is all about, and everything you need to know about it!
Can You Cast Aluminum With Investment Casting?
Let’s get straight to the point and the answer is yes, you can. Aluminum is actually one of the easier metals you can use ceramic shells as molds on. Thanks to its low pour temperature, it, in itself will do most of the work for you.
The points below explain the main process advantages casting aluminum with investment casting creates.
Thinner Ceramic Shells
Since the mold faces less heat, many aluminum castings can use fewer ceramic layers. Shells around 6 mm to 8 mm is actually already enough. But, of course, its sizing will still depend on the size and shape of what you’re trying to make.
Lower-Cost Mold Materials
In many cases, fused silica can actually already handle the pouring temperature of aluminum. What this means is that the need for the more expensive refractory materials used with hotter metals is greatly reduced; you can say goodbye to expensive molds!
Easier Shell Removal
Once the casting cools, the ceramic mold usually breaks away with less effort because of its low chemical bonding and brittleness. You can definitely expect that delicate walls and small details are less likely to break and be damaged during cleanup.
Better Pattern Stability
Last but most definitely not least is the stability. Less thermal stress helps the wax pattern and shell keep their intended shape before pouring. As a result, the finished casting can stay closer to the original design.
Which Aluminum Alloys Work Best in Investment Casting
Alloys that you can machine can still be a problem for you when they’re inside ceramic molds. Just because they’re machinable doesn’t mean they’re perfect. Silicon usually improves flow, while magnesium and copper change the strength, heat resistance, and casting difficulty.
A356
With about 7% silicon, A356 fills detailed molds well and responds reliably to T6 heat treatment. Temperatures can reach around 262 MPa tensile strength with about 5% elongation, making it a balanced choice for many cast parts.
A357
When higher strength is what you’ll need, A357 is often the better choice because of its magnesium content being closer to 0.6%. After T6 treatment, the tensile strength can reach 345 MPa, though the melt needs tighter control to limit oxidation.
C355
Better performance above 150°C is the main reason to use C355. Its copper content, around 1.2%, improves heat resistance, but it also lowers corrosion resistance and can increase the risk of shrinkage porosity.
319
319 works well for cost-sensitive production because its silicon helps the metal fill the mold, while copper supports performance near 150°C. They’re commonly used for automotive brackets and other higher-volume parts.
535
Strong corrosion resistance makes 535, or Almag 35, useful for outdoor parts and harsh environments. Its high magnesium content also improves machinability, but the alloy is harder to pour cleanly and needs an experienced foundry.
NOTE: These are not the only aluminum alloys used in investment casting. They are simply some of the most common starting options.
Pros and Cons of Casting Aluminum With Investment Casting
We know that Newton’s third law of motion suggests that for every action, there’s always an equal and opposite reaction. This also applies here because every process has a price, and investment casting is no exception.
If you’re interested, here’s an honest view of both sides before you make the decision.
Pros of Investment Casting Aluminum
- You get fine detail straight from the mold. The wax pattern can pick walls up as thin as 1.5 mm, so the part comes out extremely close to its final shape.
- You can heat treat the part to full strength. Most die cast aluminum blisters in the oven, while these parts take a T6 cycle without trouble.
- Tooling is cheap and inexpensive to start. Wax dies cost far less than hardened steel molds that die casting needs.
- The surface comes out smooth and flawless. Finishes land between 1.6 and 3.2 µm Ra, which is often clean enough to paint or coat right away.
Cons Investment Casting Aluminum
- Porosity is a real risk. Molten aluminum soaks up hydrogen, then lets it back out as tiny bubbles while the part cools.
- Lead times run long. Each shell takes days to build up, so you wait longer than you would with die casting.
- The cost per part stays high. Every pour destroys its shell, and that expense never goes away no matter how many you order.
- Very thin walls are hard to fill. Aluminum is light, so it needs a vacuum or a pump to push it into the tightest sections.
Die Casting vs. Investment Casting in Cast Aluminum
Both processes cast the same metal, so the comparison comes down to what the shell or die does to it. Differences are bigger than what most buyers expect. Here’s a side-by-side comparison of die casting and investment casting.
| Factor | Investment Casting | Die Casting |
| Cooling Rate | Slow, insulating shell | Fast, chilled steel die |
| Heat Treatment | Pull T6 possible | Usually blisters |
| Tooling Cost | Low | High upfront |
| Break-Even Volume | Under about 5,000 | Above about 10,000 |
| Wall Thickness | 1.5 mm (typical) | Down to 1mm |
| Alloy Range | Wide, includes 535 | Narrow, mostly A380 |
Heat treatment is actually one of the most crucial aspects that decides most projects. High-pressure die casting traps air in the mold, and that gas expands during solution treatment, raising blisters. Die cast aluminum parts are usually stuck with as-cast properties, while investment casts something that can be heat-treated to full durability and strength.
Die casting still wins on cost at volume, and that’s simply true. If you need 50,000 identical housings a year, the die pays for itself and investment casting can’t catch it.
Is Aluminum Investment Casting the Right Choice For You?
Aluminum investment casting fits your application when your part is extremely detailed, complex, when the weight matters, and when volumes aren’t in the tens of thousands. If you need heat treated properties in a cast shape, investment casting is usually the practical route.
Here at HDC, aluminum investment casting is work we do every day, and we’re hard to beat on it. For more than 8 years, we’ve been in the business and we ensure that our clients get the specific component they need. We pour the part, then machine and finish it in house, so nothing gets lost between suppliers.
Send a sketch along with how many you need and the alloy targets you have. We’ll tell you honestly whether aluminum investment casting suits the part, or whether another process would serve you better. Get a free quote!


