
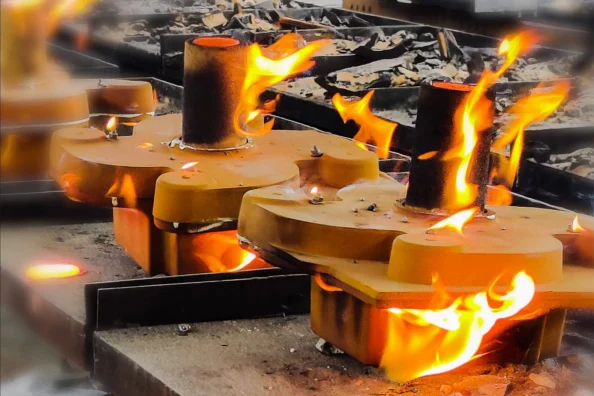
1. What is Metal Casting: The Definition
Metal casting is one of the oldest and most versatile manufacturing processes, capable of producing everything from miniature precision components to massive industrial structures.
Despite there being dozens of casting processes, they all share the same fundamental principle: creating a mold cavity that perfectly matches the geometry of the final part, which will be filled with melted metal, allowed to solidify, and removed to form the finished product. Just like you fill the ice cube tray with water and let it freeze to take its form.
Four Core Steps of Metal Casting
Regardless of the casting process, the core steps are the following four:
- Mold making: Create a mold according to the shape of the customized part (sand mold, metal mold, ceramic shell, plaster shell, etc.).
- Metal melting: Heat the metal until it becomes liquid.
- Pouring and forming: Pour or press the molten metal into the mold cavity.
- Post-processing: After the metal has completely solidified, it is demolded, cut, and the surface is cleaned. Heat treatment or machining may be performed if necessary.
2. Advantages of Manufacturing Metal Parts with Casting
Limitless Size & Weight
Casting can produce everything from small, precision parts weighing a few grams to heavy structural components weighing hundreds of tons.
Exceptional Material Adaptability
Almost all molten metals and alloys can be used for casting; you can choose the materials you want based on the project requirements.
Maximum Material Utilization
The cast blank closely resembles the shape and size of the final product, resulting in minimal waste.
High Customization Flexibility
Casting can produce single pieces, small batches, and large quantities at a high cost-performance ratio.
Infinite Geometric Shape Freedom
Casting can produce parts that are difficult to machine, such as those with internal cavities, complex curved surfaces, and thin walls.
3. Types of Metal Casting Processes
We will introduce as many conventional and special casting processes as possible based on mold characteristics, pouring methods, and molding methods, so that you can choose the appropriate casting process for your customized products.
Expendable Mold Casting
Expendable mold casting usually uses materials that are cheap and easy to shape for the mold. After the metal parts are formed, the mold needs to be destroyed to remove the parts. Therefore, we must consume one mold for each product we produce.
Investment Casting
A wax model of the part is made, which is then repeatedly dipped in slurry and sand to create a ceramic shell. After dewaxing, metal is poured in, and the shell is removed after cooling to obtain the casting.
This method is suitable for projects with high requirements for precision and surface finish.
Sand Casting
Use wooden or metal models to press cavities into clay sand, pour molten metal, and after cooling, remove the sand to obtain castings.
This process has low production costs, the dimensional tolerance is acceptable, and it is suitable for heavy, large parts with low precision requirements.
Lost Foam Casting
Bury the foam model coated with a refractory coating into dry sand, and pour molten metal directly. After the foam vaporizes, the molten metal takes its place.
Lost foam casting is suitable for products with complex internal structures and intricate designs, such as engine cylinder blocks.
Permanent Mold Casting
Permanent mold casting usually uses molds made of expensive heat-resistant steel or cast iron, which can withstand countless metal pourings and can be reused for a long time as long as the molds are not damaged.
Gravity Casting
Pour the molten metal into a permanent steel mold using gravity, allowing it to naturally fill and cool into shape.
Without relying on external pressure, the casting has almost no internal porosity and a dense structure, making it suitable for products with high strength requirements.
Die Casting
Molten metal is injected into a steel mold at high speed and pressure using a hydraulic piston, where it quickly solidifies and takes shape under pressure.
When the product batch is large and demand is stable, efficient production and ultimate cost-effectiveness can be provided.
Centrifugal Casting
Pour the molten metal into a high-speed rotating metal cylindrical mold, and the centrifugal force causes the molten metal to adhere to the inner wall and solidify.
The centrifugal force can expel impurities and gases, resulting in a casting that is pure inside, without porosity or defects.
Squeeze Casting
After pouring the molten metal into the mold, use a mechanical press to apply extremely high pressure before solidification until it is completely solidified.
The pressing eliminates internal voids, resulting in a product with high density and high strength.
4. Metals Casting Materials
Aluminum Alloys
Aluminum alloys have low density, corrosion resistance, and good thermal conductivity. After melting (melting point around 660°C), they exhibit good fluidity, allowing them to fill complex, thin-walled molds, making them one of the most commonly used non-ferrous metals in casting.
Our customers usually choose aluminum alloys to cast lightweight products with complex shapes.
- Common Grades: A356, ADC12,A380(suitable for die casting)
- Applicable Processes: Precision investment casting, die casting, sand casting…
- Common Applications: Auto parts, aerospace structural components, radiator casing, electronic device housing…
Cast Iron
Cast iron is a metal material specifically designed for casting. It flows easily, fills every mold corner, and shrinks very little during solidification.
Therefore, cast iron castings have high dimensional accuracy, complete details, and good surface quality, making them the first choice for most casting products.
- Common Grades: Gray iron-HT150, HT250, ductile iron-QT400-18, QT600-3
- Applicable to every casting process
- Common Applications: Engine blocks, machine tool bases, brake drums…
Carbon Steel & Steel Alloys
Cast steel and steel alloys, possessing both high strength and toughness, are commonly used ferrous metal materials in casting processes because they can withstand high-intensity impacts and heavy loads.
- Common Grades: AISI 1020 / 1045, 4140 / 8620
- Applicable Processes: Investment casting, precision casting, sand casting…
- Common Applications: equipment parts, railroad couplers, hydraulic components…
Stainless Steel
Stainless steel, as a type of steel alloy, not only has high strength and toughness but also possesses excellent corrosion resistance and a beautiful appearance.
It is often used by our customers to cast products for the chemical, food, medical equipment, and marine engineering industries.
- Common Grades: 304(CF8),316(CF8M) , 304L(CF3),316L(CF3M),17-4PH…
- Applicable Processes: Investment casting, precision casting, sand casting
- Common Applications: Pump bodies, valve parts, marine hardware, food processing equipment…
Superalloy
Products cast from superalloys are super resistant to heat, maintaining high strength, creep resistance, corrosion resistance, and oxidation resistance even in environments above 600°C.
- Common Grades: Inconel 718 / Inconel 625, Hastelloy C276, Monel 400…
- Applicable Processes: Investment casting
- Common Applications: Aerospace components, gas turbine parts, chemical processing equipment…
Magnesium Alloys
Magnesium alloys are the lightest metal materials, and their excellent flow properties after melting make them suitable for filling intricate mold cavities.
If you want to customize lightweight, thin-walled parts, magnesium alloys are also a good choice.
- Common Grades: AZ91D, AM60B
- Applicable Processes: Die casting, sand casting
- Common Applications: Automotive instrument panels, seat frames, laptop/phone housings
Zinc
Zinc alloys offer excellent fluidity for precise mold replication. Their low melting point (~390°C) reduces thermal shock, helping control mold costs.
Our customers typically choose zinc alloys for mass production of low-cost, dimensionally precise, and aesthetically pleasing thin-walled small parts.
- Common Grades: Zamak 3, Zamak 5
- Applicable Processes: Die casting
- Common Applications: Lock parts, faucet handles, luggage hinges, electronic connectors…
Copper Alloys
Copper alloys offer excellent corrosion resistance, wear resistance, and thermal and electrical conductivity.
- Common Grades: Brass, bronze
- Applicable Processes: Sand casting, centrifugal casting
- Common Applications: Valve bodies, pipe fittings, marine propellers; bronze: gears, marine propellers, sculptures…
Titanium Alloys
Titanium alloys are high in strength, have excellent corrosion resistance, and are highly biocompatible, but they are extremely reactive in the liquid state, so they are usually cast in a vacuum environment.
- Common Grades: ZTC4 (Ti-6Al-4V)
- Applicable Processes: Vacuum investment casting, vacuum centrifugal casting
- Common Applications: Aircraft engine casings, surgical implants…
Gold & Silver
For precious metals such as gold and silver, casting can achieve complex hollow patterns with minimal material waste.
- Applicable Processes: Investment casting
- Common Applications: Jewelry
5. Industrial Applications of Metal Casting
Automotive & E-Mobility
- Specific Applications: Engine block, cylinder head, transmission case, brake caliper, suspension system components, wheels…
- Core Process: Die casting, gravity casting, lost foam casting, investment casting…
- Common Materials: Aluminum alloy, cast iron, magnesium alloy…
Aerospace & Marine Engineering
- Specific Applications: Turbine blades, engine impellers, fuel system components, structural supports, casings; propellers, marine engine blocks, rudder blades, pump bodies, valves…
- Core Process: Investment casting, vacuum casting, sand casting
- Common Materials: superalloy, titanium alloy, cobalt-based alloy, stainless steel…
Heavy Machinery
- Specific Applications: Construction machinery parts, mining equipment parts, machine tool beds, hydraulic pump bodies and valves, large gearboxes
- Core Process: Sand casting
- Common Materials: Cast steel, ductile iron
Energy & Power
- Specific Applications: Steam/gas turbine blades, nuclear reactor components, petrochemical equipment parts, power generation equipment parts
- Core Process: Precision casting, sand casting
- Common Materials: Heat-resistant steel, stainless steel, superalloys
Healthcare
- Specific Applications: Artificial joints (hip, knee), surgical instruments, dental implants, medical device housings, and structural components
- Core Process: Precision casting
- Common Materials: Cobalt-chromium-molybdenum alloys, titanium alloys, stainless steel
Infrastructure & Municipal
- Specific Applications: Pipelines, fittings, valves, manhole covers, building hardware, railway components (turnouts, fasteners), ship propellers
- Core Process: Sand casting
- Common Materials: Gray cast iron, ductile iron, bronze
Infrastructure & Municipal
- Specific Applications: Home appliances (refrigerators, air conditioner compressors), kitchenware, bathroom hardware, gardening tools, furniture accessories, musical instruments (piano iron plates)
- Core Process: Die casting, sand casting
- Common Materials: Aluminum alloys, zinc alloys, cast iron
6. Common Metal Casting Process Comparison
| Process | Investment Casting | Die Casting | Sand Casting |
|---|---|---|---|
| Applicable Materials | Steel, stainless steel, aluminum, bronze, titanium, superalloys… | Non-ferrous: aluminum, zinc, magnesium, copper alloys… | Cast iron, steel, aluminum, bronze, magnesium… |
| Design Flexibility | Very high – complex shapes, fine details, undercuts possible | Moderate – limited by die opening and draft angles; undercuts difficult | High – can produce large, complex shapes; cores allow internal cavities |
| Upfront Cost | Moderate to high (pattern, shell tooling) | Very high (metal die, hydraulic system) | Low (wood or metal pattern, simple flasks) |
| Unit Cost | Moderate (low to medium volume) | Very low (high volume) | Moderate to high (depends on volume & labor) |
| Unit Weight Range | Grams to ~50 kg | Grams to ~20 kg (typical <10 kg) | Grams to >100 tonnes |
| Production Speed | Slow (multiple steps, drying time) | Very fast (seconds to minutes per cycle) | Slow to moderate (mold preparation, cooling) |
| Tolerance Level | CT5–CT7 | CT4–CT6, tightest | CT8–CT12 |
| Casting Surface Roughness | Ra 1.6–3.2 µm | Ra 0.8–1.6 µm | Ra 6.3–25 µm |
7. How to Choose the Right Metal Casting Process
In fact, no casting process is a panacea. Considering the following factors, we will recommend the most suitable customization solution for you.
Part Dimensions & Weight
- Under 10 kg with high volume: die casting or investment casting
- Over 50 kg or even several tons: sand casting
Precision & Surface Requirements
- Very tight (CT4–CT6, Ra < 1.6 µm): die casting or precision investment casting
- Moderate (CT7–CT9): investment casting or gravity casting
- Loose (CT10 or above): sand casting (most economical)
Production Volume
- 1–1,000 parts: sand casting
- 1,000–50,000 parts: investment casting or gravity casting
- 50,000+ parts: die casting (lowest part cost)
Material Type
- Cast iron, cast steel, superalloys: sand casting or investment casting
- Aluminum, zinc, magnesium alloys: die casting, investment casting, or gravity casting
- Titanium, cobalt-chromium alloys: investment casting (with vacuum assistance)
Tooling vs Part Cost
- Want to save on tooling: sand casting
- Higher tooling for lower part cost: die casting or investment casting
8. Post-processing for Casted Metal Parts
In order for the product to reach the final dimensions, surface, and performance requirements, after removing the casting from the mold, we still need to carry out one or more post-processing operations on the casting.
Sand / Bead Blasting
Casting surfaces usually have residues such as sand grains, oxide scale, and coatings, which need to undergo sand blasting or bead blasting, that is, cleaning the surface and improving the surface finish of the casting by high-speed spraying of sand grains or glass beads.
CNC Finishing
Simple casting cannot meet the tolerance requirements of all dimensions, so subsequent precision machining, such as CNC milling, CNC turning, and drilling, is required to ensure the accuracy of critical mating surfaces, threaded holes, and other parts of the casting.
Heat Treatment
Heat treatment ensures castings meet hardness, strength, and toughness requirements. It improves mechanical properties or removes internal stresses.
Common processes include normalizing, annealing, solution treatment, and aging for aluminum alloys and superalloys, and stress relief annealing.
Surface Finishing
Depending on the product’s usage environment and aesthetic design, additional surface finishing can be applied to the casting, such as painting, powder coating, anodizing of aluminum alloys, electroplating, passivation, etc.
We can provide one-stop customized services from casting to machining to surface treatment, selecting the most suitable processing technology for your product, and ensuring the quality and delivery time of each step.
9. Casting vs Other Metal Manufacturing Processes
Casting vs Injection Molding
Injection molding produces lightweight, cheap parts with short cycle times. But plastic parts cannot withstand high heat or heavy loads — they soften, deform, and fail quickly.
Casting, in contrast, pours molten metal into a mold. Metal parts are strong, heat-resistant, and durable, ideal for industrial use.
Casting vs CNC Machining
CNC machining cuts from solid material, achieving high precision with no heating or mold trials. But it removes most of the material, generating significant waste.
Casting, instead, uses material efficiently and is ideal for custom mass production. You can get near-net shape parts with little scrap.
Casting vs Forging
Forging heats metal to a red-hot state and hammers it into shape. So, forged parts are dense and strong, ideal for high pressure and impact.
But forging only makes simple, solid shapes, while casting produces complex, intricate, and hollow designs.
Casting vs 3D Printing
3D printing builds parts layer by layer with no tooling and high geometric freedom. It is slow, weak, and expensive for medium to large volumes.
Casting, on the other hand, is fast, strong, and cost-effective for production runs.
Casting vs Fabrication
Fabrication cuts and welds sheet metal — low startup cost for simple, low-volume jobs. However, it creates waste, multiple steps, and weak joints.
In contrast, casting pours molten metal into a mold, producing complex, one-piece parts with uniform strength and minimal scrap.
10. Metal Casting Design Considerations
Drawing design directly affects tooling and casting production. Below are key design elements based on our experience and customer feedback. Consider them to control lead time and cost.
Draft Angle
Draft angle (typically 0.5°–3°) helps castings release smoothly.
Without it, forced removal can scratch the part or jam the mold.
We’ll recommend the right angle based on your part shape and process to lower the tooling cost and scrap rate.
Wall Thickness
Uniform wall thickness (typically 1.5–5 mm) ensures smooth mold filling and even cooling.
Uneven or overly thick walls cause shrinkage or cracks; too thin leads to misruns.
We’ll advise smooth transitions, radii, ribs, or core removal to make your casting lighter, cheaper, and better.
Parting Line
The parting line is where mold halves meet; it determines flash location.
Poor placement puts critical dimensions on the parting line, ruining surface finish and increasing deburring cost.
We’ll confirm the best parting line position and flag dimensions that must avoid it, giving you both a good appearance and a low cost.
Undercuts
Undercuts (side bosses, internal grooves, or side holes) block mold release.
Ignoring them forces complex tooling or impossible die opening.
We’ll identify all undercuts and tweak the design to eliminate them—reducing tooling cost.
Cores
Cores create internal cavities, hollow passages, or undercuts.
Overly complex cores risk being washed out by molten metal and leaving trapped sand that’s hard to clean.
We’ll evaluate and optimize the safest core hole size for you—ensuring smooth, clean internal passages.
Gating System in Casting
The gating system directs molten metal smoothly into the mold cavity.
Poor channel design creates violent turbulence and traps air, leading to invisible porosity and slag inclusions.
We will calculate the optimal ingate position before tooling—ensuring a fully dense casting.
Casting Tolerances
Casting tolerance is the allowable dimensional deviation, typically ISO 8062 CT7–CT12. Precision investment casting can reach CT4–CT6; sand casting usually CT8–CT9.
Overly tight tolerances on the drawing cause high scrap rates.
We’ll suggest cost-effective tolerances based on your process and volume, or add machining allowance and provide post-casting CNC finishing.
Not sure about your design? Send us the drawing. We’ll review it, suggest improvements, and provide one-stop service from design to production.
11. Common Metal Casting Defects
Casting defects directly affect the performance and yield of products. Only by understanding the types of casting defects and their causes can we apply the right remedies and cast qualified products.
Porosity
Porosity is tiny gas pores in a casting (like a sponge), from trapped gas in molten metal or poor venting.
It harms sealing and, if machined, can weaken the part or cause failure.
Shrinkage
Shrinkage forms irregular, rough cavities in thick casting sections (slowest-cooling hot spots), caused by solidification contraction without timely metal refill.
This weakens the structure, leading to sudden brittle fracture under impact or tension.
Sink Marks
Sink marks are surface pits on castings (often behind thick walls or ribs), when outer metal solidifies first, while inner thick sections shrink without refill, so atmospheric pressure creates pits.
They harm surface finish and dimensional accuracy.
Dross/Slag Inclusions
Dross (slag) inclusions are hard, dark non-metallic impurities in castings, from slag or oxides during melting or pouring.
If CNC machining is performed later, they damage CNC tools and ruin the surface finish.
Sand Inclusions / Sand Holes
Sand holes (sand inclusions) are rough pits containing sand or ceramic particles, resulting from cracked investment shells or collapsed sand molds.
They cause localized pitting, damage machining tools, and make coatings blister or peel off.
Misrun
A misrun is an incomplete casting where metal fails to fill thin sections or corners, due to low temperature or slow pouring.
This defect is irreversible and makes the part unusable.
Cold Shuts
Cold shuts are smooth, rounded gaps on a casting surface, due to low temperature causing premature solidification.
These gaps can crack under stress, leading to structural failure.
12. Metal Casting Quality Control
Quality control is essential during both the casting process and post-production to ensure product performance and quality.
Chemical Analysis
Verify that the composition of casting materials meets standards, such as the content of elements like carbon(C), silicon(Si), sulfur(S), and phosphorus(P).
Spectrometer Testing
Spectrometers rapidly analyze the chemical composition of molten metal or finished products, ensuring material traceability.
CMM Inspection
Coordinate Measuring Machines (CMMs) perform high-precision automatic inspection of critical dimensions in castings, ensuring geometric tolerances.
X-Ray Inspection
X-ray inspection checks castings for hidden defects such as porosity, shrinkage cavities, and inclusions.
Dye Penetrant Testing
Dye penetrant testing detects surface defects such as cracks, porosity, and cold shuts; it is simple to operate and low-cost.
Mechanical Testing
Testing the tensile strength, hardness, elongation, and other mechanical properties of castings to verify compliance with design requirements.
If you need them, we can provide all the above quality control inspection documents to safeguard the quality of your products.
13. Conclusion
Metal casting gives you great design freedom, saves material, and keeps costs low. Learn the right process, avoid common defects, and apply proper finishing — you’ll get high-quality parts. We offer one-stop service from design review to final casting, backed by strict QC. Send us your drawing, and we’ll make it happen.
FAQs
How do I choose the right casting process for my part?
Consider part size, weight, tolerance, surface finish, annual volume, and material. Use our fivequestion guide to narrow down options. Still unsure? Send us your drawing for a free recommendation.
What are the most common casting defects, and how can they be avoided?
Common defects include porosity, shrinkage, sink marks, inclusions, misruns, cold shuts, and mismatches. They are avoided by proper gating design, controlled pouring temperature, clean materials, and rigorous process simulation. Our factory uses vacuum degassing, Xray inspection, and simulation software to minimize defects.
Can you provide post-casting services like CNC machining or heat treatment?
Yes. We offer a full range of postprocessing: sand/bead blasting, CNC finishing, heat treatment (annealing, solution aging, stress relief), and surface finishing (painting, anodizing, plating, etc.). One-stop service from casting to finished part.
What materials are commonly used in casting?
Aluminum alloys, cast iron, carbon steel, stainless steel, superalloys, magnesium alloys, zinc alloys, copper alloys, titanium alloys, and even precious metals like gold and silver. Each material has specific advantages in weight, strength, corrosion resistance, or cost.
How do you ensure the quality of castings?
We perform chemical analysis, spectrometer testing, CMM inspection, X-ray inspection, dye penetrant testing, and mechanical testing. All quality control documents are available upon request to guarantee every casting meets your specifications.
Do you offer design assistance for casting drawings?
Yes. Our engineers review your drawing and suggest improvements on draft angles, wall thickness, parting line, undercuts, cores, gating system, and tolerances. We help you avoid costly mistakes before tooling.


