
CF8M Stainless Steel Threaded Housing with Cast Fins
Project Focus
Product Views
Cast Body and End Fins
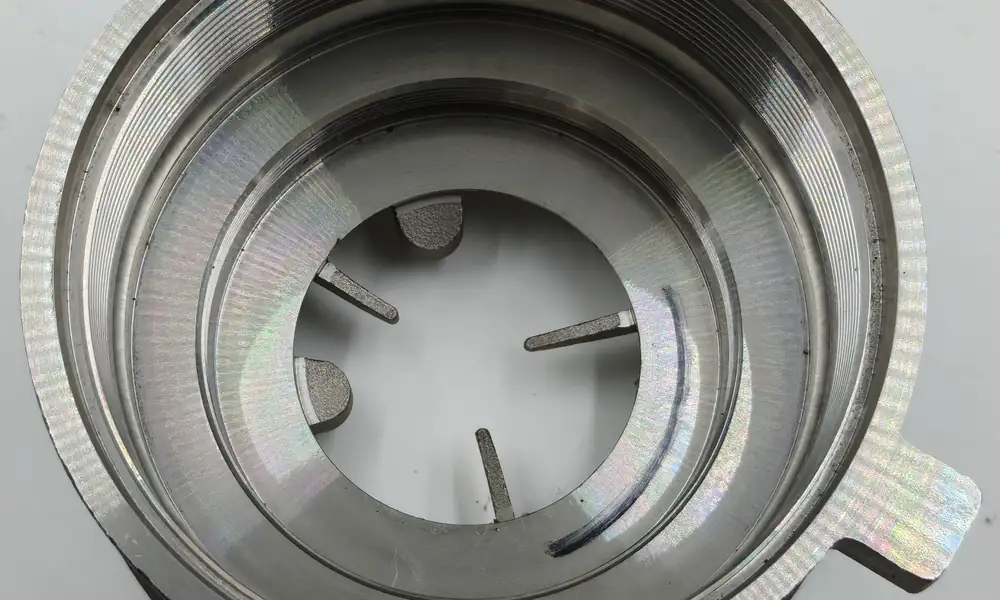
Stepped Internal Geometry
Casting the Tapered Fins as Part of the Housing
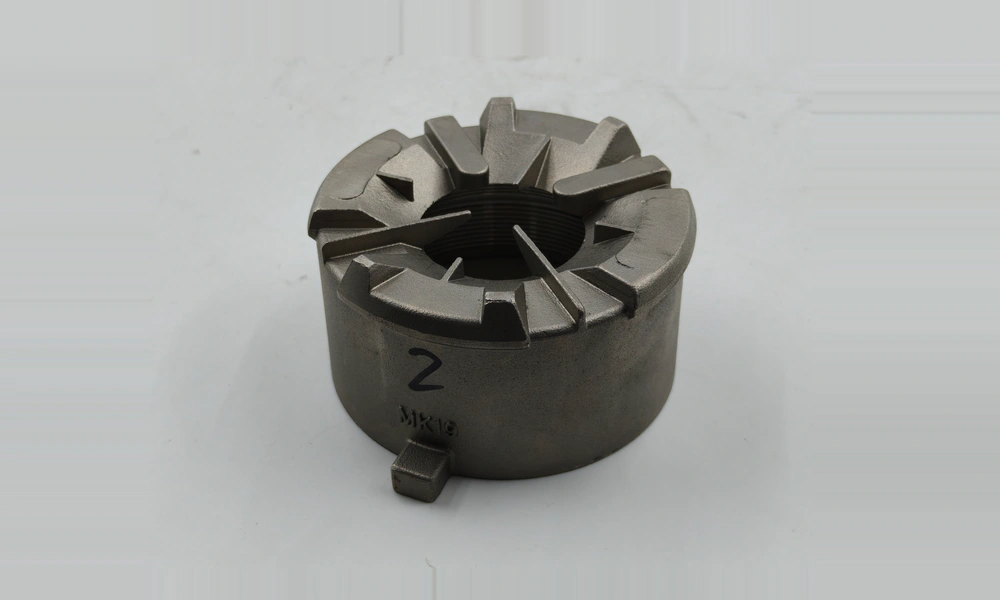
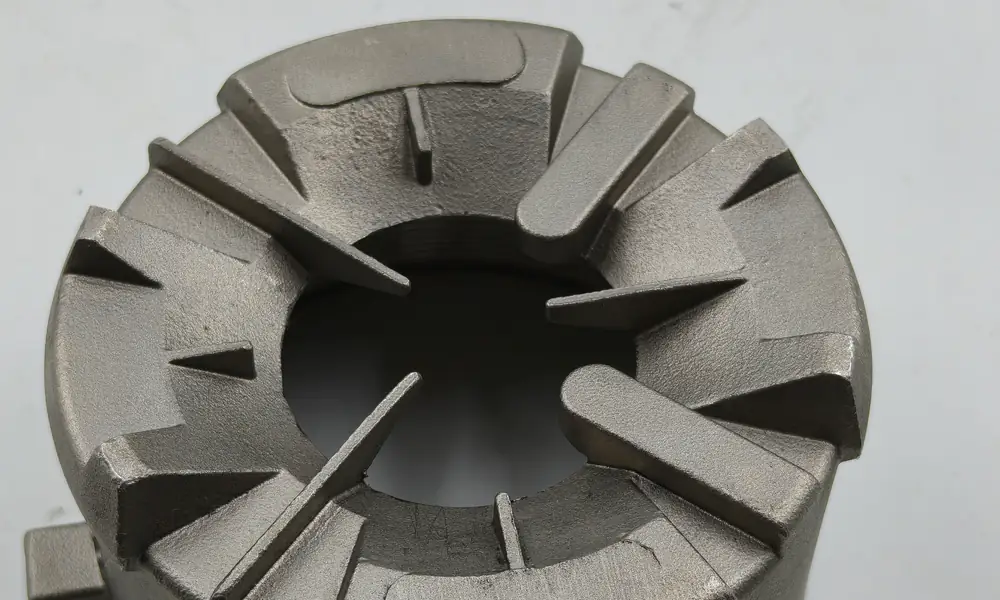
The tapered fins were cast integrally with the CF8M housing. The fins have a minimum thickness of approximately 2.5 mm and project around 20 mm from the body.
Fin definition starts with the wax pattern. Complete wax filling reproduces the narrow tips, tooling vents release displaced air, and controlled pattern removal protects the projecting features before shell building.
During casting, the thin ends lose heat faster than the surrounding body. The gating layout, shell temperature and pouring conditions control metal flow into these sections before solidification. These process controls preserve complete fin tips and defined edges.
Machining Two Threaded Diameters Within a Stepped Interior
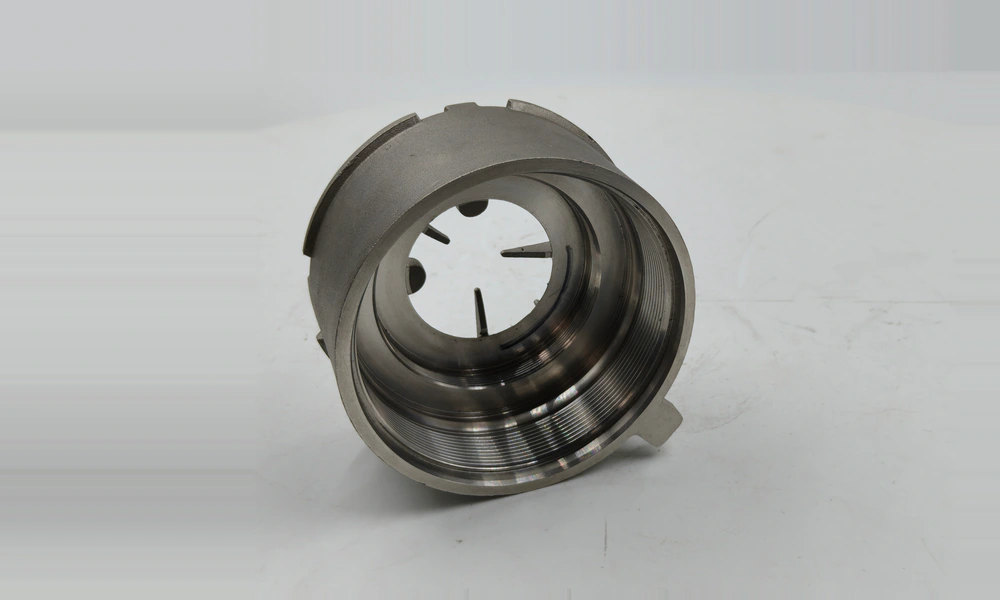
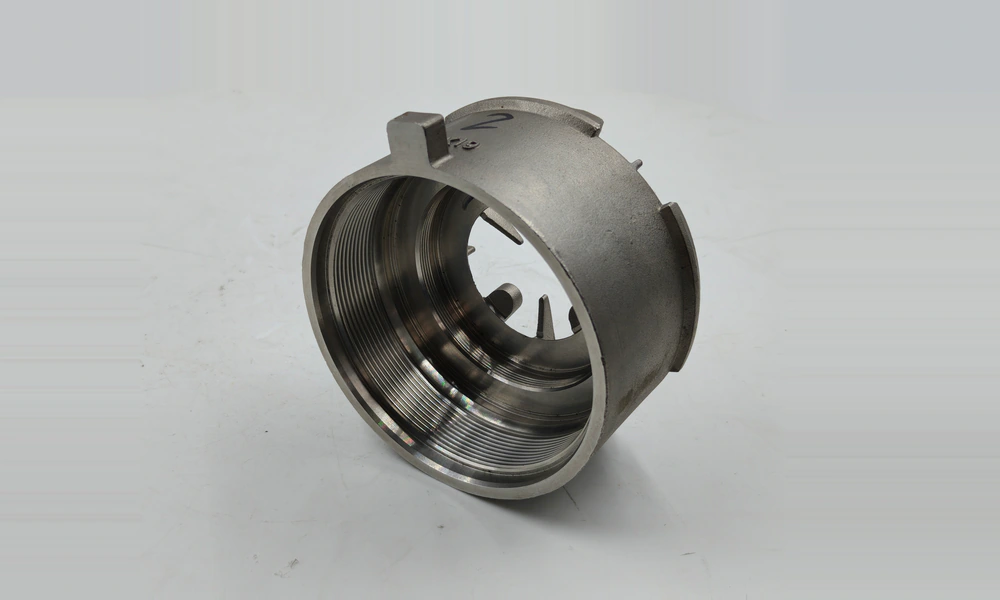
After casting, YTD machined the housing’s internal bore surfaces, shoulders and two threaded sections. The larger thread sits near the entrance, while the smaller thread is recessed deeper inside the component.
The stepped geometry governs tool access and workholding. Clamping on the cylindrical body keeps loads off the projecting fins. The machining sequence provides clearance for tools to reach the recessed thread and adjacent shoulders.
Machining establishes the finished thread profiles, bore diameters and shoulder positions. The completed component retains its integral cast fins on the outside and provides finished threaded connections and stepped surfaces inside.
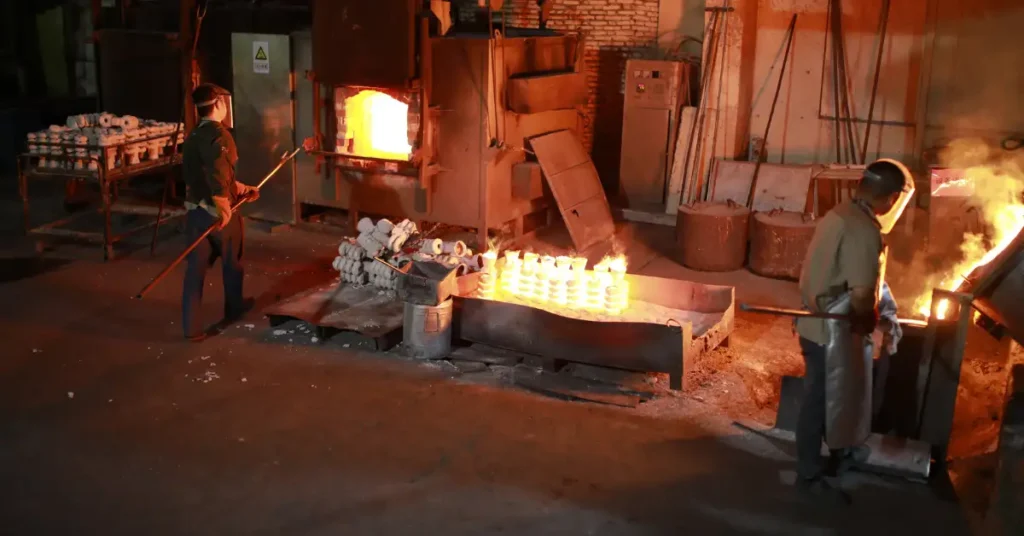
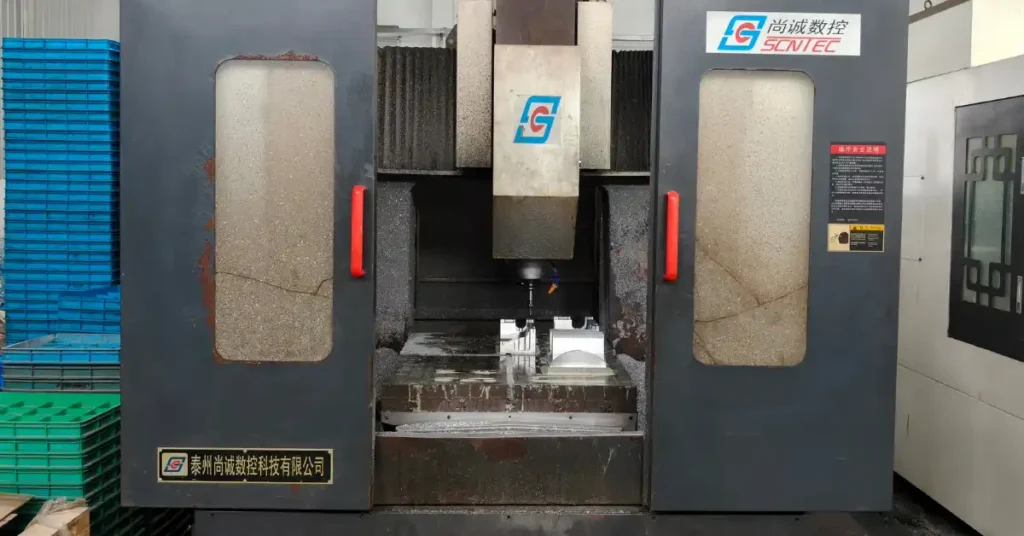
Inside Our Factory
Related Casting Projects
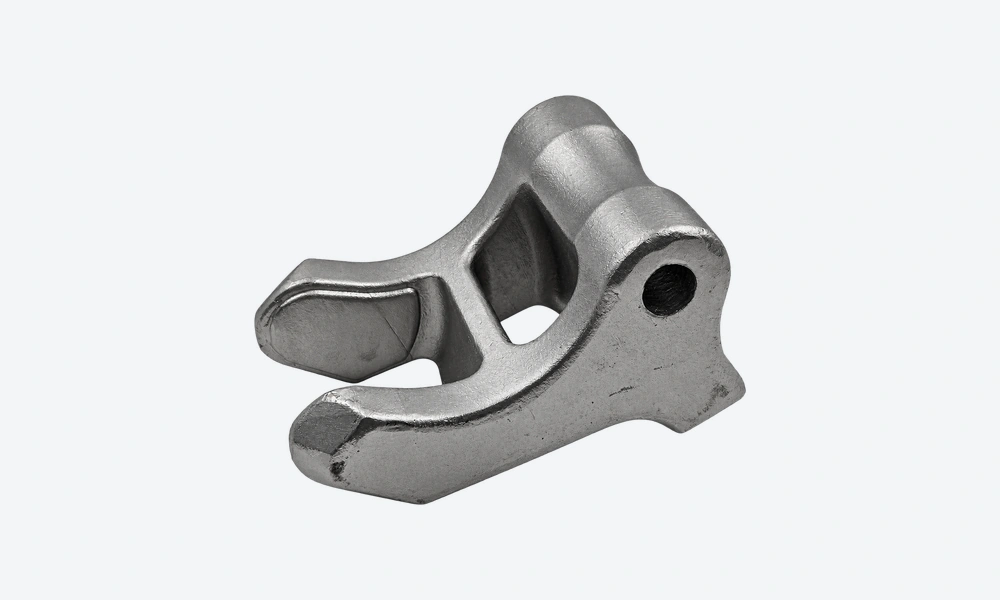
Stainless Steel Fork Casting with a Shot-Blasted Finish
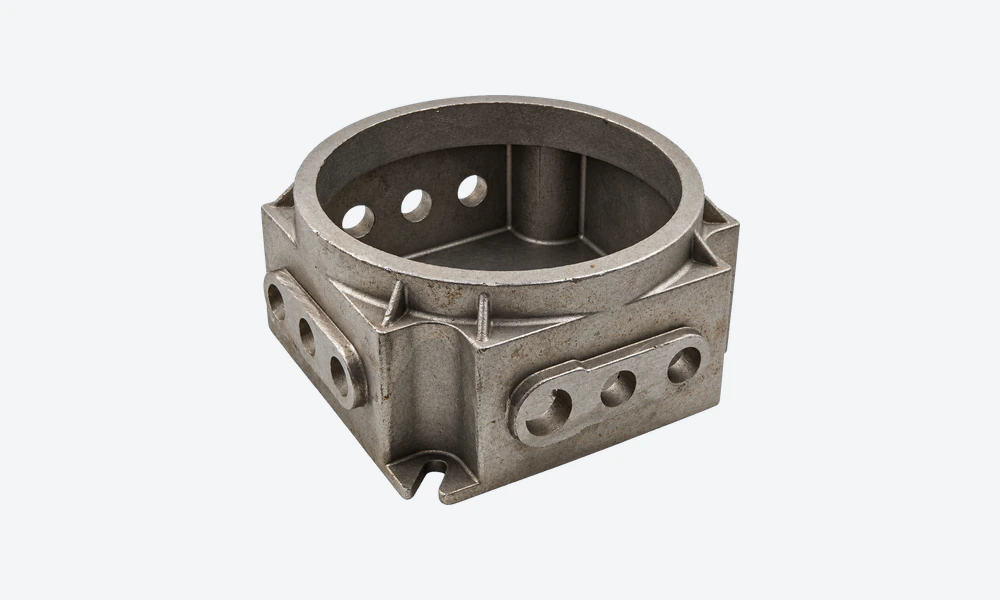
Carbon Steel Housing Casting with Side Openings
Stainless Steel Impeller Casting with Curved Vanes
CF8M Neck Flange
Aluminum Fishing Reel Frame
CF8 Three-Way Pipe Fitting
CF8 Quick-Connect Coupling Body
CF8M Carcass Hook
Stainless Steel Flow Meter Body
CF8M Pump Valve Body
Need Casting and Machining for a Complex Part?
Send your drawing or 3D model, material specification, order quantity and assembly requirements. YTD will review the casting geometry, internal features and machining scope to develop a production plan for your part.