“Vacuum casting” can describe more than one manufacturing process.
In prototyping, it usually means casting polyurethane resin into a silicone mold under vacuum. In metal manufacturing, vacuum may instead be used during melting, mold filling, or high-pressure die casting.
These processes solve very different problems.
This guide first explains the vacuum casting process most people find when searching the term, then shows how it differs from vacuum investment casting and vacuum die casting so you can identify which process actually fits your project.
What Is Vacuum Casting?
The most common meaning of vacuum casting is a low-volume manufacturing process that uses a flexible silicone mold to reproduce a master model in polyurethane or similar casting resin.
A typical application might require:
- 10 prototype housings
- 20 product samples
- A short batch for market testing
- Several cosmetic models
- Flexible or transparent prototype components
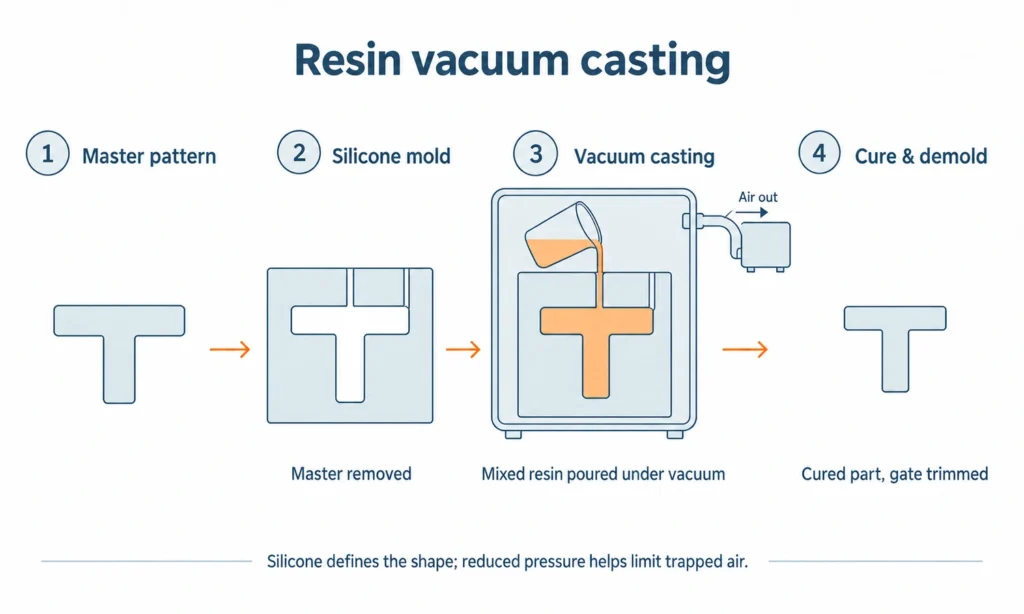
Instead of machining every prototype individually or investing in an injection-molding tool, a manufacturer creates one accurate master model and uses it to make a silicone mold.
Liquid resin is then cast into that mold under vacuum.
The vacuum helps remove trapped air so the resin can reproduce fine surface details and complex features more reliably.
Formlabs and other rapid-prototyping sources describe this process as a bridge between one-off prototyping and full production tooling.
However, this is only one meaning of vacuum casting.
In metal foundries, the word “vacuum” can refer to something very different.
Three Different Processes Called Vacuum Casting
The easiest way to avoid confusion is to separate the term into three manufacturing contexts.
| Verfahren | Material | What the Vacuum Does | Typical Goal |
|---|---|---|---|
| Resin Vacuum Casting | Polyurethane and similar resins | Removes air during mold filling | Prototype and low-volume plastic-like parts |
| Vacuum Investment Casting | Nickel, cobalt, titanium and other suitable metal alloys | Controls melting atmosphere and/or pouring conditions | High-performance metal castings |
| Vacuum Die Casting | Mainly aluminum and other die-cast alloys | Removes gas from the metal die before/during injection | Dense, high-volume structural castings |
These are not variations of one basic process.
They use different molds, different materials, different equipment, and serve very different production volumes.
How Resin Vacuum Casting Works
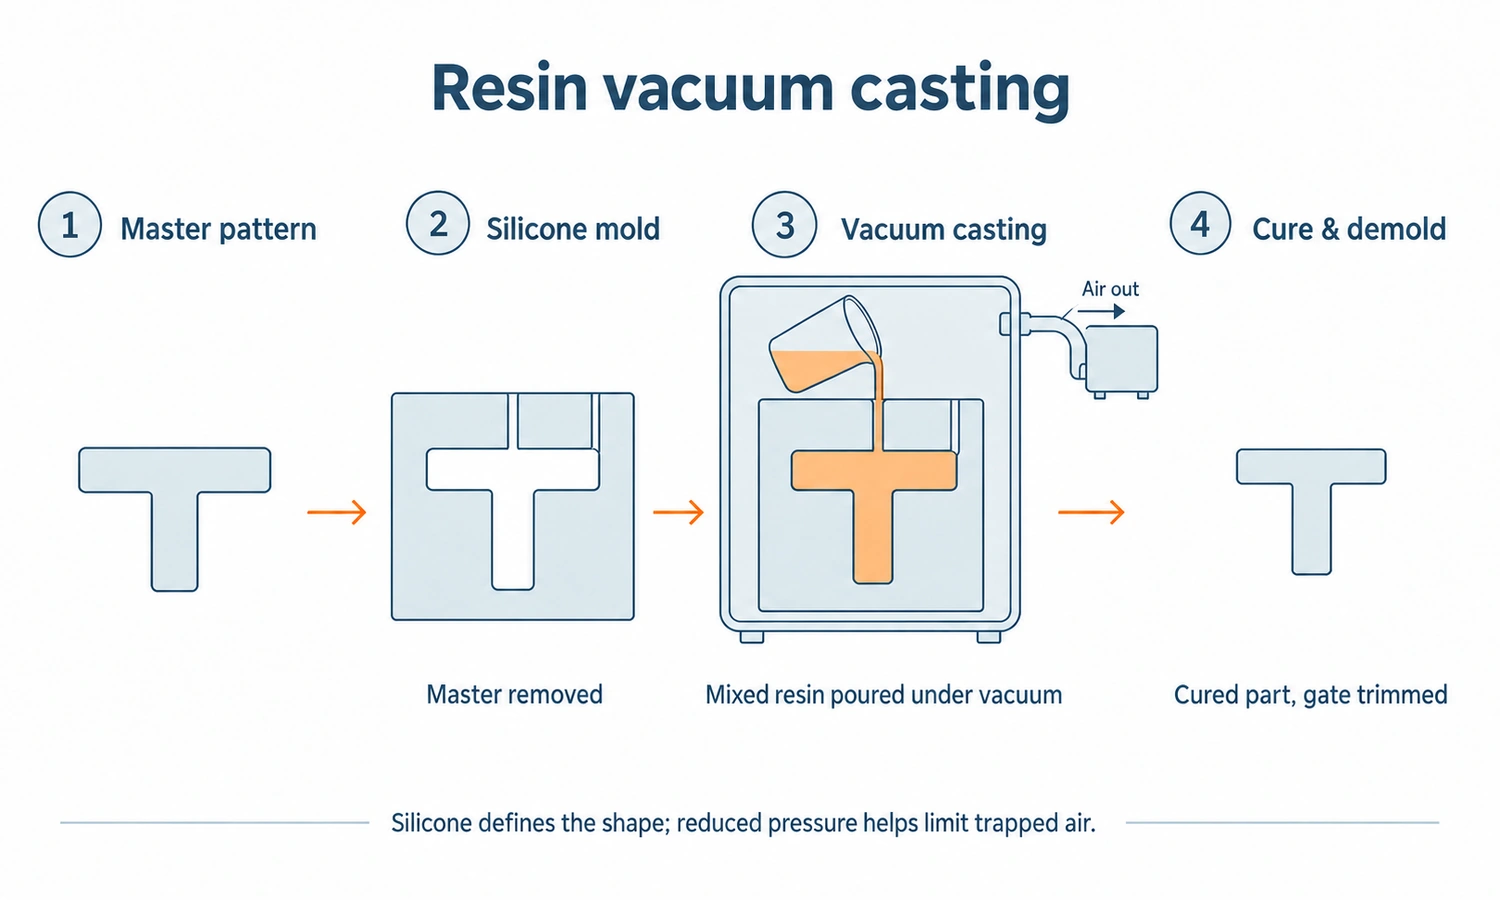
The conventional prototyping process begins with a finished master model.
1. Make the Master Pattern
The master determines the geometry and surface condition of every copy made from the silicone mold.
It is often produced through:
- SLA 3D printing
- CNC-Bearbeitung
- Another high-resolution prototyping method
The master may then be sanded, polished, painted, or otherwise finished.
This is important because the silicone mold reproduces very small surface details.
A rough master produces rough replicas.
2. Build a Silicone Mold
The master model is positioned inside a mold box.
Liquid silicone is poured around it, commonly under controlled vacuum conditions to reduce trapped bubbles.
After the silicone cures, the mold is carefully cut open and the master is removed.
What remains is a flexible negative cavity matching the original part.
Depending on geometry, the mold may contain:
- Two or more mold sections
- Gates
- Vents
- Inserts
Unlike an injection-molding tool, this mold is relatively quick and inexpensive to create.
It is also temporary.
3. Prepare the Casting Resin
The production material is normally a two-part polyurethane or similar resin system.
Manufacturers can choose formulations designed to imitate characteristics of production plastics such as:
- ABS-like rigidity
- Polypropylene-like flexibility
- Rubber-like elasticity
- Transparent plastics
- High-temperature plastics
These materials simulate many useful prototype properties, but they should not automatically be treated as chemically identical to the final injection-molding resin.
4. Cast Under Vacuum
The resin components are mixed and poured into the silicone mold.
Vacuum helps remove air that might otherwise remain in the liquid resin or become trapped around small features.
The objective is not to “suck the part into shape.”
The mold already defines the shape.
Vacuum mainly improves filling and reduces unwanted bubbles.
5. Cure and Remove the Part
The resin is allowed to cure, sometimes with controlled heating.
Because silicone is flexible, the mold can then be opened and the finished replica removed.
The same silicone tool can normally be reused for a limited number of components before wear, tearing, or dimensional deterioration makes replacement necessary.
How many parts one mold produces depends strongly on:
- Geometrie
- Undercuts
- Resin chemistry
- Surface texture
- Mold design
In practice, vacuum casting is therefore a short-run process rather than permanent production tooling.
What Materials Are Used in Vacuum Casting?
For conventional silicone-mold vacuum casting, the answer is usually casting resin rather than metal.
Polyurethane Resins
Polyurethane systems dominate the process because manufacturers can formulate them with very different mechanical and cosmetic characteristics.
Depending on the resin, parts may be:
- Rigid
- Semi-rigid
- Flexible
- Rubber-like
- Transparent
- Colored
- Flame-resistant
- Heat-resistant to varying degrees
This versatility is one of the main advantages of the process.
A design team can produce prototype parts that behave much more like molded products than a basic visual 3D print.
Silicone Parts
Silicone materials can also be used for certain soft components.
Applications may include:
- Seals
- Flexible covers
- Soft-touch parts
- Prototype elastomer components
Again, material capability should be checked against the actual application rather than assumed from appearance alone.
When Does Vacuum Casting Make Sense?
Resin vacuum casting works best in the gap between one-off prototyping Und production injection molding.
It is particularly useful when you need several realistic copies of the same design.
Typical situations include:
Functional Prototypes
A single 3D-printed part may be enough to inspect geometry.
But a development team may need several parts for:
- Assembly testing
- User testing
- Drop tests
- Customer demonstrations
- Internal validation
A reusable silicone mold can make that more practical.
Appearance Models
Because the silicone reproduces the master surface closely, the process works well for parts where appearance matters.
Textures, colors, clear sections, and soft-touch characteristics can often be simulated.
Bridge Production
Sometimes the product design is complete but the final production tooling is not ready.
A small vacuum-cast batch can provide temporary parts while production tooling is developed.
Low-Volume Products
If only a few dozen components are needed, permanent injection-molding tooling may never make economic sense.
Vacuum casting can serve as the production process itself.
Limitations of Resin Vacuum Casting
The flexibility of the process should not be confused with mass-production capability.
Silicone Molds Wear Out
The silicone mold is intentionally soft and flexible.
That makes complicated demolding possible, but it also limits mold life.
If production rises into hundreds or thousands of identical parts, repeatedly replacing silicone molds becomes inefficient.
Resin Is Not Always the Final Production Material
A polyurethane described as “ABS-like” is still not automatically the same material as injection-molded ABS.
This matters when the application depends on:
- Long-term outdoor exposure
- Exact chemical resistance
- Regulatory certification
- Long-term creep
- Production-specific flame ratings
Prototype performance should therefore be matched to what the test actually needs to prove.
Dimensional Consistency Is Lower Than Permanent Tooling
Silicone is flexible.
Its dimensional stability and tool life cannot match a rigid steel production mold over large production quantities.
Unit Cost Does Not Scale Like Injection Molding
Vacuum casting avoids expensive permanent tooling, but significant labor remains in:
- Mixing
- Pouring
- Curing
- Demolding
- Mold replacement
That cost remains with every batch.
Vacuum Casting vs. 3D Printing
These processes are often used at similar stages of product development, but they solve different problems.
| Faktor | Vacuum Casting | 3D Printing |
|---|---|---|
| Tooling | Silicone mold required | Usually none |
| Best Quantity | Small batches of repeated parts | One-offs and very small batches |
| Surface | Closely copies a finished master | Depends on printing process |
| Material Simulation | Wide range of plastic-like PU properties | Limited by printing material |
| Design Changes | New master/mold may be required | Digital file can be changed quickly |
| Repeat Copies | Efficient for multiple identical parts | Each part printed individually |
If you need one part tomorrow to check geometry, 3D printing is often the simpler solution.
If you need 20 visually and mechanically similar replicas, vacuum casting can become more useful.
Vacuum Casting vs. Injection Molding
The fundamental tradeoff is temporary tooling versus permanent tooling.
Injection molding requires a rigid production mold, usually aluminum or steel.
That involves a much larger upfront investment.
But once production begins, parts can be molded rapidly and consistently in true thermoplastics.
Vacuum casting uses a lower-cost silicone tool but produces parts much more slowly.
So the practical distinction is:
Vacuum casting minimizes the commitment to tooling.
Injection molding minimizes unit cost at scale.
The decision depends less on whether one process makes a “better” plastic part and more on whether the project has enough stable production volume to justify permanent tooling.
Can Vacuum Casting Be Used for Metal?
This is where the terminology becomes confusing.
The conventional silicone-mold process described above is not a metal casting process.
Molten steel, stainless steel, or nickel superalloy obviously cannot be poured into the same flexible silicone tooling used for polyurethane prototypes.
However, several real metal-manufacturing processes also use vacuum.
That is where terms such as:
- Vacuum investment casting
- Vacuum precision casting
- Vacuum induction melting
- Vacuum die casting
come from.
These terms should be understood separately.
What Is Vacuum Investment Casting?
Investment casting normally uses a disposable ceramic shell rather than a silicone mold.
In standard production, metal can be melted and poured under atmospheric conditions.
But some high-performance alloys need much tighter environmental control.
Why Melt Metal Under Vacuum?
Nickel- and cobalt-based superalloys may contain reactive alloying elements such as:
- Aluminium
- Titanium
At molten-metal temperatures, interaction with atmospheric gases can affect cleanliness and chemistry.
Vacuum induction melting provides a controlled environment for preparing these alloys before pouring.
The Investment Casting Institute publishes technical material specifically addressing Vacuum Precision Investment Casting, in which alloy is induction melted under vacuum before being poured into a preheated ceramic shell.
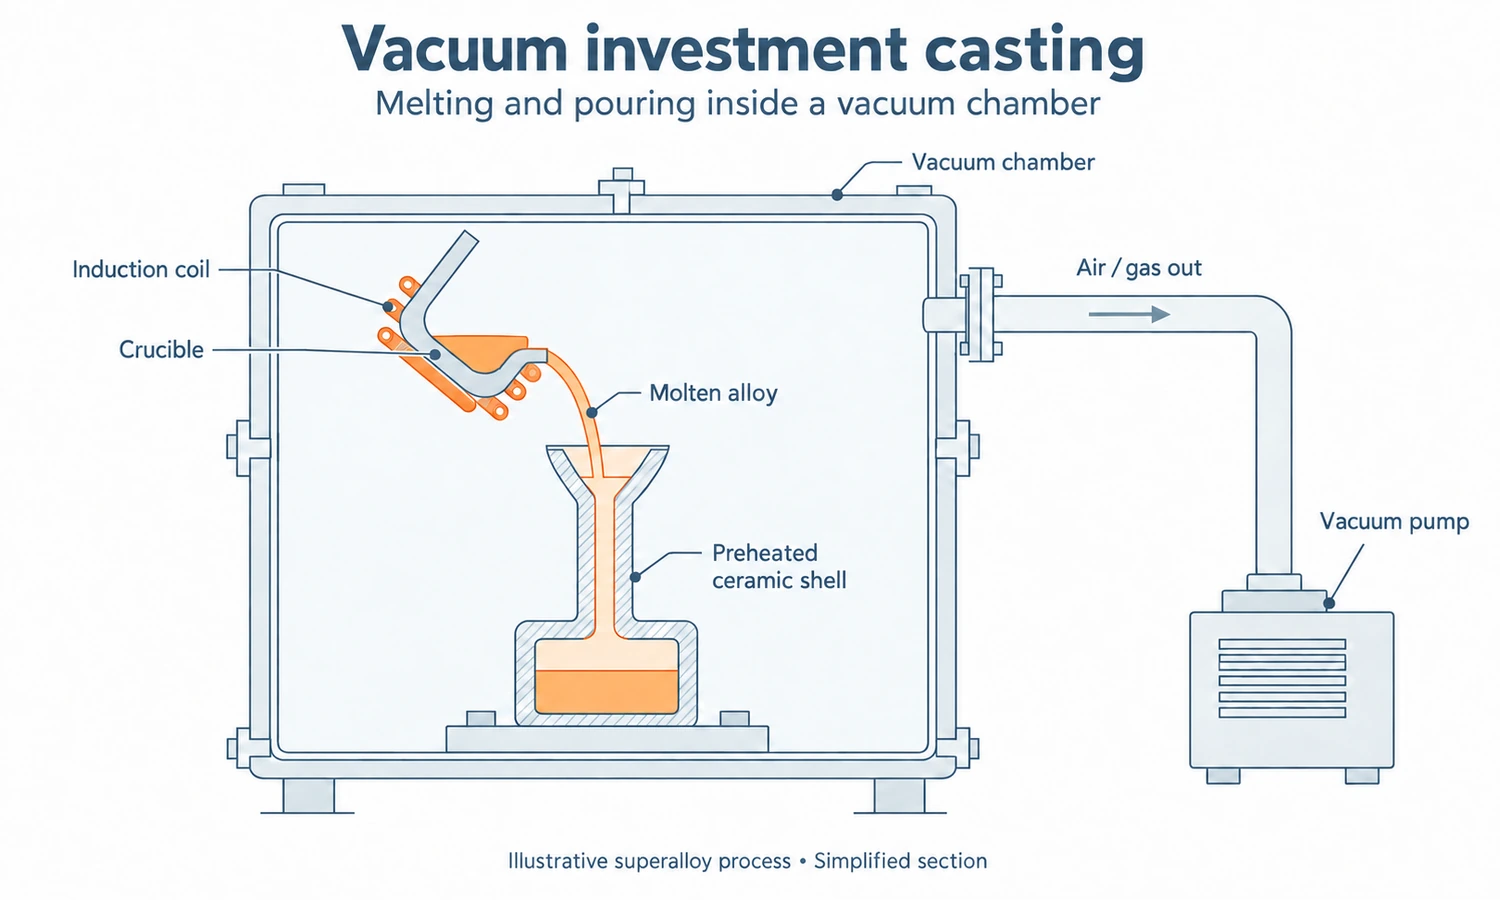
Commercial aerospace casting operations also use vacuum-melted nickel- and cobalt-based superalloys for high-performance precision components.
Vacuum Melting Is Not the Same as Resin Vacuum Casting
This distinction is important.
In resin vacuum casting:
vacuum primarily helps control air during resin molding.
In vacuum investment casting:
vacuum may control the environment around molten metal and the pouring operation.
The molds, temperatures, materials, equipment, and final products are completely different.
At YTD Foundry, our use of vacuum belongs to this metal investment-casting context, not polyurethane silicone-mold prototyping.
For suitable nickel-, cobalt-, and iron-based superalloys, vacuum melting can be integrated with our investment-casting process.
Investment Casting at YTD Foundry
What Is Vacuum Die Casting?
Vacuum die casting is another completely different metal process.
In conventional high-pressure die casting, molten metal enters a reusable steel die very quickly.
Air inside the cavity can become trapped during filling.
In high-vacuum die casting, the die is sealed and air is evacuated before and during injection.
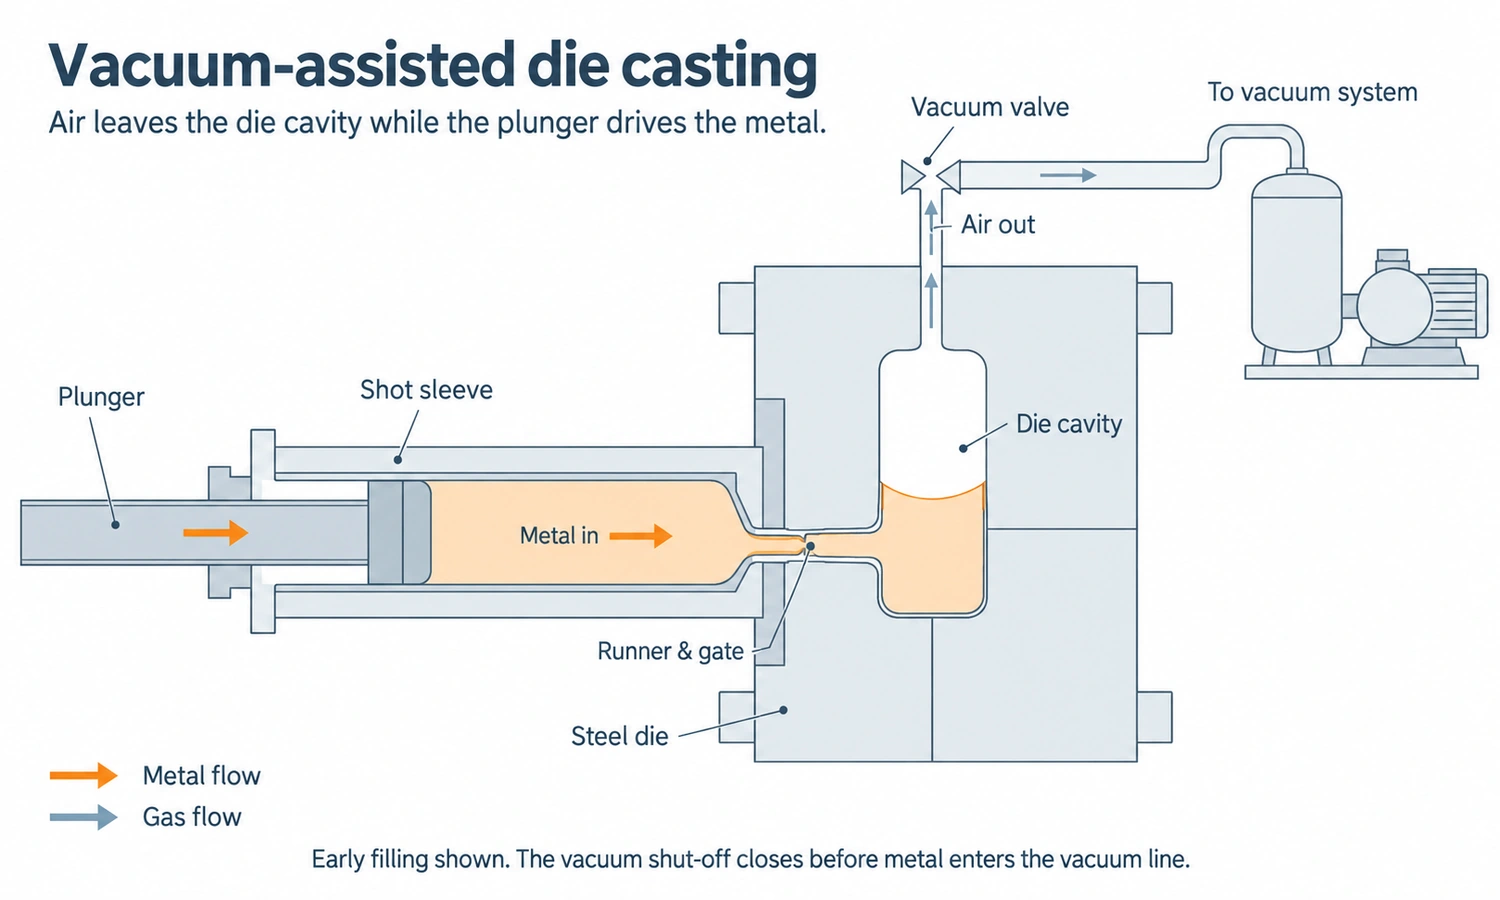
NADCA explains that this reduces the amount of gas trapped in the casting and allows high-vacuum components to achieve higher mechanical integrity and, when properly designed, support heat treatment.
This process is particularly relevant to structural aluminum die castings.
The logic is:
Vacuum investment casting → control around high-performance molten alloys and ceramic-shell casting.
Vacuum die casting → remove gas from a reusable metal die during high-pressure filling.
Again, sharing the word “vacuum” does not make them the same process.
Vacuum Resin Casting vs. Vacuum Investment Casting vs. Vacuum Die Casting
The following comparison usually resolves the terminology quickly.
| Faktor | Resin Vacuum Casting | Vacuum Investment Casting | Vacuum Die Casting |
|---|---|---|---|
| Material | Polyurethane / resin | High-performance metal alloys | Mainly aluminum and other die-cast alloys |
| Mold | Silicone | Einweg-Keramikhülle | Wiederverwendbare Stahlmatrize |
| Vacuum Purpose | Reduce air during resin molding | Control melting/pouring environment | Evacuate gas from die cavity |
| Werkzeugkosten | Niedrig | Mäßig | Hoch |
| Typisches Volumen | Prototype / short run | Low-medium specialized production | High production |
| Typical Product | Plastic-like prototype | Turbine / industrial precision metal part | Structural aluminum production part |
| Main Advantage | Fast low-volume replication | High-performance alloy processing | Dense high-volume metal production |
This is why asking:
“What are the advantages of vacuum casting?”
without identifying the process can produce contradictory answers.
One source may be discussing polyurethane prototypes.
Another may be discussing turbine blades.
Another may be describing structural automotive aluminum.
All can legitimately use the term “vacuum casting.”
Which Vacuum Casting Process Do You Need?
A simple material-first decision usually solves the problem.
You Need Plastic-Like Prototype Parts
If you need:
- 5–50 prototype housings
- Cosmetic samples
- Soft-touch prototypes
- Transparent prototypes
- Pre-production resin parts
then silicone-mold resin vacuum casting is probably the process you are looking for.
You Need a High-Performance Cast Metal Component
If the component requires:
- Nickel-based superalloy
- Cobalt-based alloy
- High-temperature service
- Complex precision metal geometry
then vacuum investment casting may be relevant.
You Need High-Volume Structural Aluminum Components
If the project requires:
- High-volume production
- Thin aluminum walls
- Hochdruck-Druckguss
- Reduced gas porosity
- Structural heat-treated components
then high-vacuum die casting deserves consideration.
The word “vacuum” should come after identifying the material and manufacturing objective, not before.
Where YTD Foundry Fits
YTD Foundry specializes in custom metal castings rather than silicone-mold polyurethane prototypes.
Our core in-house process is investment casting.
For suitable superalloy projects, this can include:
- Tooling
- Wax pattern production
- Ceramic shell building
- Vacuum melting
- Feinguss
- Wärmebehandlung
- CNC-Bearbeitung
- Inspection
Superalloy Casting at YTD Foundry
For components better suited to vacuum die casting, production can be coordinated through our specialized die-casting partners.
This distinction matters when requesting a quote.
If you send a drawing for a “vacuum casting” project, the first thing we need to know is not the required vacuum level.
Es ist:
What material is the part, what does it need to do, and how many do you need?
Those answers determine which meaning of vacuum casting is actually relevant.
Schlussbetrachtung
“Vacuum casting” does not identify one manufacturing process.
For most prototyping searches, it means resin poured into a silicone mold under vacuum. In metal manufacturing, vacuum may instead be used during investment casting or high-pressure die casting for completely different reasons.
Start with the material, required quantity, and function of the part. Once those are clear, the correct vacuum-based process becomes much easier to identify.
Häufig gestellte Fragen
Is Vacuum Casting a Plastic or Metal Process?
It can refer to both, which is why the term is confusing. In general manufacturing searches, vacuum casting usually means polyurethane resin cast into silicone molds for prototypes and short production runs. In metal manufacturing, vacuum can also be used in investment casting or die casting.
What Material Is Used for Vacuum Casting?
Conventional prototype vacuum casting mainly uses polyurethane and similar resin systems. Metal vacuum processes can use completely different alloys, including aluminum in vacuum die casting and selected nickel- or cobalt-based superalloys in vacuum investment casting.
How Many Parts Can a Vacuum Casting Mold Make?
A silicone mold normally produces only a limited number of parts before wear affects quality. The actual number depends on component geometry, resin, surface details, undercuts, and mold design. It should be considered temporary tooling rather than a production mold with a fixed long life.
Is Vacuum Casting Cheaper Than Injection Molding?
For small quantities, it often requires far less tooling investment. At high production volumes, injection molding normally becomes more economical because its permanent tooling supports very fast repeat production.
Is Vacuum Casting the Same as Vacuum Investment Casting?
No. Conventional vacuum casting uses silicone molds and resin to produce prototype or low-volume plastic-like parts. Vacuum investment casting uses refractory ceramic molds and molten metal, with vacuum used to control suitable high-performance metal processing.
Why Is Vacuum Used for Superalloy Casting?
Vacuum provides greater control over the atmosphere surrounding molten reactive alloys. This is particularly valuable for selected nickel- and cobalt-based superalloys containing elements that can interact with atmospheric gases during melting.